

Working Principle and Features of Pharmaceutical Pneumatic Conveying Systems
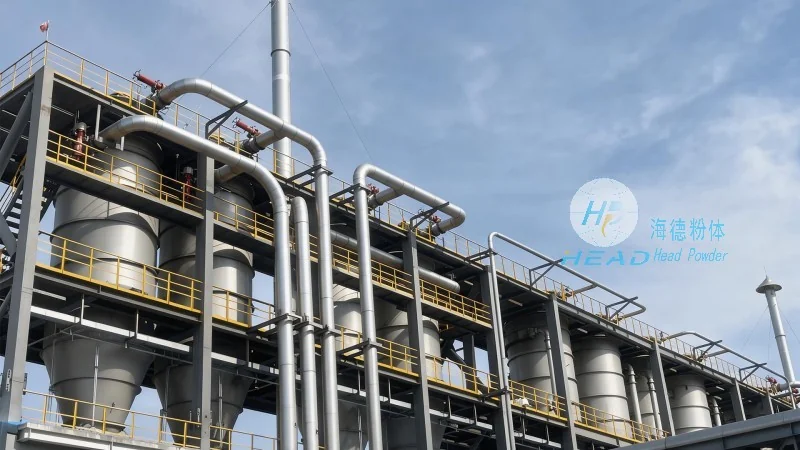
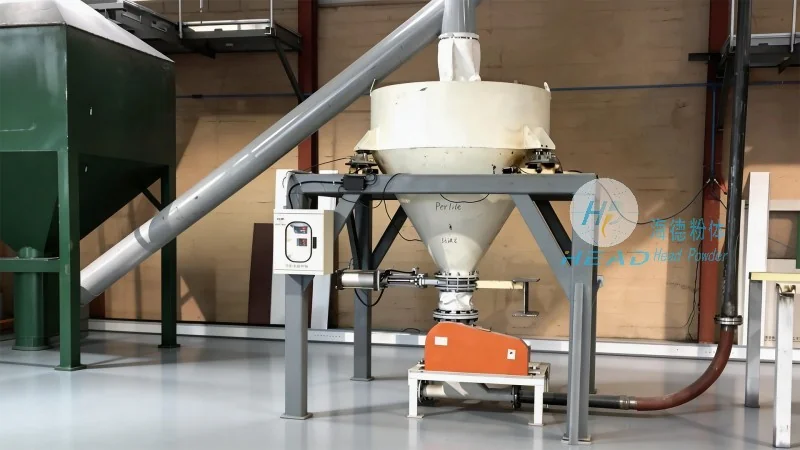
Pharmaceutical pneumatic conveying systems operate by utilizing compressed air or other gases to transport bulk materials, such as powders and granules, through a network of pipes. The process typically involves a feeding mechanism that introduces the material into the system, where it is then carried by the air flow. The system may employ different conveying methods, including dilute-phase and dense-phase transport, each tailored to specific material properties and application requirements. The compressed air creates a flow that moves the material from the source to the destination, ensuring efficient and controlled transfer. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and enhancing hygiene, which is critical in pharmaceutical environments where contamination control is paramount.
Key Features of Pharmaceutical Pneumatic Conveying Systems
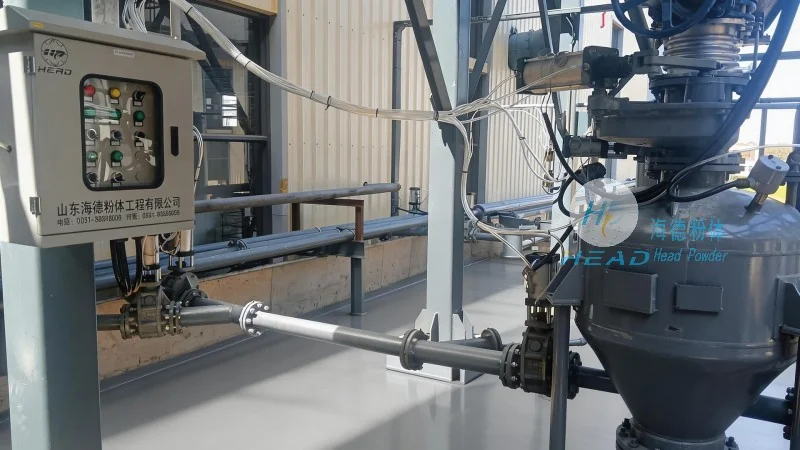
Pharmaceutical pneumatic conveying systems are designed with several distinct features that make them suitable for the pharmaceutical industry. Firstly, they offer high levels of containment and dust control, minimizing the risk of product contamination and cross-contamination. The enclosed piping system prevents airborne particles from escaping, ensuring compliance with regulatory standards like GMP (Good Manufacturing Practice). Secondly, these systems provide flexibility in material handling, allowing for the transport of various powders and granules with different flow characteristics. The ability to adjust air pressure and flow rates enables precise control over the conveying process, ensuring consistent material delivery. Additionally, pneumatic conveying systems are easy to clean and maintain, with features like CIP (Clean-In-Place) and SIP (Steam-In-Place) compatibility, which are essential for maintaining sterile conditions in pharmaceutical manufacturing. Another key feature is their space efficiency, as the system can be installed in compact areas, making it ideal for facilities with limited floor space. Finally, the systems are designed for durability and reliability, with components made from materials that resist corrosion and wear, ensuring long-term operation with minimal downtime.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for the pharmaceutical industry. With a focus on precision engineering and adherence to industry standards, the company provides customized solutions tailored to the unique needs of pharmaceutical manufacturers. HeadPowder's systems are engineered to meet stringent regulatory requirements, ensuring compliance with GMP and other quality control measures. The company's expertise lies in developing efficient and reliable conveying solutions that enhance production efficiency while maintaining the highest standards of product purity and safety. HeadPowder's commitment to innovation and customer satisfaction has established it as a trusted partner in the pharmaceutical equipment sector, delivering solutions that meet the evolving demands of modern pharmaceutical production.