

Working Principle and Features of a Glucose Powder Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of bulk material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. HeadPowder, as the company is commonly known, has established itself as a trusted partner for industries requiring efficient and reliable transport of fine powders, such as glucose powder. This article explores the working principle and key features of a glucose powder pneumatic conveying system, highlighting how these systems enhance operational efficiency and product integrity in industrial applications.
Introduction to Glucose Powder Pneumatic Conveying Systems
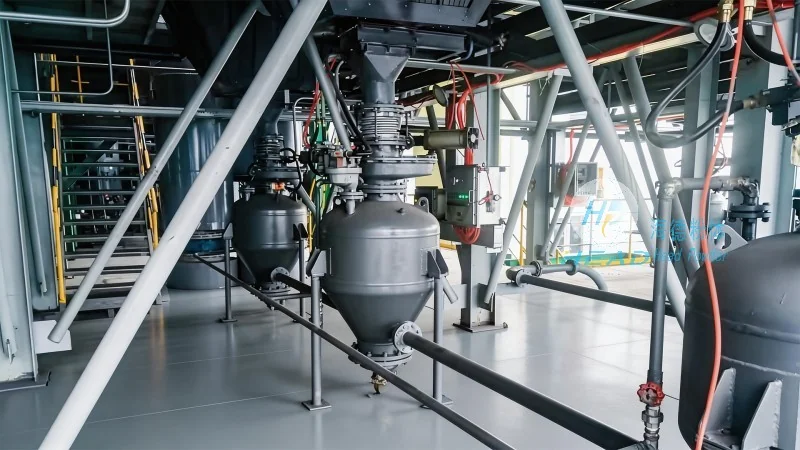
A pneumatic conveying system is a technology used to transport bulk materials, including powders, granules, and small particles, through a pipeline using air or other gases as the conveying medium. In the context of glucose powder, which is a fine, hygroscopic material commonly used in food, pharmaceutical, and chemical industries, pneumatic conveying offers a superior alternative to traditional methods like bucket elevators or belt conveyors. The system ensures that the powder is moved with minimal contact, reducing the risk of contamination and degradation, while maintaining a high level of hygiene and safety. HeadPowder's expertise lies in customizing these systems to meet the specific requirements of glucose powder handling, ensuring optimal performance and compliance with industry standards.
Working Principle of the Pneumatic Conveying System
The core working principle of a glucose powder pneumatic conveying system involves the use of compressed air to create a flow of material through a pipeline. The process typically begins with the material being fed into a hopper or silo, where it is then drawn into the conveying line by the pressure differential created by the air flow. The compressed air, often supplied by a blower or compressor, is introduced at the inlet of the pipeline, generating a high-velocity stream that entrains the glucose powder particles. As the mixture travels through the pipeline, the air and powder are separated at the discharge point, typically using a cyclone separator or a filter. The separated air is then recirculated back into the system, while the glucose powder is collected in a receiving hopper or storage tank. This continuous cycle ensures a seamless and efficient transport of the powder from the source to the destination. HeadPowder's systems are engineered with precision, ensuring that the air-to-powder ratio is optimized to maintain a stable and consistent flow, minimizing pressure drops and preventing material blockages.
Key Features of the System
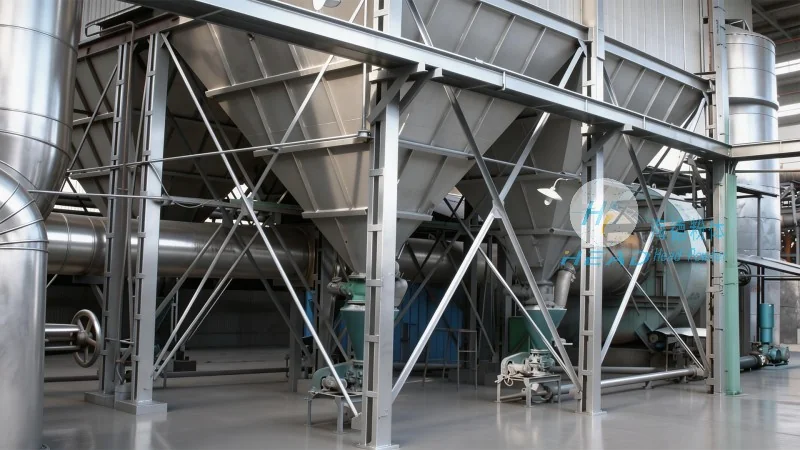
HeadPowder's glucose powder pneumatic conveying systems are characterized by several key features that set them apart in the industry. Firstly, the system offers high efficiency in material transport, with the ability to move large quantities of glucose powder over long distances with minimal energy consumption. The use of compressed air as the conveying medium eliminates the need for mechanical components like belts or chains, reducing maintenance costs and downtime. Secondly, the system is designed for cleanliness and hygiene, which is crucial in the food and pharmaceutical sectors where contamination control is paramount. The enclosed pipeline system prevents dust and powder from escaping into the environment, while the materials used in construction, such as stainless steel, are easy to clean and sanitize. Thirdly, the system provides flexibility in operation, allowing for easy integration with existing production lines and the ability to adjust the conveying rate based on production demands. HeadPowder's engineers also incorporate advanced control systems that monitor pressure, flow, and temperature in real-time, ensuring optimal performance and early detection of any issues. Additionally, the system is designed for low maintenance, with components like the blower and cyclone separator being easily accessible for routine checks and repairs. These features collectively contribute to a reliable and cost-effective solution for glucose powder handling, enhancing overall operational productivity and product quality.
Applications and Benefits in Industrial Settings
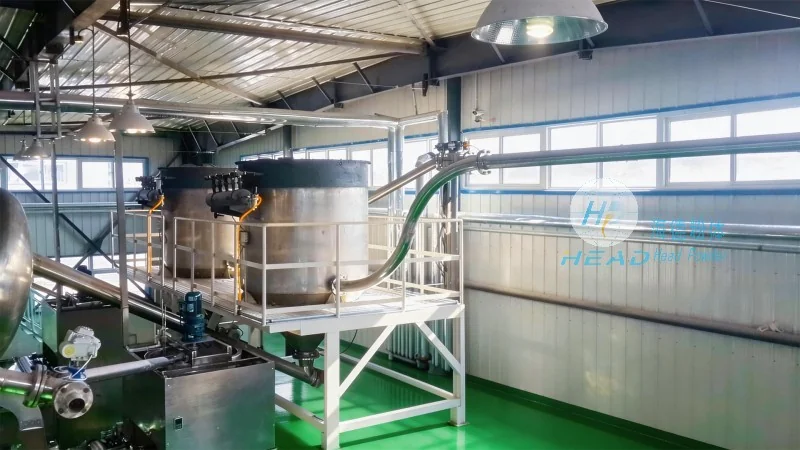
The application of glucose powder pneumatic conveying systems in industrial settings, particularly in the food and pharmaceutical industries, brings numerous benefits. In food processing, the system ensures that glucose powder is transported without any loss of flavor or quality, as the enclosed system prevents exposure to external contaminants. This is critical for maintaining the safety and regulatory compliance of food products. In pharmaceutical manufacturing, the system's hygienic design and ability to handle fine powders with precision are essential for producing high-quality medications. The benefits extend to cost savings, as the system reduces labor costs associated with manual handling and minimizes material waste due to reduced spillage and breakage. Furthermore, the system's ability to handle large volumes efficiently reduces the need for multiple handling steps, streamlining the production process and increasing overall throughput. HeadPowder's commitment to quality and customization ensures that their systems are tailored to meet the specific needs of each client, providing a solution that is both effective and sustainable.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd. stands as a leading manufacturer of glucose powder pneumatic conveying systems, leveraging advanced technology and engineering expertise to deliver reliable and efficient solutions for bulk material handling. The company's systems are designed to meet the stringent requirements of various industries, ensuring that glucose powder is transported with the highest level of quality and safety. By understanding the working principles and key features of these systems, industries can enhance their operational efficiency, reduce costs, and improve product integrity. HeadPowder's dedication to innovation and customer satisfaction positions them as a trusted partner in the development of advanced material handling solutions, contributing to the growth and success of their clients in the competitive market.