

Working Principle and Features of High-Temperature Ash Powder Pneumatic Conveying Systems
High-temperature ash powder pneumatic conveying systems are advanced industrial equipment designed to transport high-temperature, fine particulate materials efficiently and safely. These systems are widely used in power plants, cement factories, and other industrial facilities where the handling of hot ash and powders is essential. The technology behind these systems combines pneumatic transport principles with specialized components to ensure reliable operation under challenging conditions.
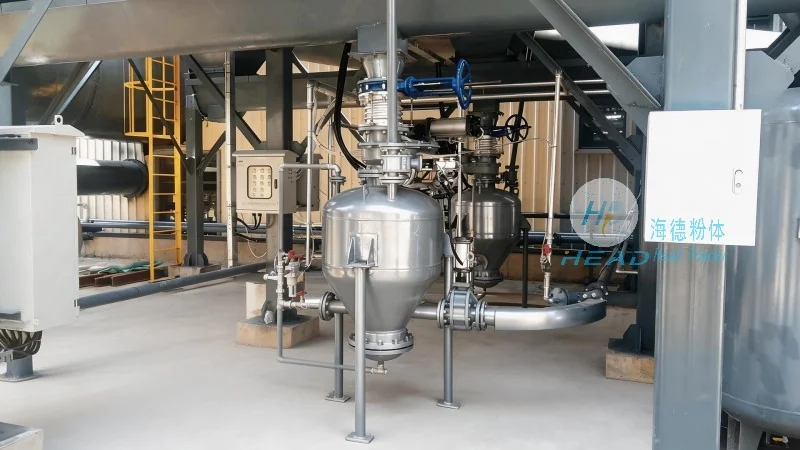
Working Principle of High-Temperature Ash Powder Pneumatic Conveying Systems
The core working principle of a high-temperature ash powder pneumatic conveying system involves the use of compressed air or gas to create a flow that transports the ash particles through a pipeline. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line (often with heating elements to maintain temperature), and a receiver for the discharged material. The process begins when the ash is fed into the system, and the feeder introduces the material into the conveying line. Compressed air is then introduced at the inlet, creating a high-velocity flow that lifts and transports the ash particles. The air and ash mixture travels through the pipeline, and the ash is separated from the air at the receiver, where the air is often filtered and recycled. The system is designed to handle temperatures up to several hundred degrees Celsius, ensuring that the material remains in a dry, powdery state throughout the transport process. This method eliminates the need for mechanical components like belts or buckets, reducing wear and maintenance while improving overall efficiency.
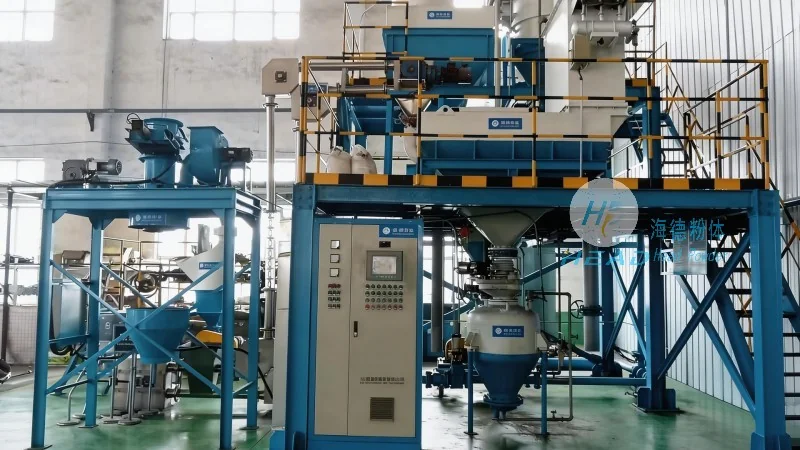
Key Features and Advantages of High-Temperature Ash Powder Pneumatic Conveying Systems
High-temperature ash powder pneumatic conveying systems offer several key features that make them ideal for industrial applications. One of the primary advantages is their ability to handle materials with high temperatures, which is critical for ash from power plant boilers. The systems are equipped with temperature-resistant components, such as heated pipelines and insulated hoppers, to prevent material degradation or caking. Another significant feature is the system's flexibility in conveying distances and heights, allowing for horizontal, vertical, or inclined transport. This adaptability makes it suitable for various plant layouts and operational requirements. The systems also provide high transport efficiency, with minimal material loss and low pressure drop across the pipeline. This results in lower energy consumption and reduced operational costs. Additionally, the pneumatic design offers better safety compared to mechanical systems, as there are no moving parts that could cause sparks or mechanical failures. The enclosed pipeline system also helps in controlling dust emissions, contributing to a cleaner and safer working environment. The systems are designed for easy maintenance, with accessible components and automated controls that monitor pressure, temperature, and flow rates. This ensures consistent performance and reduces downtime, making them a reliable choice for continuous industrial operations.
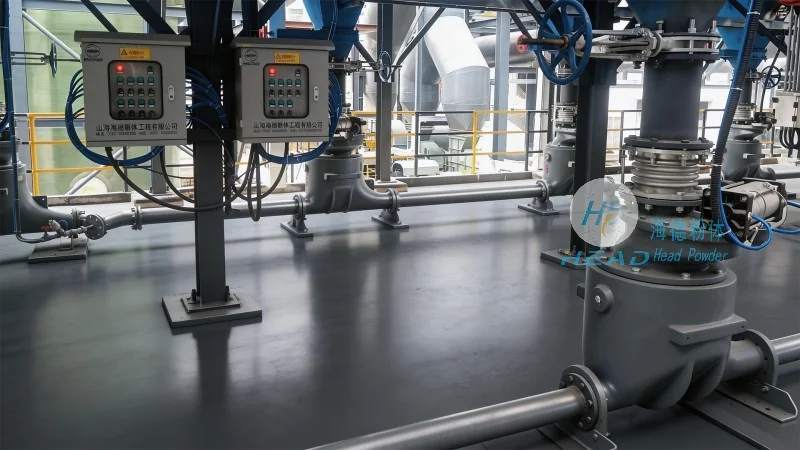
Technical Specifications and Application Scenarios
Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing high-temperature ash powder pneumatic conveying systems tailored to meet the specific needs of industrial clients. The company's systems are engineered with robust materials, such as stainless steel and heat-resistant alloys, to withstand the harsh conditions of high-temperature ash transport. Typical technical specifications include conveying capacities ranging from 1 to 50 tons per hour, depending on the system size and application. The systems can handle ash temperatures up to 600°C, with some models capable of higher temperatures. The conveying line diameter varies from 50 to 200 mm, and the system can cover distances of up to several hundred meters, including vertical lifts of up to 50 meters. The company's systems are designed for integration into existing industrial facilities, with options for both new installations and retrofits. They are commonly used in power plants for transporting fly ash from boilers to storage silos or for use in cement production. In cement factories, the systems help in conveying raw materials and finished products, improving production efficiency. The systems are also applicable in other industries, such as chemical and metallurgical plants, where high-temperature powders need to be transported safely and efficiently. The company's commitment to quality and innovation ensures that their systems meet international standards and provide long-term reliability for industrial operations.