

Principles and Working Scene Characteristics of Sugar Powder Conveying Systems
The sugar powder conveying system is a specialized solution designed to handle the unique properties of sugar as a bulk powder material. In industrial settings, particularly within the food processing and sugar manufacturing sectors, efficient and reliable transport of sugar from storage to processing or packaging stages is critical. This system leverages advanced engineering principles to address the challenges posed by sugar's characteristics, such as its fine particle size, hygroscopic nature, and the need for sanitary, low-dust operation. The following content explores the fundamental principles behind these systems and highlights the key working scene characteristics that define their effectiveness in real-world applications.
Core Principles of the Conveying System
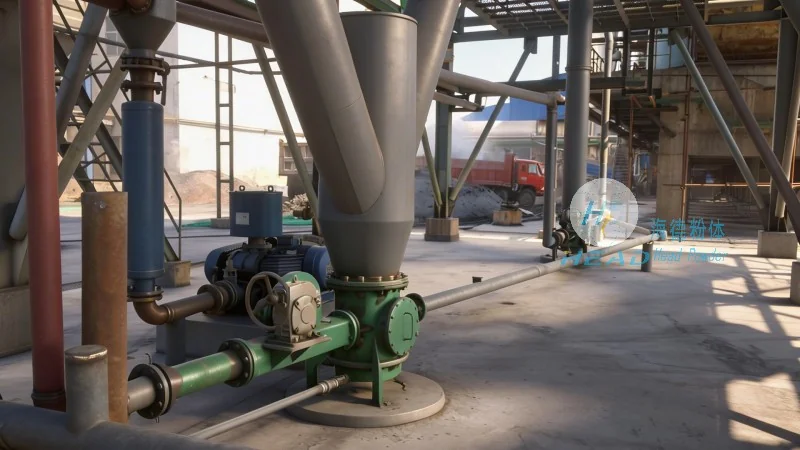
At the heart of the sugar powder conveying system are several core principles that ensure optimal performance. First, the system is engineered to maintain the integrity of the sugar powder, preventing agglomeration or caking during transport. This is achieved through controlled air flow and appropriate material handling mechanisms, such as rotary valves or pneumatic conveyors. Second, the design prioritizes hygiene and cleanliness, which is essential in food processing environments. Stainless steel components, sealed systems, and easy-to-clean designs are standard features to meet regulatory standards and maintain product quality. Third, the system is scalable and adaptable, allowing customization for different production capacities and operational requirements. Whether handling small batches for laboratory testing or large volumes for industrial production, the system can be configured to meet specific needs.
Key Working Scene Characteristics
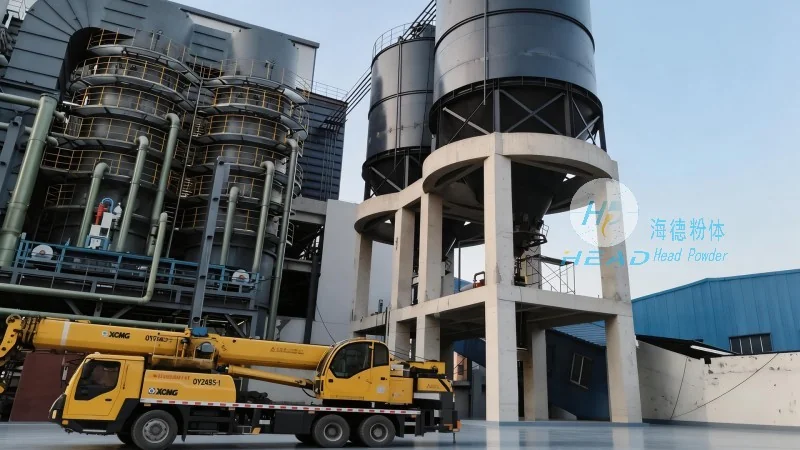
The effectiveness of a sugar powder conveying system is often determined by its performance in various working scenes. These scenes can range from initial raw material storage and handling to intermediate processing stages and final packaging. In warehouse environments, the system may be used to transfer bulk sugar from storage silos to production lines, ensuring a continuous supply without manual intervention. During production, the system can transport sugar between different processing units, such as from a grinding station to a refining unit, maintaining a consistent flow rate and preventing bottlenecks. In packaging areas, the system may deliver sugar to filling machines, where precise metering and controlled discharge are crucial for product consistency. The working scene characteristics also include the need for flexibility, as production schedules may change, requiring the system to adjust its speed or direction quickly. Additionally, the system must be robust enough to handle the abrasive nature of sugar particles, which can wear down components over time, necessitating durable materials and regular maintenance.
Application Examples in Real-World Operations
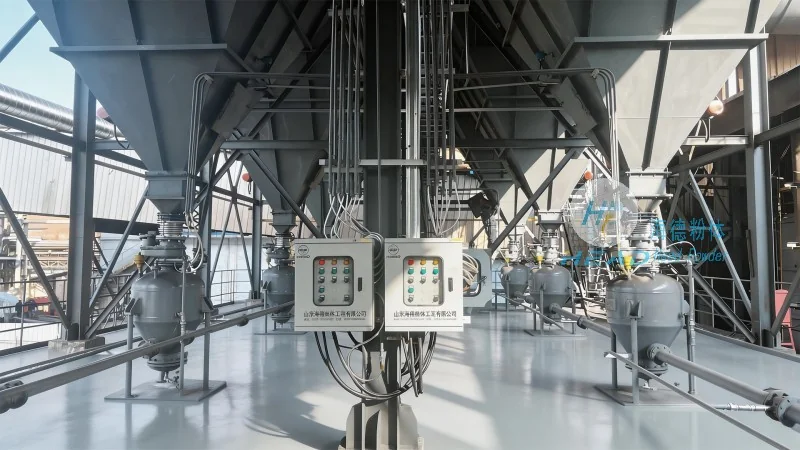
Real-world applications of sugar powder conveying systems are widespread across the sugar industry. For instance, in a large-scale sugar factory, the system might be used to transport raw sugar from a storage silo to a grinding mill, where it is converted into a fine powder. The pneumatic conveying system, with its high efficiency and minimal dust generation, is ideal for this process. Another example is in a confectionery plant, where the system delivers sugar to a mixing line, ensuring a consistent sugar-to-flavor ratio in the final product. The system's ability to handle different sugar grades, such as white sugar or brown sugar, without cross-contamination is a key advantage. Furthermore, in a packaging facility, the system may be integrated with automated filling machines, allowing for high-speed, accurate delivery of sugar into bags or containers. These applications demonstrate how the conveying system enhances operational efficiency, reduces labor costs, and improves product quality by maintaining the purity and consistency of the sugar powder throughout the process.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
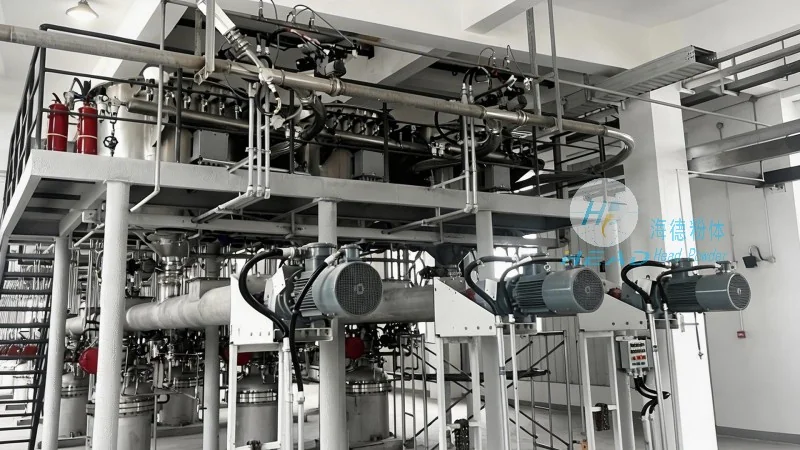
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of specialized powder handling solutions, including sugar powder conveying systems. With headquarters located in Shandong, China, the company has established itself as a trusted partner in the food processing and bulk material handling industries. HeadPowder's expertise lies in designing and manufacturing customized conveying systems that meet the unique requirements of each client. The company's team of engineers and technicians work closely with customers to understand their operational challenges and develop tailored solutions. By leveraging advanced technology and adhering to strict quality standards, HeadPowder ensures that its systems are reliable, efficient, and compliant with industry regulations. The company's commitment to innovation and customer satisfaction has made it a preferred choice for businesses seeking to optimize their sugar powder handling processes.