

Principle and Application Features of Dust-Free Automatic Powder Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced dust-free automatic powder pneumatic conveying systems. These systems are engineered to efficiently transport dry powders and bulk materials in industrial settings while maintaining a clean, contamination-free environment. The core principle of pneumatic conveying involves using compressed air or gas to move material through a pipeline, eliminating the need for mechanical components like belts or buckets that can introduce dust and contamination.
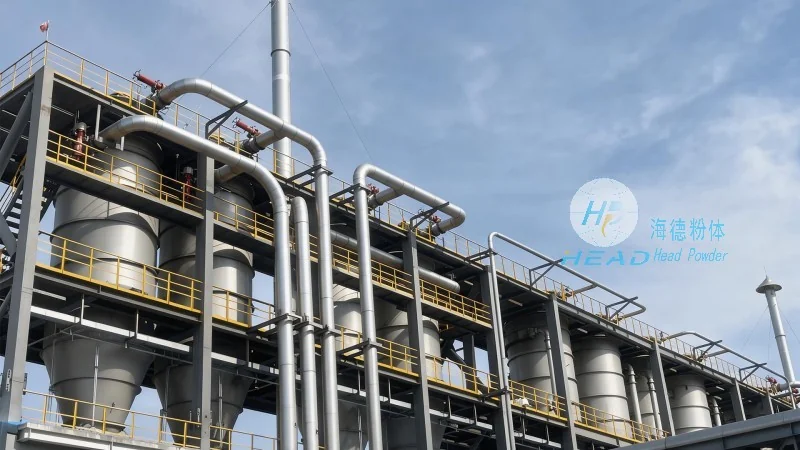
Key Working Principles of the Dust-Free Automatic Powder Pneumatic Conveying System
The dust-free automatic powder pneumatic conveying system operates on the principle of air-based material transport. It utilizes a closed-loop system with a positive or negative pressure differential to move powders from a source to a destination. The system typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the material. The compressed air is introduced at a controlled pressure, creating a flow that propels the powder particles through the pipeline. This method ensures that the material remains enclosed within the system, preventing dust emissions and maintaining a clean working environment. The system is designed with high-efficiency filters and seals to minimize air leakage and ensure that all material is conveyed without loss or contamination.
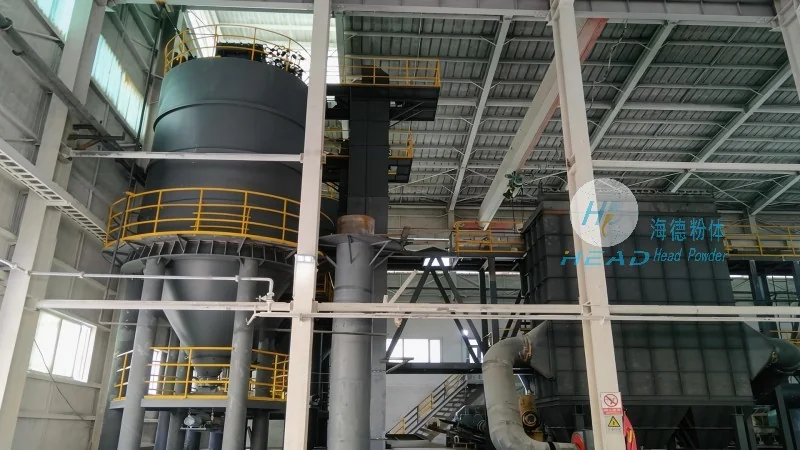
Application Scenarios and Industry Advantages
The dust-free automatic powder pneumatic conveying equipment is widely used in various industries where maintaining a dust-free environment is critical. In pharmaceutical manufacturing, these systems are essential for transporting active pharmaceutical ingredients (APIs) and excipients without cross-contamination. The food and beverage industry also relies on them to handle powders like flour, sugar, and spices, ensuring product purity and compliance with food safety regulations. In chemical processing, the systems are used to transport raw materials and finished products, reducing the risk of dust explosions and ensuring workplace safety. The automotive and electronics industries benefit from the precision and cleanliness of these systems when handling sensitive components and powders. The key advantages include improved product quality, reduced downtime due to maintenance, and enhanced workplace safety by eliminating dust-related hazards. Additionally, the automated nature of the system minimizes human error and labor costs, making it a cost-effective solution for high-volume material handling.
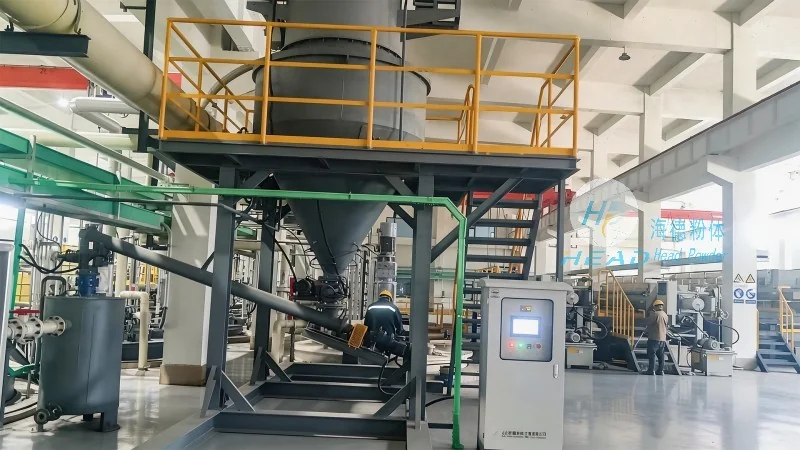
Technical Features and Customization Options
HeadPowder's dust-free automatic powder pneumatic conveying systems are equipped with advanced features to meet diverse industrial needs. The systems can be configured for both positive and negative pressure operations, allowing flexibility in different application scenarios. The material feeders are designed with adjustable flow control to maintain consistent material delivery, which is crucial for processes requiring precise dosing. The conveying lines are made from high-quality materials such as stainless steel or food-grade plastics, ensuring durability and resistance to corrosion and chemical exposure. The system includes integrated filtration and cleaning mechanisms to maintain air quality and prevent clogging. For large-scale operations, the systems can be scaled up with multiple conveying lines and receivers to handle high material throughput. Customization options are available to accommodate specific material properties, such as particle size, density, and moisture content. The systems can also be integrated with automation controls, enabling remote monitoring and operation, which enhances operational efficiency and reduces human intervention.
Company Background and Commitment to Quality
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer specializing in industrial conveying solutions. The company has a strong commitment to research and development, continuously improving its products to meet evolving industry standards. HeadPowder's dust-free automatic powder pneumatic conveying systems are designed and manufactured with a focus on durability, efficiency, and environmental compliance. The company adheres to international quality standards and undergoes rigorous testing to ensure that each system meets the highest performance criteria. With a team of experienced engineers and technicians, HeadPowder provides comprehensive support, including installation, maintenance, and technical assistance, to ensure that clients achieve optimal performance from their conveying systems. The company's dedication to quality and customer satisfaction has earned it a reputation as a trusted partner in the industrial equipment sector.