

Operation Process and Working Principle of Copper Sulfate Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in providing efficient and reliable equipment for the transportation of various powders, including copper sulfate. This article delves into the operation process and working principle of our copper sulfate pneumatic conveying equipment, highlighting its design, functionality, and the key steps involved in its operation.
Introduction to Copper Sulfate Pneumatic Conveying Equipment
Copper sulfate, also known as cupric sulfate or bluestone, is a common inorganic compound widely used in agriculture, water treatment, and industrial applications. The efficient and safe transportation of copper sulfate is crucial for maintaining product quality and ensuring smooth production processes. Pneumatic conveying systems offer a cost-effective and flexible solution for handling this material, especially in applications where dust control and minimal product degradation are essential.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating from Shandong, China, is dedicated to innovation and excellence in engineering. Our company, Shandong HeadPowder Engineering Co., Ltd., has established itself as a trusted provider of high-quality material handling equipment. With a focus on customer satisfaction and technical advancement, we design and manufacture equipment tailored to meet the specific needs of our clients, ensuring optimal performance and durability in demanding industrial environments.
Overview of the Pneumatic Conveying System
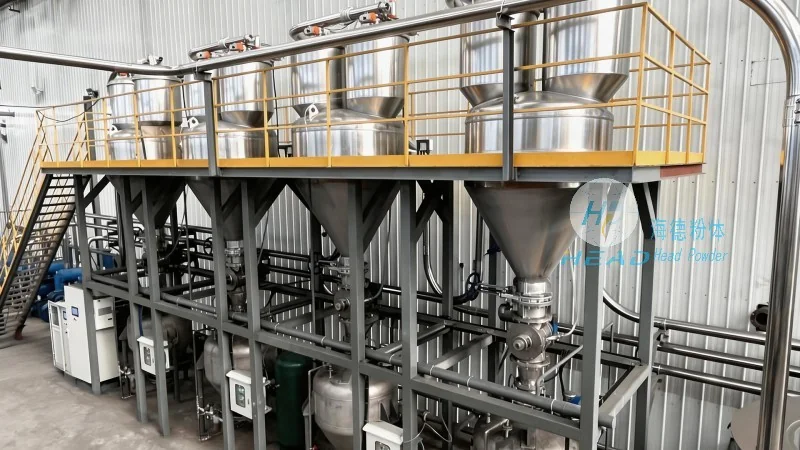
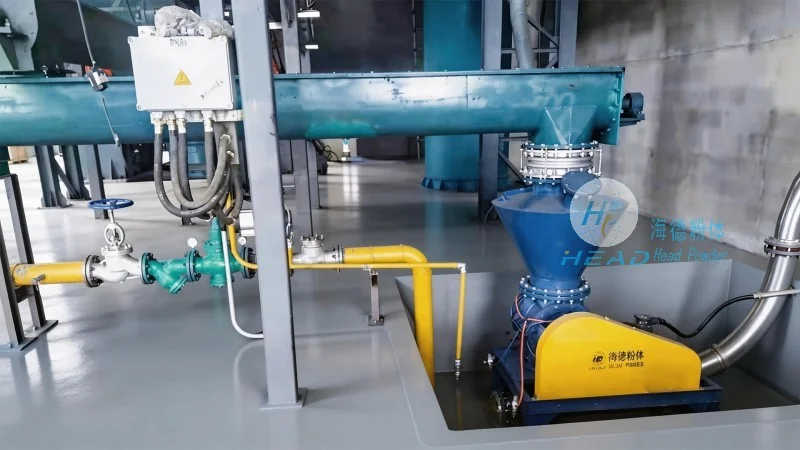
The copper sulfate pneumatic conveying equipment typically consists of several key components, including a hopper for material storage, a feeder to control the flow of copper sulfate, a conveying line (often equipped with filters and cyclones for dust separation), and a receiver for the discharged material. The system operates by using compressed air to create a flow that transports the copper sulfate particles through the pipeline, ensuring a continuous and controlled movement of the material from the source to the destination.
Step-by-Step Operation Process
The operation of the copper sulfate pneumatic conveying equipment involves a series of coordinated steps to ensure efficient material transport. First, the copper sulfate is fed into the hopper from the storage container. The feeder then regulates the flow rate, preventing overloading and ensuring a consistent supply of material to the conveying line. Compressed air is introduced into the system, creating a pressure differential that propels the copper sulfate particles through the pipeline. As the material travels, it passes through filters and cyclones that separate any entrained dust or moisture, maintaining the purity of the copper sulfate. The material is then collected in the receiver at the end of the conveying line, ready for further processing or storage.
Working Principle of the Equipment
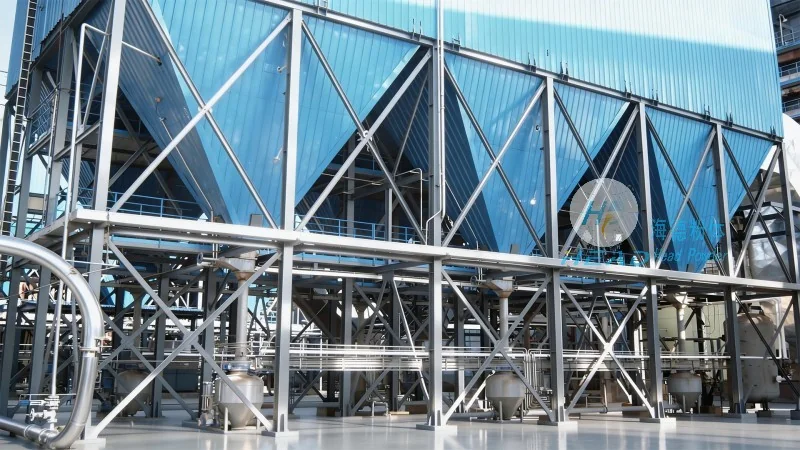
The working principle of the copper sulfate pneumatic conveying equipment is based on the principles of fluid dynamics and particle transport. Compressed air is used as the conveying medium, creating a flow that entrains the copper sulfate particles and moves them through the pipeline. The velocity of the air and the size of the particles determine the efficiency of the conveying process. The system is designed to handle various particle sizes and flow rates, ensuring that the copper sulfate is transported without clogging or excessive pressure drop. The use of filters and cyclones in the system helps to maintain the quality of the copper sulfate by removing any contaminants that may be present in the material or the air.
Key Features and Benefits
Our copper sulfate pneumatic conveying equipment offers several advantages over traditional methods of material handling. The system is compact and can be installed in various locations, making it suitable for both new and existing facilities. The use of compressed air eliminates the need for mechanical components such as conveyors or elevators, reducing maintenance costs and increasing operational reliability. The equipment is also designed to minimize dust emissions, improving workplace safety and environmental compliance. Additionally, the system can handle large volumes of copper sulfate, making it an efficient solution for high-throughput applications.
Application and Industry Use
The copper sulfate pneumatic conveying equipment is widely used in various industries where copper sulfate is a key component. In agriculture, it is used as a fungicide and fertilizer, and the equipment ensures that the material is transported safely and efficiently to the application sites. In water treatment, copper sulfate is used to control algae growth, and the system helps to deliver the material to the treatment plants without contamination. In industrial applications, it is used in the production of pigments, batteries, and other products, and the equipment ensures that the material is handled with precision and care.
Maintenance and Safety Considerations
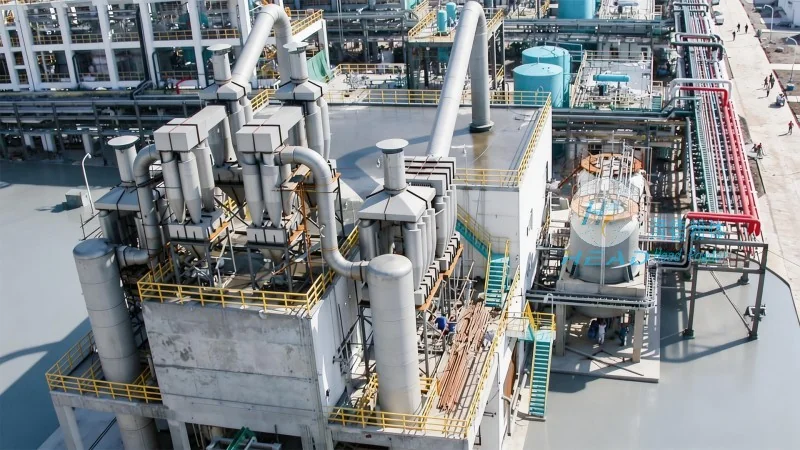
Proper maintenance and safety measures are essential for the optimal performance and longevity of the copper sulfate pneumatic conveying equipment. Regular inspection of the hopper, feeder, and conveying line is necessary to ensure that there are no blockages or leaks. The filters and cyclones should be cleaned or replaced as needed to maintain their efficiency. The system should be operated within the specified pressure and flow rates to prevent damage to the components. Additionally, safety measures such as dust suppression systems and proper ventilation should be implemented to protect the operators from exposure to copper sulfate dust.
Conclusion
HeadPowder's copper sulfate pneumatic conveying equipment is a reliable and efficient solution for the transportation of copper sulfate. By understanding the operation process and working principle of the equipment, users can ensure optimal performance and maintain product quality. With our expertise and commitment to quality, we provide equipment that meets the highest standards of performance and safety, helping our clients to achieve their production goals while minimizing operational costs.