

Operation Process and Working Principle of Dust Removal Ash Material Conveying System
Shandong HeadPowder Engineering Co., Ltd. specializes in providing efficient and reliable solutions for material conveying systems, particularly focusing on the handling of dust removal ash. The company, commonly known as headpowder, is headquartered in Shandong, China, and has established itself as a leading provider in the field of industrial material transport. This article delves into the operation process and working principle of the dust removal ash material conveying system, highlighting the key components, operational mechanisms, and the benefits of such systems in industrial applications.
Key Components of the Conveying System
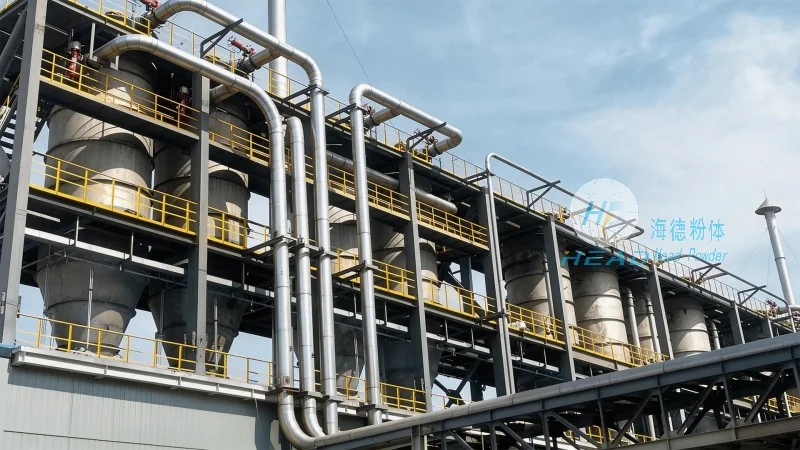
The dust removal ash material conveying system typically consists of several critical components that work in tandem to ensure smooth and efficient material transport. The primary components include the ash collection hopper, the conveyor belt or screw mechanism, the drive system, and the control panel. The ash collection hopper is designed to receive and store the dust removal ash, which is then transferred to the conveyor system. The conveyor belt or screw conveyor is responsible for transporting the ash from the hopper to the designated discharge point. The drive system, often powered by electric motors, provides the necessary force to move the conveyor, while the control panel allows operators to monitor and adjust the system's performance as needed. Each component is engineered to withstand the abrasive nature of ash particles and to maintain high operational efficiency over extended periods.
Operation Process of the Conveying System
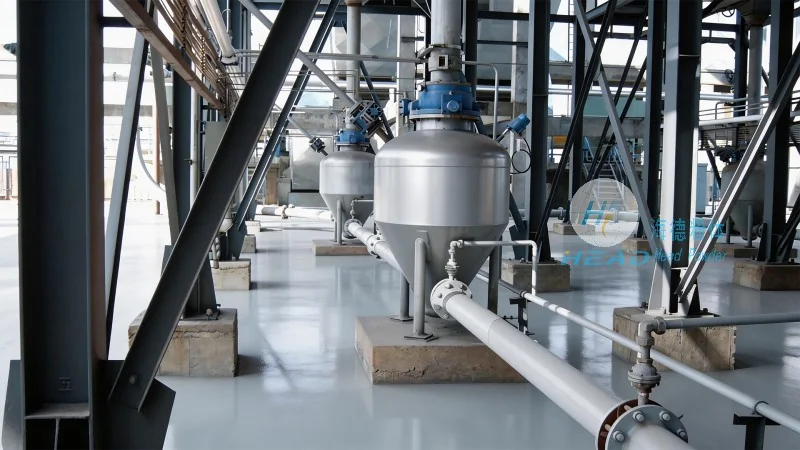
The operation of the dust removal ash material conveying system follows a systematic process that ensures consistent and reliable material transport. Initially, the ash is collected in the hopper through the dust removal process from industrial furnaces or other sources. Once the hopper is filled to a certain level, the conveyor system is activated. The drive motor engages, causing the conveyor belt or screw to rotate, which then moves the ash from the hopper to the discharge point. The system operates continuously, with the control panel monitoring the flow rate and ensuring that the conveyor does not overload. In case of any blockage or abnormal operation, the control panel triggers an alarm or automatically stops the system to prevent damage. The discharge point is typically connected to a storage silo or a transport vehicle, allowing the ash to be further processed or disposed of according to industrial regulations. The entire process is designed to minimize downtime and maximize throughput, making it an essential part of modern industrial operations.
Working Principle of the Conveying System
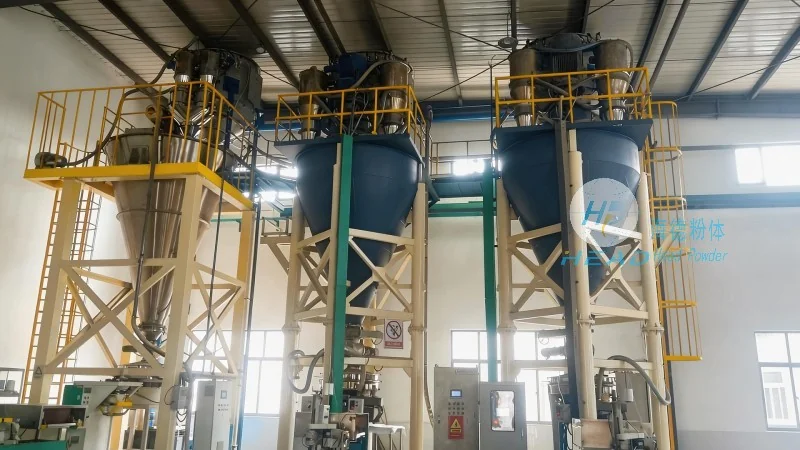
The working principle of the dust removal ash material conveying system is based on mechanical energy transfer and material handling technology. The system utilizes a conveyor mechanism, such as a belt conveyor or a screw conveyor, to move the ash from the collection point to the discharge point. The belt conveyor operates by using a continuous belt loop that is driven by a motor, with the ash placed on the belt and carried to the end. The screw conveyor, on the other hand, uses a rotating screw to push the ash forward through a tube or trough. Both mechanisms rely on the principle of gravity and mechanical force to transport the material. The control system plays a crucial role in regulating the speed and direction of the conveyor, ensuring that the ash is moved at an optimal rate. The system is also equipped with safety features, such as overload protection and emergency stop buttons, to prevent accidents and ensure the safety of operators. By integrating these components, the dust removal ash material conveying system achieves high efficiency and reliability in handling abrasive and heavy materials.
Benefits and Applications
The dust removal ash material conveying system offers several benefits that make it an ideal solution for industrial applications. Firstly, it provides a safe and efficient method for handling dust removal ash, reducing the risk of manual handling and associated health hazards. The system minimizes dust exposure, which is a significant concern in industrial environments, thereby improving workplace safety. Secondly, the system enhances operational efficiency by automating the material transport process, reducing labor costs and increasing throughput. The continuous operation of the conveyor ensures that the ash is transported consistently, without interruptions, which is crucial for maintaining production schedules. Additionally, the system is designed to be durable and low-maintenance, with components that are resistant to wear and tear from ash particles. This reduces the need for frequent repairs and replacements, lowering the overall operational costs. The applications of this system are widespread, including power plants, cement factories, and other industrial facilities that generate large quantities of ash. By using the dust removal ash material conveying system, these facilities can effectively manage their waste materials, comply with environmental regulations, and improve their overall operational performance.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced dust removal ash material conveying systems that are designed to meet the demanding requirements of industrial applications. The operation process and working principle of these systems are based on robust engineering and efficient technology, ensuring high performance and reliability. By integrating key components such as the ash collection hopper, conveyor mechanism, and control system, the company offers solutions that enhance workplace safety, improve operational efficiency, and reduce costs. The dust removal ash material conveying system is a critical component in modern industrial operations, and with the expertise of headpowder, facilities can achieve optimal material transport and waste management. As a leading provider in the field, headpowder continues to innovate and develop new solutions to meet the evolving needs of the industry.