

Operation Process and Working Principle of Coffee Bean Material Handling Systems
For coffee processing facilities, efficient material handling is crucial to maintaining production efficiency and product quality. The coffee bean material handling system, developed by Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder), is a specialized solution designed to streamline the movement of coffee beans from storage to processing stages. This system integrates advanced engineering principles and robust components to ensure reliable and consistent operation in coffee production environments.
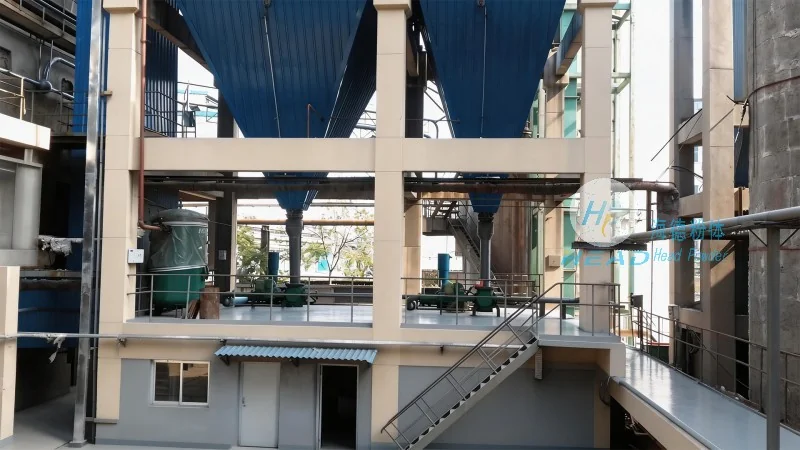
Overview of the Coffee Bean Material Handling System
The coffee bean material handling system is engineered to handle various types of coffee beans, including green coffee beans, roasted coffee beans, and coffee grounds. It features a modular design that allows for customization based on the specific needs of coffee processing plants. The system typically includes components such as hoppers, conveyors, elevators, and control panels, all working in tandem to facilitate smooth material flow. HeadPowder's expertise in material handling technology ensures that each component is optimized for durability, efficiency, and minimal maintenance, making it a reliable choice for coffee manufacturers seeking to enhance their production workflows.
Key Components and Their Functions
The system's core components play critical roles in the overall operation. The hopper serves as the initial storage and feeding unit, where coffee beans are loaded and prepared for transport. It is designed with a sloped bottom to facilitate gravity-fed movement of the beans into the conveyor system. The conveyor, often a belt or chain-type design, is responsible for transporting the coffee beans horizontally or at an incline. This component is equipped with adjustable speed controls to match the processing capacity of the facility. The elevator, or vertical conveyor, is used to lift coffee beans from lower to higher levels, such as from storage silos to processing machinery. The control panel integrates sensors and automation technology to monitor and regulate the system's operation, ensuring that the flow of coffee beans is consistent and safe.
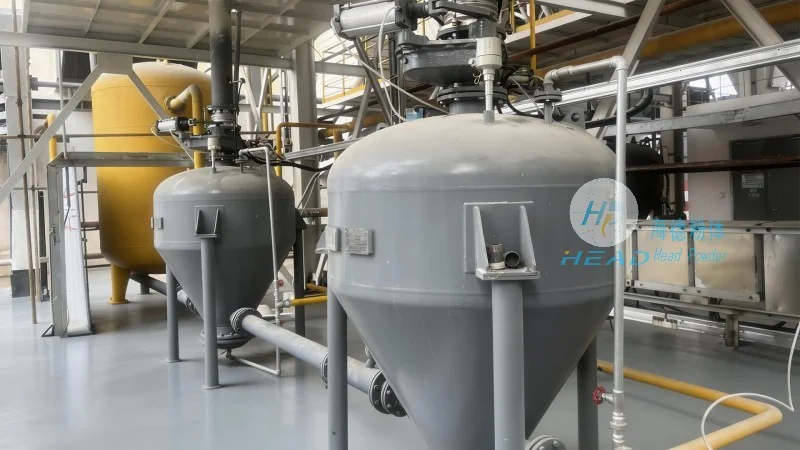
Operation Process: Step-by-Step Workflow
The operation of the coffee bean material handling system follows a systematic workflow that begins with the loading of coffee beans into the hopper. Once loaded, the beans are released into the conveyor system, where they are transported to the processing area. The conveyor's speed is adjusted based on the processing requirements, ensuring that the beans move at an optimal rate. The elevator then lifts the beans to the desired height, where they are fed into the next stage of processing, such as roasting or grinding. Throughout the process, the control panel continuously monitors the system's performance, detecting any blockages or malfunctions and triggering appropriate alerts. This real-time monitoring helps maintain the system's efficiency and prevents downtime, which is critical for coffee production plants that operate on tight schedules.
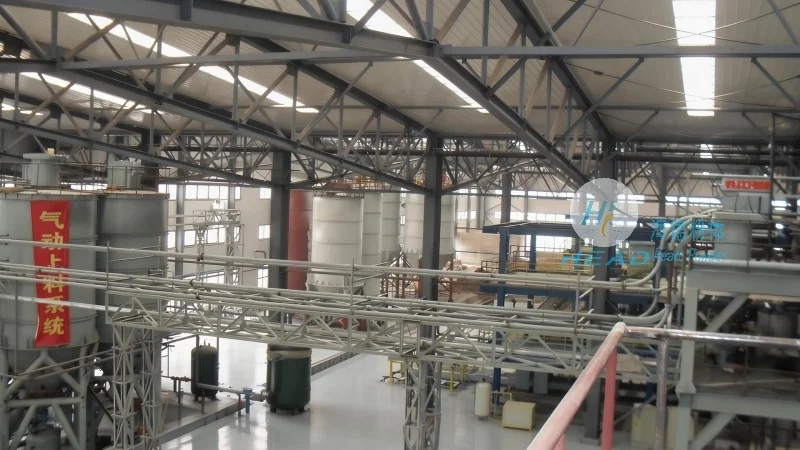
Working Principle: How the System Ensures Efficiency
The working principle of the coffee bean material handling system is based on the principles of gravity and mechanical motion. The hopper's sloped design allows coffee beans to move by gravity, reducing the need for additional power for initial movement. The conveyor system uses mechanical power to transport the beans horizontally, while the elevator utilizes a combination of gravity and motor-driven mechanisms to lift the beans vertically. The control panel integrates sensors that detect the position and flow rate of the beans, providing data to the automation system. This data is used to adjust the speed of the conveyor and elevator, ensuring that the system operates at peak efficiency. The system's design also incorporates safety features, such as emergency stop buttons and overload protection, to prevent accidents and ensure the safety of operators.
Benefits of Using the Coffee Bean Material Handling System
Implementing the coffee bean material handling system from HeadPowder offers several benefits to coffee processing facilities. Firstly, it enhances production efficiency by reducing the time and labor required to move coffee beans between stages. The system's modular design allows for easy integration with existing processing equipment, minimizing the need for extensive modifications. Secondly, it improves product quality by ensuring consistent and uniform movement of coffee beans, which reduces the risk of damage or contamination. Thirdly, the system's advanced control panel provides real-time monitoring and data analysis, enabling facility managers to identify and address issues promptly. Finally, the system's durability and low maintenance requirements result in long-term cost savings for coffee manufacturers.