

Operation Process and Working Principle of a Dust-Free Bulk Material Bag-In Bulk Loading Station wit
For industrial applications requiring efficient and clean handling of bulk powders, the dust-free bag-in bulk loading station with pneumatic conveying line is a critical piece of equipment. This system, designed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers a comprehensive solution for seamless material transfer while maintaining a clean and safe working environment. The following article provides an in-depth look at the operation process and working principle of this advanced system.
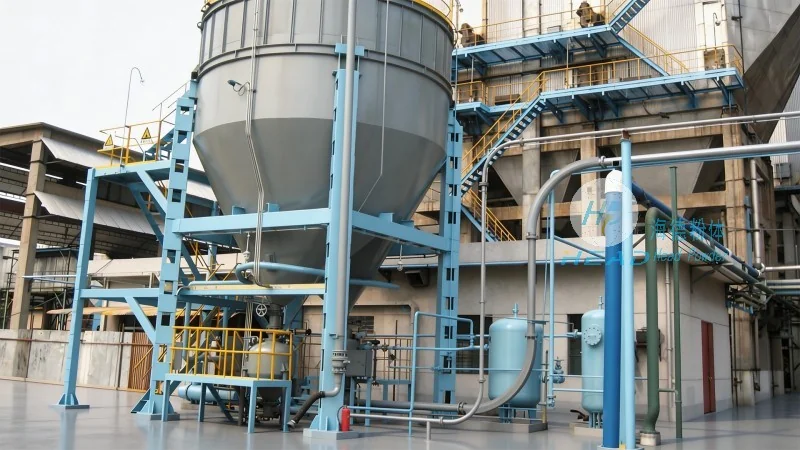
Overview of the Dust-Free Bag-In Bulk Loading Station
The dust-free bag-in bulk loading station is engineered to handle the transfer of bulk materials from sealed bags into a processing or storage system without generating dust or contamination. This is achieved through a combination of advanced pneumatic conveying technology and a sealed, enclosed design that ensures all material handling occurs within a controlled environment. The system is particularly suitable for industries such as pharmaceuticals, food processing, chemicals, and fine chemicals, where product purity and operator safety are paramount.
Key Components and Their Functions
The system comprises several key components, each playing a vital role in the overall operation. These include the bag opening mechanism, the pneumatic conveying line, the dust collection system, and the material storage or processing unit. The bag opening mechanism is designed to safely and efficiently open the sealed bags without exposing the material to the air, thus preventing dust generation. The pneumatic conveying line uses compressed air to transport the material from the bag to the processing area, while the dust collection system ensures that any particles that may escape are captured and filtered. The material storage or processing unit is where the bulk material is transferred for further use or processing.
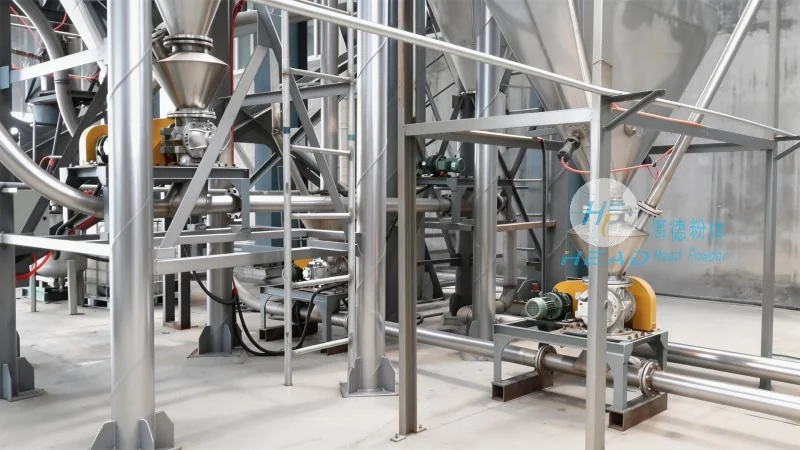
Operation Process of the Pneumatic Conveying Line
The operation of the dust-free bag-in bulk loading station begins with the placement of a sealed bag into the designated loading position. The bag opening mechanism then activates, carefully cutting or tearing the bag's seal to allow the material to be released. Simultaneously, the pneumatic conveying system is activated, and compressed air is introduced into the line. This creates a pressure differential that draws the material from the bag and transports it through the conveying line to the processing or storage unit. The material is then deposited into the receiving vessel or hopper, completing the transfer process. The entire operation is automated, with sensors and controls ensuring that the process runs smoothly and efficiently.
Working Principle of the Pneumatic Conveying System
The working principle of the pneumatic conveying line is based on the use of compressed air to move bulk materials. In this system, the material is suspended in a stream of air and carried through the conveying line. The air flow is controlled to maintain a consistent velocity, ensuring that the material is transported without causing blockages or excessive wear on the system components. The system uses a combination of positive and negative pressure to move the material, with the positive pressure used to draw the material from the bag and the negative pressure used to maintain the flow through the line. The dust collection system is integrated into the line to capture any particles that may be released during the transfer process, ensuring that the air leaving the system is clean and free of contaminants.
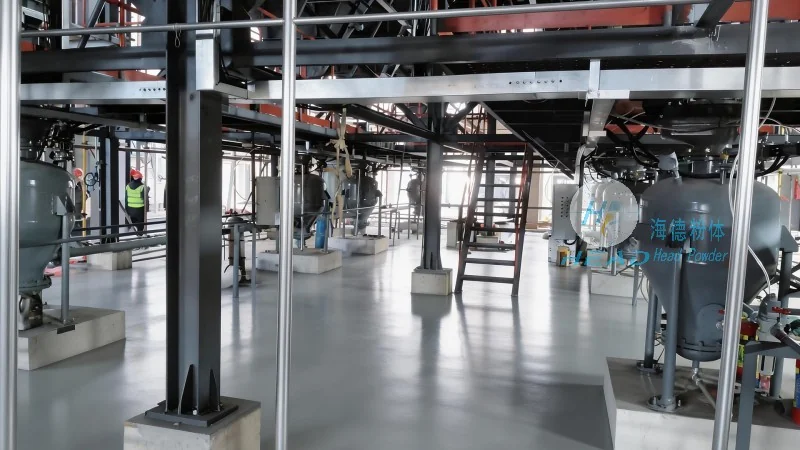
Advantages of the Dust-Free Bag-In Bulk Loading Station
One of the primary advantages of this system is its ability to handle bulk materials without generating dust or contamination. This is crucial for industries where product purity is a critical factor, as it prevents cross-contamination and ensures that the final product meets the required quality standards. Additionally, the system is highly efficient, with the ability to transfer large quantities of material quickly and with minimal downtime. The automated operation reduces the need for manual handling, improving safety and reducing the risk of accidents. The sealed design also minimizes the risk of material exposure to the environment, which is particularly important for hazardous or sensitive materials.
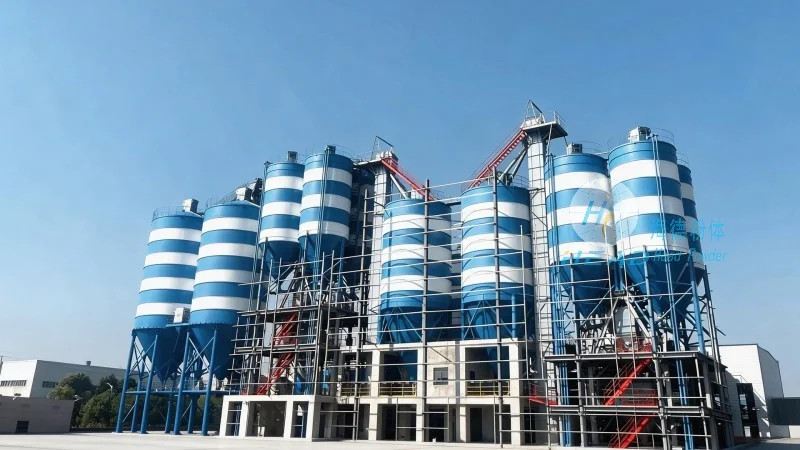
Application Examples and Industry Impact
The dust-free bag-in bulk loading station with pneumatic conveying line is widely used in various industries. In the pharmaceutical industry, it is used to transfer active pharmaceutical ingredients (APIs) and other raw materials into processing lines, ensuring that the materials remain pure and free of contaminants. In the food processing industry, it is used to handle ingredients such as flour, sugar, and spices, maintaining the quality and safety of the final products. In the chemical industry, it is used to transfer chemicals and other materials, ensuring that the process is efficient and safe. The system has a significant impact on the efficiency and safety of industrial operations, reducing the risk of accidents and improving the overall quality of the products.
Conclusion and Future Developments
The dust-free bag-in bulk loading station with pneumatic conveying line is an advanced and efficient system for handling bulk materials. Designed by Shandong HeadPowder Engineering Co., Ltd., it offers a comprehensive solution for industries requiring clean and safe material transfer. The system's operation process and working principle are based on advanced technology and careful engineering, ensuring that it meets the highest standards of performance and safety. As technology continues to advance, the system is likely to evolve to include even more advanced features, such as real-time monitoring and predictive maintenance, further enhancing its efficiency and reliability.