

Working Principle and Features of a Metering Bin Pump Pneumatic Conveying System
For industrial applications requiring efficient and reliable material handling, the metering bin pump pneumatic conveying system stands out as a versatile solution. This system is designed to transport bulk materials with precision and control, making it ideal for various industries such as chemical, food processing, and pharmaceuticals. Understanding its working principle and key features is essential for selecting the right equipment for specific operational needs.
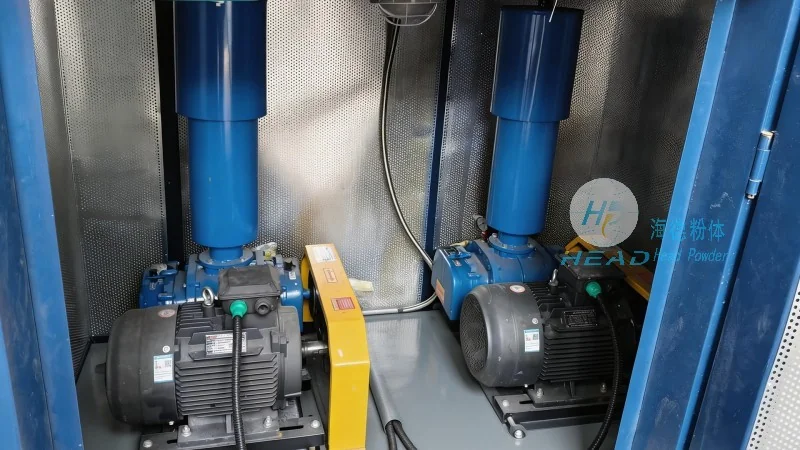
Introduction to Metering Bin Pump Pneumatic Conveying Systems
A metering bin pump, also known as a bin venturi or a pressure bin, is a critical component in pneumatic conveying systems. It combines the functions of a storage bin with a pumping mechanism, allowing for controlled discharge of materials. The system typically consists of a hopper, a pump unit, a conveying line, and a receiver. This integrated approach ensures that materials are transported safely and efficiently from the source to the destination.
Working Principle of the System
The operation of a metering bin pump pneumatic conveying system relies on the principles of air pressure and vacuum. The process begins with the material being fed into the storage bin. When the pump is activated, it creates a vacuum or pressure differential within the conveying line. This differential draws the material from the bin into the pump chamber. The pump then uses a rotating impeller or a piston to compress the material-air mixture, forcing it through the conveying line to the receiver. The system maintains a consistent flow rate by controlling the air pressure and the speed of the pump, ensuring that the material is transported without blockages or excessive pressure buildup.
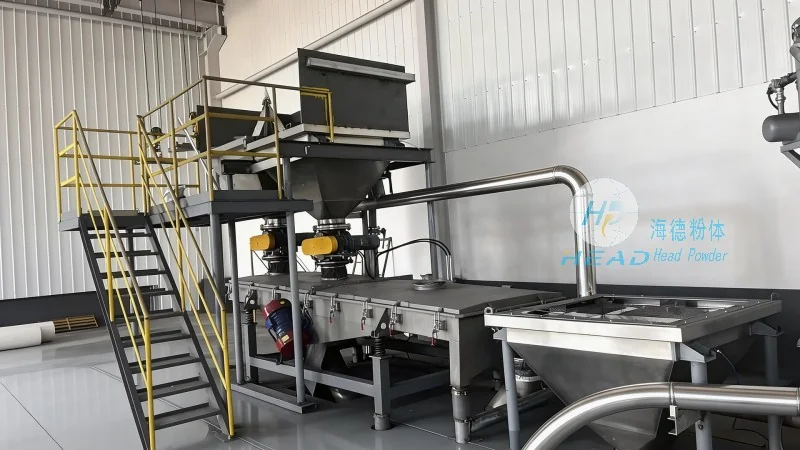
Key Features and Advantages
One of the primary advantages of this system is its ability to handle a wide range of materials, from fine powders to bulk solids. The metering bin pump provides precise control over the discharge rate, which is crucial for processes that require exact material quantities. Additionally, the system is compact and can be integrated into existing facilities, reducing installation time and costs. The pneumatic conveying method minimizes material degradation and contamination, making it suitable for sensitive products. Another key feature is the system's energy efficiency, as it uses compressed air only when needed, optimizing operational costs.
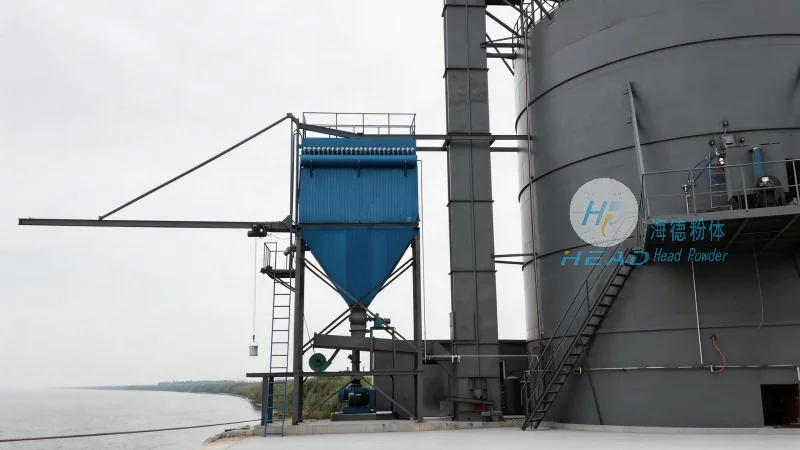
Application Scenarios and Benefits
The metering bin pump pneumatic conveying system is widely used in industries where material handling demands accuracy and reliability. In the chemical industry, it is used to transport powders and granules, ensuring that the process flow is consistent and that product quality is maintained. In food processing, the system is ideal for handling ingredients such as flour, sugar, and spices, as it prevents cross-contamination and maintains product integrity. The pharmaceutical industry also benefits from this system, as it allows for the safe and controlled transport of raw materials and finished products. The benefits extend to reduced labor costs, as the system operates automatically, and lower maintenance requirements due to its robust design.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial material handling equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable pneumatic conveying solutions. HeadPowder's expertise lies in designing and manufacturing metering bin pumps and other related systems that meet the highest industry standards. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled workforce to produce top-tier equipment. HeadPowder's commitment to customer satisfaction and product excellence has made it a preferred choice for clients worldwide.