

Working Principle and Features of Dust-Free Powder Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced dust-free powder pneumatic conveying systems. These systems are essential for industries that require precise, contamination-free material handling, such as pharmaceuticals, food processing, and chemical manufacturing. The following article explores the working principle and key features of these systems, highlighting their efficiency and reliability.
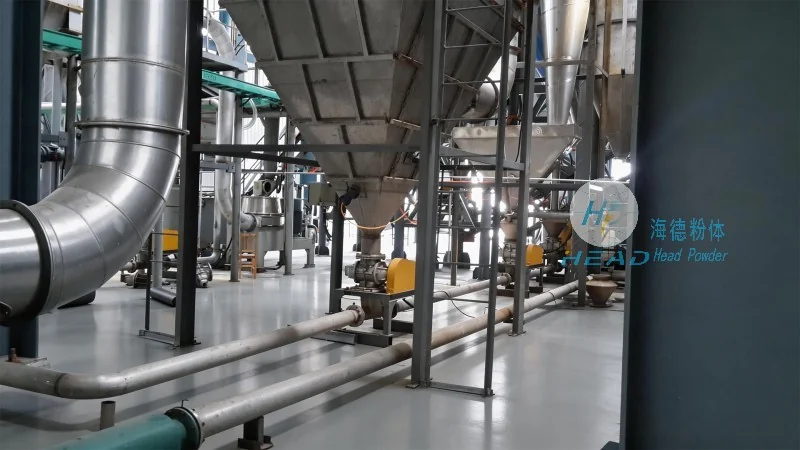
Working Principle of the Dust-Free Powder Pneumatic Conveying Line
The core of a dust-free powder pneumatic conveying system lies in its ability to transport dry powders through an enclosed pipeline using compressed air or vacuum. The process typically involves several key components: a feeder to introduce the powder into the system, a conveying line to transport it, and a separator to collect the material at the destination. In a positive pressure system, compressed air is used to push the powder forward, while a negative pressure system uses suction to draw the material. The design of these systems emphasizes airtight seals and filtration to prevent dust leakage and maintain a clean environment. For example, in a pharmaceutical application, the system must meet stringent GMP (Good Manufacturing Practice) standards, ensuring that no contaminants enter the product stream. The headspace of the conveying line is often equipped with HEPA filters to capture any airborne particles, maintaining a particle-free zone throughout the process.
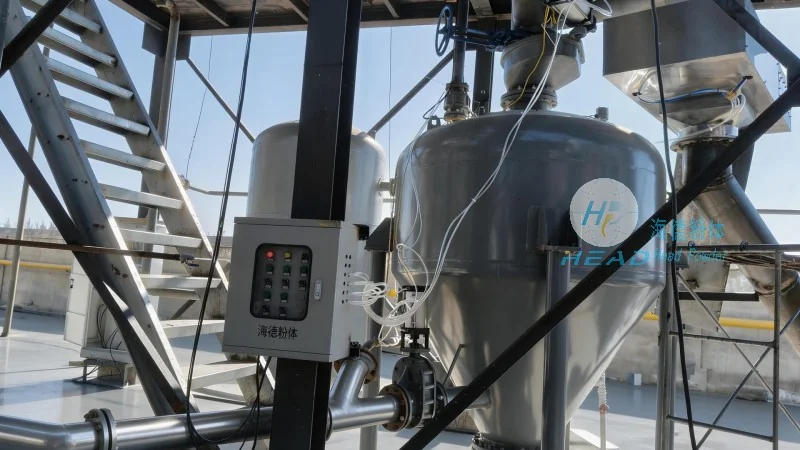
Key Features of the Dust-Free Powder Pneumatic Conveying System
One of the primary features of the dust-free powder pneumatic conveying system is its ability to handle a wide range of powder characteristics, including fine powders, bulk powders, and even cohesive materials. The system is designed to operate with minimal pressure differentials, reducing energy consumption and wear on components. Another critical feature is its self-cleaning capability, which prevents material buildup in the pipeline and ensures consistent performance over time. The system also includes safety features such as pressure relief valves and overcurrent protection to prevent accidents and equipment damage. Additionally, the modular design allows for easy integration with existing production lines, enabling manufacturers to upgrade their material handling capabilities without major disruptions.
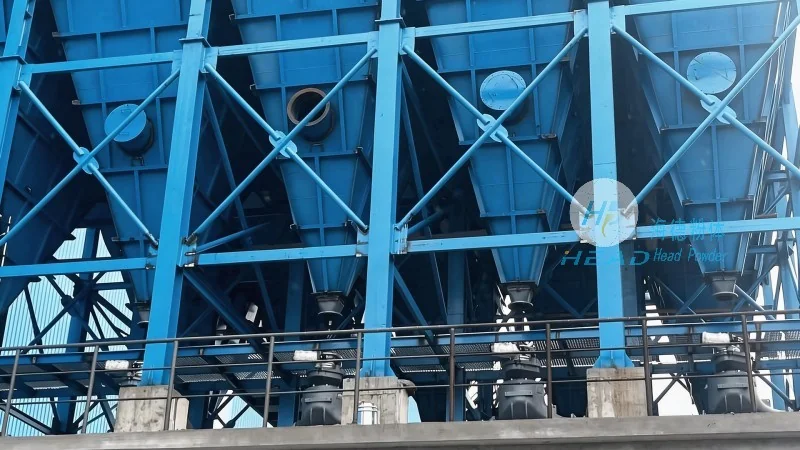
Technical Advantages and Practical Applications
The dust-free powder pneumatic conveying system offers several technical advantages that make it a preferred choice for industries with strict cleanliness requirements. For instance, the system can transport powders over long distances with minimal loss, making it suitable for large-scale production facilities. The low maintenance requirements and high reliability reduce downtime and operational costs, contributing to overall efficiency. In practical applications, these systems are commonly used in the production of pharmaceuticals, where the purity of the final product is paramount. They are also widely used in the food industry to handle ingredients like flour, sugar, and spices, ensuring that the product remains free from contaminants. In the chemical industry, the system is used to transport reactive powders safely, preventing dust explosions and maintaining a safe working environment. The system's adaptability to different powder types and its ability to integrate with automated processes further enhance its value in modern manufacturing.
Company Information and Service Commitment
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable company dedicated to developing and manufacturing high-quality dust-free powder pneumatic conveying systems. With years of experience in the industry, the company has built a strong reputation for its innovative solutions and commitment to customer satisfaction. The company's products are designed to meet international standards and are backed by a team of skilled engineers and technicians who provide comprehensive support, including installation, maintenance, and technical training. By choosing HeadPowder, manufacturers can benefit from reliable, efficient, and cost-effective material handling solutions that enhance their production processes and ensure compliance with industry regulations.