

Principles and Working Scene Characteristics of Powdered Food Additive Conveying
Conveying powdered food additives is a critical process in the food and pharmaceutical industries, ensuring efficient and safe transfer of these materials from one location to another. The principles and working scene characteristics of such systems are essential for maintaining product quality, operational efficiency, and regulatory compliance. This article explores the fundamental principles behind powdered food additive conveying and highlights the key characteristics of various working scenarios.
Core Principles of Powdered Food Additive Conveying
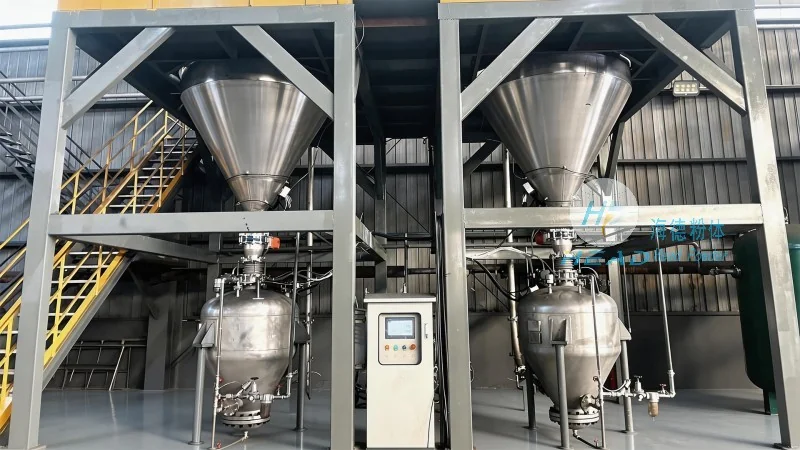
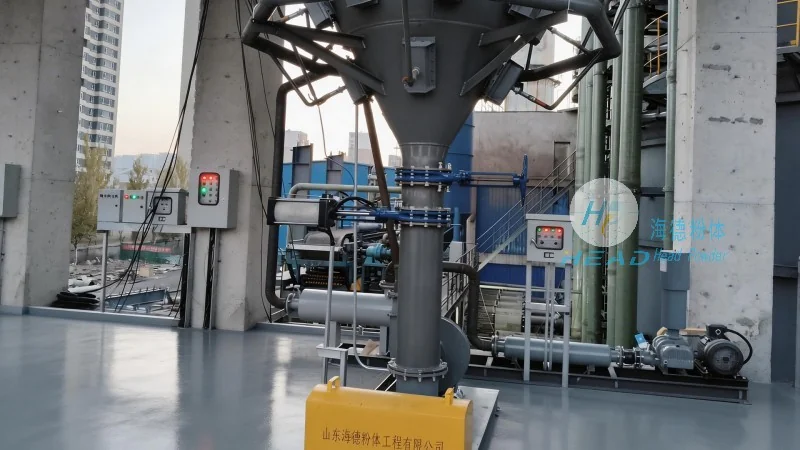
The primary goal of conveying powdered food additives is to transport these fine particles reliably and without degradation. Several core principles underpin the design and operation of these systems. First, the choice of conveying method—whether mechanical, such as screw conveyors or belt conveyors, or pneumatic, like air-swept or pressure systems—depends on factors like the particle size, moisture content, and bulk density of the additive. For food additives, which often have low bulk density and can be sensitive to moisture, pneumatic conveying is frequently preferred due to its ability to handle fine powders and maintain a controlled environment. The principle of fluidization, where the powder is suspended in a moving gas stream, is central to pneumatic systems, ensuring consistent flow and preventing clogging. Additionally, the design of the conveying line, including the use of appropriate ductwork, bends, and filters, is crucial to minimize particle degradation and maintain product integrity. The selection of materials for the conveying equipment, such as stainless steel or food-grade plastics, is also critical to prevent contamination and ensure compliance with food safety regulations.
Working Scene Characteristics and Application Scenarios
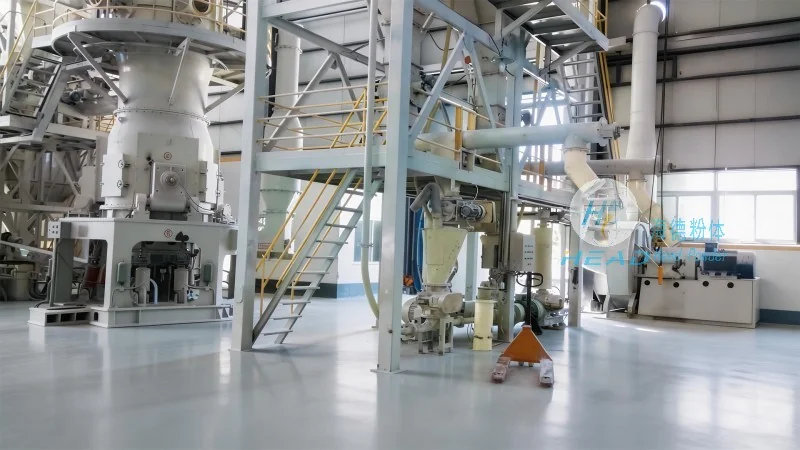
The working scene characteristics of powdered food additive conveying vary significantly based on the specific application and operational environment. In industrial food processing facilities, for example, conveying systems are often integrated into larger production lines, requiring seamless coordination with mixing, packaging, and quality control processes. These scenarios demand high throughput and reliability, as delays in the supply of additives can disrupt the entire production schedule. The working environment in such settings is typically characterized by high humidity and temperature fluctuations, necessitating equipment that can withstand these conditions while maintaining consistent performance. In contrast, pharmaceutical applications for powdered food additives, such as in nutraceutical or dietary supplement manufacturing, may involve more stringent regulatory requirements. Here, the conveying systems must adhere to GMP (Good Manufacturing Practice) standards, with features like closed-loop systems, dust collection, and traceability to prevent cross-contamination and ensure product safety. The working scene may also involve smaller batch sizes and more frequent changes in product types, requiring flexible and modular conveying solutions. Another key characteristic is the need for precise control over the flow rate and pressure, as even minor variations can affect the final product quality. For instance, in the production of powdered beverages or instant foods, the uniform distribution of additives is critical to achieve consistent flavor and texture. The working scene may also involve integration with automated dosing systems, where the conveying equipment must provide accurate and repeatable dosing to meet product specifications.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
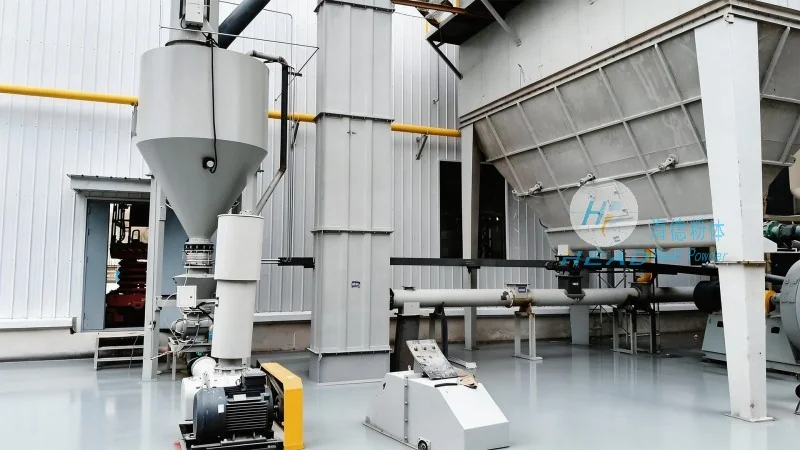
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading provider of specialized conveying solutions for the food and pharmaceutical industries. Headquartered in Shandong, China, the company has established itself as a trusted partner for businesses seeking reliable and efficient systems for handling powdered food additives. With a strong focus on innovation and quality, HeadPowder offers a range of conveying equipment tailored to the unique needs of its clients. The company’s products include pneumatic conveying systems, screw conveyors, and bulk handling solutions, all designed to meet the stringent requirements of food safety and regulatory compliance. HeadPowder’s expertise lies in understanding the specific challenges of powdered food additive conveying, such as handling fine particles, preventing clogging, and maintaining product integrity. By leveraging advanced engineering and manufacturing capabilities, the company provides customized solutions that enhance operational efficiency and reduce downtime. The company’s commitment to customer satisfaction and product excellence has earned it a reputation as a leading provider in the industry. HeadPowder continues to expand its product portfolio and service offerings, ensuring that clients have access to the latest technologies and solutions for their conveying needs. With a dedicated team of engineers and technicians, HeadPowder is well-positioned to support the growing demands of the food and pharmaceutical sectors.