

Principles and Operational Characteristics of Powder Mixing and Conveying Systems for Ingredient Pre
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder handling systems. These systems are crucial for industries that rely on precise ingredient mixing and efficient material transport. The core of such systems lies in the integration of mixing mechanisms and conveying technologies, enabling seamless processing of bulk powders from various sources.
Principles of Powder Mixing and Conveying Systems
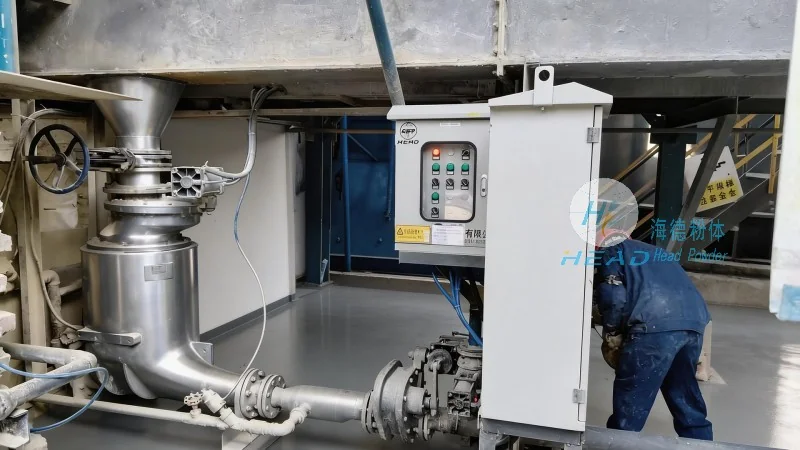
The fundamental principle of a powder mixing and conveying system is to ensure uniform blending of different ingredients while facilitating their movement through pipelines or other transport channels. The system typically comprises several key components, including a mixing chamber, a conveying mechanism (such as pneumatic or mechanical systems), and control units. The mixing process involves the introduction of raw materials into the chamber, where they are agitated to achieve a homogeneous mixture. This is often achieved through rotating blades, paddles, or other mixing tools that break down agglomerates and ensure thorough contact between particles. The conveying stage then transports the mixed powder to the next processing stage, such as packaging or further processing. The control system monitors parameters like speed, pressure, and temperature to maintain optimal performance and product quality.
Operational Characteristics in Different Industrial Scenarios
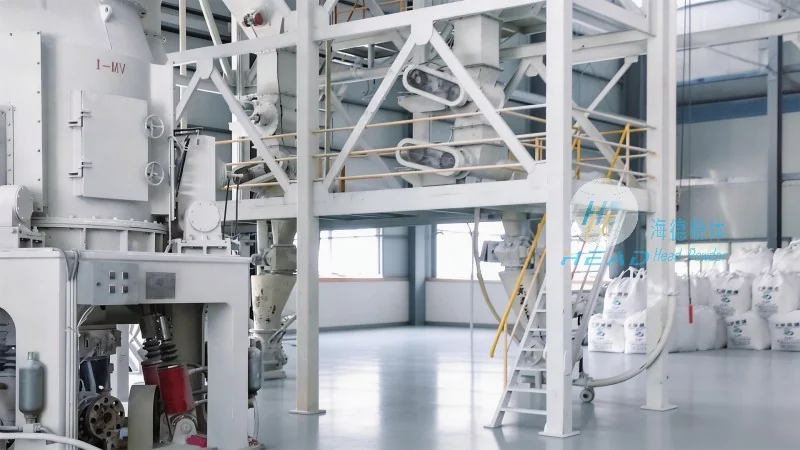
The operational characteristics of powder mixing and conveying systems vary significantly based on the specific industrial application. In the chemical industry, for example, these systems must handle a wide range of chemical powders, often with strict safety and contamination control requirements. The systems are designed to minimize dust generation and ensure compliance with environmental regulations. In the food and pharmaceutical sectors, the focus shifts to hygiene, sterilization, and precise dosing. These industries demand systems that can maintain sterile conditions, prevent cross-contamination, and deliver ingredients with high accuracy. The versatility of HeadPowder's systems allows them to adapt to these diverse needs, providing customized solutions that meet the unique challenges of each application.
Key Features and Advantages
HeadPowder's powder mixing and conveying systems are engineered with several advantages that enhance operational efficiency and product quality. One of the primary features is the ability to handle a wide range of powder properties, including different particle sizes, densities, and flow characteristics. This flexibility allows the system to process materials from fine powders to coarse granules without compromising performance. Another key advantage is the integration of real-time monitoring and control, which enables operators to adjust parameters dynamically based on process feedback. This leads to improved consistency and reduced waste. Additionally, the systems are designed for easy maintenance and cleaning, which is critical in industries where hygiene is paramount. The robust construction and use of high-quality materials ensure long-term reliability and minimal downtime, contributing to overall operational cost savings.
Conclusion
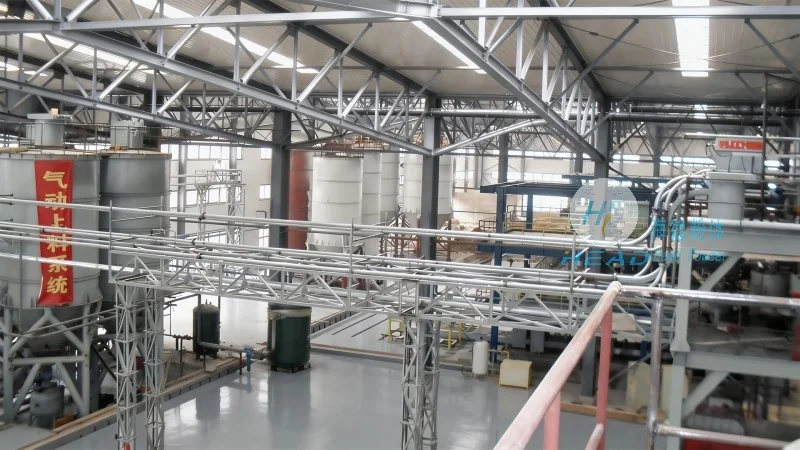
HeadPowder's powder mixing and conveying systems represent a sophisticated solution for industries requiring precise ingredient preparation and efficient material transport. By combining advanced mixing technologies with reliable conveying mechanisms, these systems address the diverse needs of various sectors, including chemicals, food, and pharmaceuticals. The company's commitment to innovation and customization ensures that clients receive tailored solutions that enhance productivity, maintain product quality, and comply with industry standards. Based in Shandong, China, HeadPowder continues to lead the way in providing high-performance powder handling solutions that meet the evolving demands of modern manufacturing.