

Principle and Working Scene Characteristics of Sodium Bicarbonate Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design and production of advanced material handling systems tailored for sodium bicarbonate processing. The company, operating from Shandong, China, has developed a comprehensive system that efficiently manages the transportation and handling of sodium bicarbonate, a critical chemical widely used in various industries. This article delves into the underlying principles of the system and highlights its key working scene characteristics, providing insights into its operational efficiency and practical applications.
Working Principle of the Material Handling System
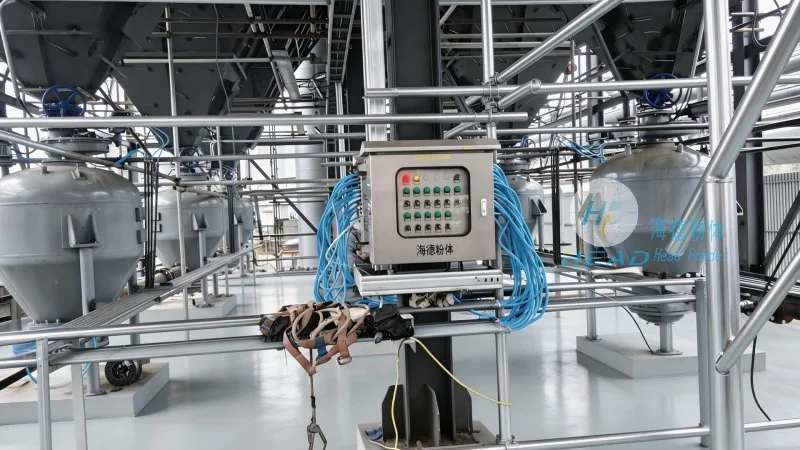
The sodium bicarbonate material handling system operates on a sophisticated mechanism that ensures seamless and safe transportation of the material. At its core, the system integrates multiple components, including conveyor belts, feeding mechanisms, and control systems, to facilitate the movement of sodium bicarbonate from storage to processing units. The feeding mechanism, for instance, uses precision-controlled feeders to regulate the flow rate, preventing overloading or underfeeding that could affect the quality of the material. The conveyor system, equipped with durable materials and robust structures, handles the bulk of sodium bicarbonate, ensuring minimal product degradation and consistent performance. Advanced control systems, often integrated with sensors and automation technology, monitor the entire process in real-time, adjusting parameters as needed to maintain optimal operational conditions. This integrated approach not only enhances the efficiency of material handling but also reduces the risk of operational errors, making it a reliable solution for industrial applications.
Key Working Scene Characteristics
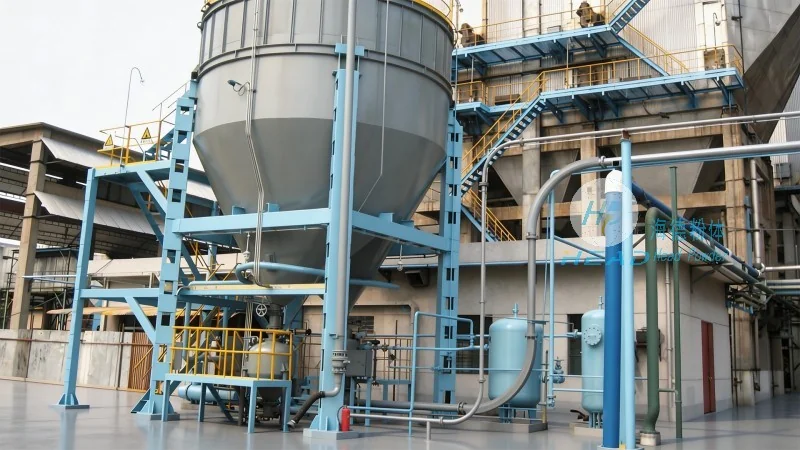
The working scene characteristics of the sodium bicarbonate material handling system are tailored to meet the specific demands of industrial environments. One of the primary characteristics is its adaptability to different processing scales, from small-scale laboratory operations to large-scale industrial production lines. The system is designed to handle varying particle sizes and moisture content of sodium bicarbonate, ensuring consistent performance regardless of the material's physical properties. Another notable characteristic is its energy efficiency, which is achieved through optimized motor selection and energy-saving control strategies. This not only reduces operational costs but also aligns with environmental sustainability goals. The system also features high durability and low maintenance requirements, thanks to the use of high-quality materials and robust construction. This makes it suitable for continuous operation in demanding industrial settings, where downtime can significantly impact productivity. Additionally, the system's modular design allows for easy integration with existing production lines and scalability, enabling businesses to expand their operations without significant modifications.
Application and Operational Benefits
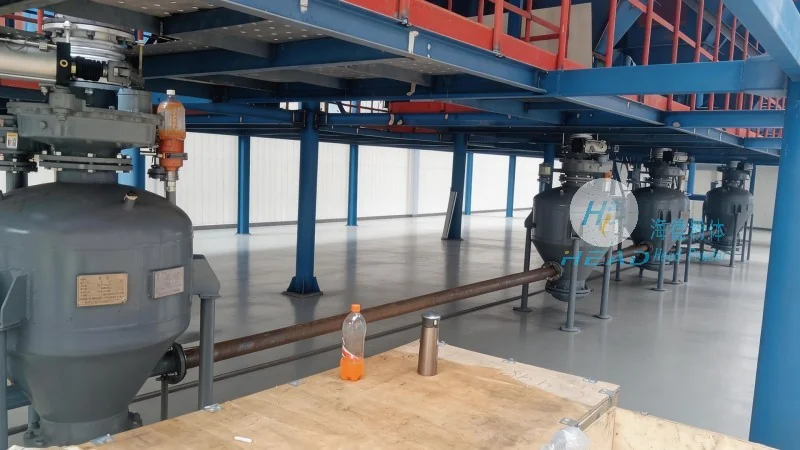
The sodium bicarbonate material handling system is widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, it facilitates the safe and hygienic handling of sodium bicarbonate, which is commonly used as a leavening agent in baking. The system ensures that the material is handled under controlled conditions, preventing contamination and maintaining product quality. In the pharmaceutical sector, the system's precision and cleanliness are crucial, as sodium bicarbonate is used in the formulation of various medications. The system's ability to maintain low contamination levels and consistent particle size distribution makes it an ideal choice for pharmaceutical applications. In chemical manufacturing, the system's robust design and ability to handle bulk quantities make it suitable for processing sodium bicarbonate in large-scale production. The operational benefits of the system extend beyond efficiency, as it also enhances workplace safety by reducing manual handling of the material, thereby minimizing the risk of accidents and injuries. Furthermore, the system's automation capabilities reduce the need for manual intervention, leading to improved operational consistency and reduced labor costs.
Conclusion
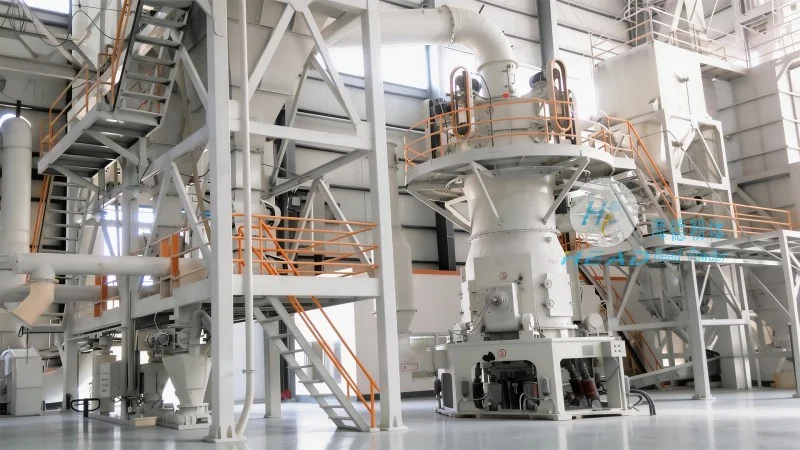
Shandong HeadPowder Engineering Co., Ltd.'s sodium bicarbonate material handling system exemplifies advanced engineering and practical application in material handling technology. By integrating sophisticated principles and tailored working scene characteristics, the system provides a reliable and efficient solution for the transportation and handling of sodium bicarbonate. Its adaptability, energy efficiency, and durability make it a valuable asset for businesses operating in various industries. As the demand for efficient material handling solutions continues to grow, this system stands as a testament to the company's commitment to innovation and quality, ensuring that it remains a leading choice for industrial applications.