

Principle and Working Scene Characteristics of Limestone Powder Material Handling System Equipment
For industrial applications involving limestone powder, efficient material handling is crucial. The limestone powder material handling system, developed by Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder), is designed to meet the demands of various processing environments. This system integrates advanced technology to ensure reliable and efficient transportation of limestone powder, supporting production workflows in mining, construction, and chemical industries.
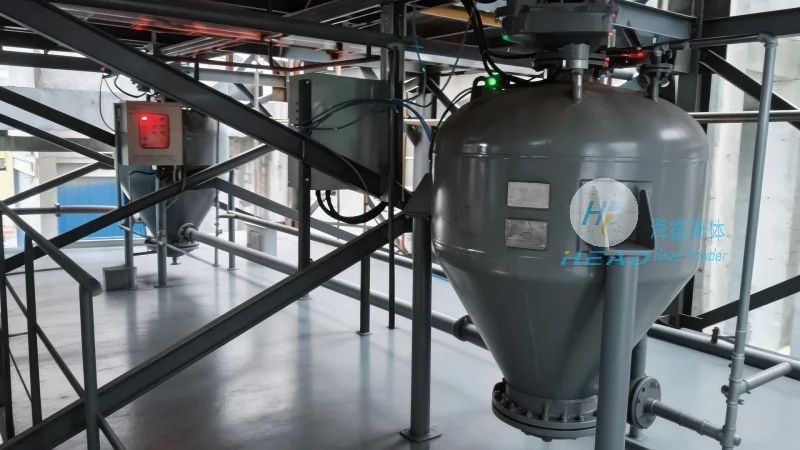
Principle of Operation
The core principle of the limestone powder material handling system lies in its ability to handle fine powders with precision. The system typically incorporates components such as feeders, conveyors, and control units. The feeder ensures a consistent and controlled flow of limestone powder into the conveyor system. The conveyor, often using pneumatic or mechanical methods, transports the powder through pipelines or open channels. Advanced control systems monitor and adjust the flow rate, pressure, and speed to maintain optimal performance. This integrated approach minimizes material loss, reduces dust generation, and enhances overall operational efficiency.
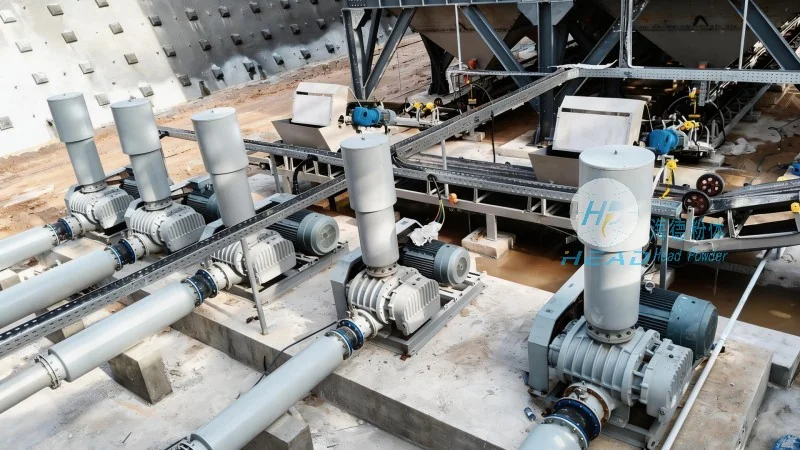
Key Working Scene Characteristics
The limestone powder material handling system is tailored to diverse working environments, each with unique requirements. In mining operations, the system is used to transport limestone from extraction sites to processing facilities, ensuring a continuous supply of raw material. In construction material production, it facilitates the handling of limestone powder for cement and concrete production, where precise dosage and mixing are critical. In chemical processing, the system supports the handling of limestone powder in the production of calcium compounds, where purity and consistency are paramount. The system's adaptability allows it to operate in both indoor and outdoor settings, with options for enclosed or open conveyor systems depending on the specific application and environmental conditions.
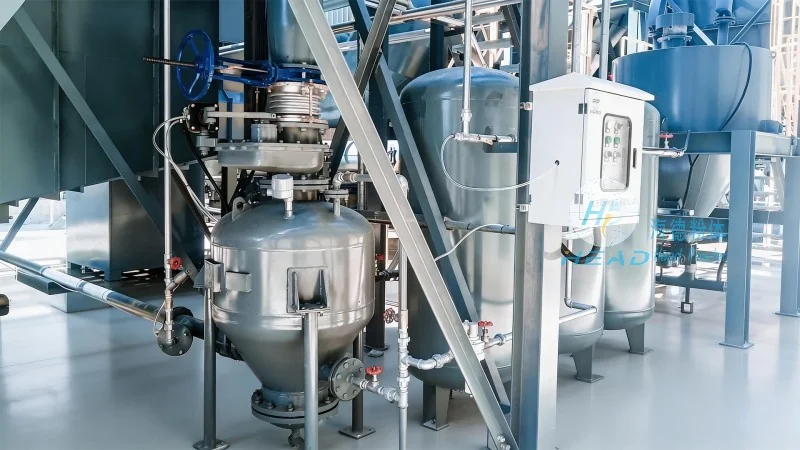
Technical Advantages and Performance
HeadPowder's limestone powder material handling system offers several technical advantages that enhance its performance in real-world applications. The system is designed for high capacity and low maintenance, with components engineered to withstand the abrasive nature of limestone powder. Advanced sealing technologies reduce dust leakage and improve safety in industrial environments. The control system provides real-time monitoring and data logging, enabling operators to optimize performance and troubleshoot issues quickly. Additionally, the system's modular design allows for easy integration with existing production lines and scalability to accommodate increasing production demands.
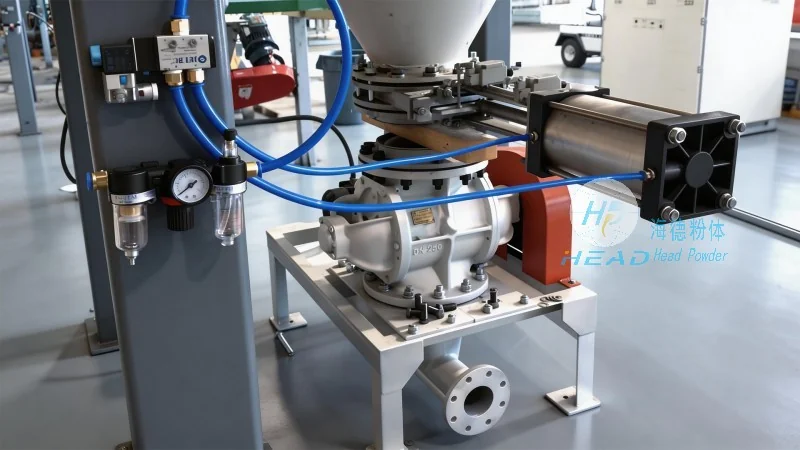
Application Examples and Case Studies
Real-world applications of the limestone powder material handling system demonstrate its effectiveness in various industrial settings. For instance, in a cement plant, the system successfully handled limestone powder from crushing to storage, achieving a throughput of 500 tons per hour with minimal downtime. In a chemical manufacturing facility, the system ensured consistent powder quality for calcium carbonate production, reducing product variability by 15%. These examples highlight the system's reliability and adaptability, making it a preferred choice for industries requiring efficient and safe material handling solutions.