

Principle and Working Scene Characteristics of Air-Driven Conveying Systems for Methylcellulose Mate
Shandong HeadPowder Engineering Co., Ltd. (headpowder), a professional enterprise based in Shandong, China, specializes in the design and manufacturing of air-driven conveying systems tailored for transporting methylcellulose materials. Methylcellulose, a widely used non-ionic cellulose ether, serves as a key additive in pharmaceuticals, food products, and industrial coatings due to its excellent film-forming and thickening properties. The air-driven conveying system is a critical infrastructure in the supply chain for these materials, ensuring efficient and reliable transport from storage to processing units.
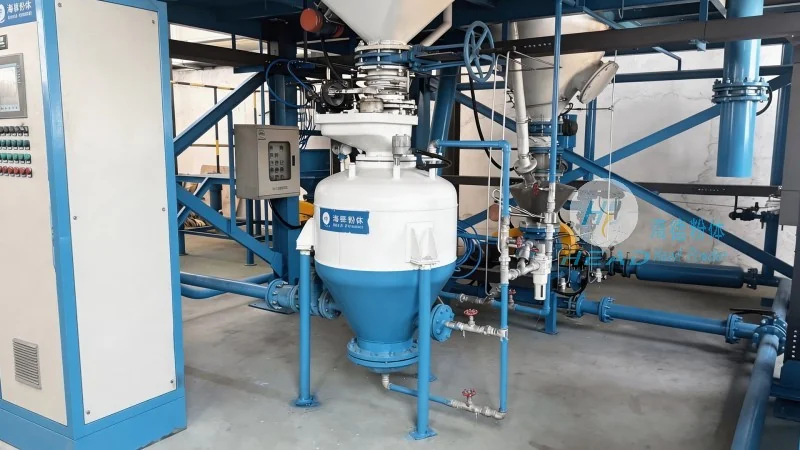
Core Principle of Air-Driven Conveying Systems
The fundamental principle of air-driven conveying systems is pneumatic transport, which utilizes compressed air to move bulk materials through a closed pipeline network. For methylcellulose, which is typically a fine powder or granular substance, the system operates by creating a pressure differential between the conveying line and the ambient environment. Air is introduced into the material stream, generating a flow that lifts and propels the material through the pipeline. The key to efficient operation lies in balancing air velocity and pressure to maintain a stable, homogeneous flow without causing material degradation, agglomeration, or excessive wear on the system components.
System Components and Operational Workflow
A typical air-driven conveying system for methylcellulose consists of several integrated components: a material feeder, conveying pipeline, air source unit, control valves, and a receiving hopper. The material feeder, often a rotary valve or a screw feeder, introduces the methylcellulose into the pipeline at a controlled rate. The air source unit, equipped with a compressor and filtration system, supplies clean, dry air to the conveying line. Control valves, such as pressure regulators and flow meters, adjust the air pressure and volume to optimize material transport. The receiving hopper collects the conveyed material, which can then be transferred to the next processing stage.
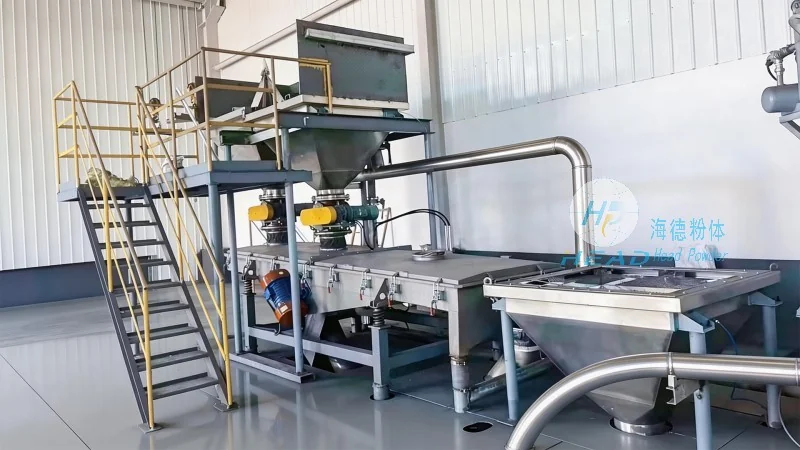
Working Scene Characteristics: Tailored for Methylcellulose Properties
The working scene characteristics of these systems are specifically designed to address the unique properties of methylcellulose. Methylcellulose is hygroscopic, meaning it absorbs moisture from the air, and it can vary in particle size, affecting its flowability. The air-driven system's design mitigates these challenges by employing low air velocities and precise pressure control to prevent material clumping or caking. In industrial settings, the system is often integrated into continuous production lines, ensuring seamless material transfer with minimal downtime. The systems are also adaptable to different production scales, from small-scale laboratory applications to large-scale manufacturing facilities, making them versatile for various operational needs.
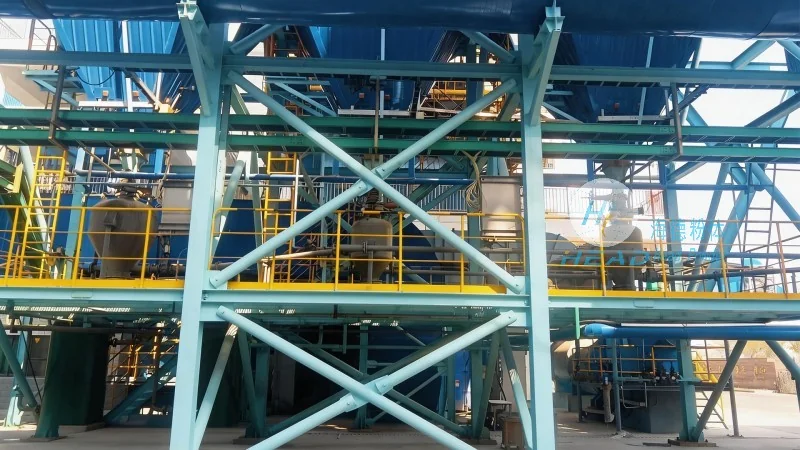
Advantages in Industrial Applications
Compared to traditional mechanical conveying methods like belt or screw conveyors, air-driven systems offer distinct advantages when handling methylcellulose. They minimize material degradation by reducing friction and impact, preserving the material's purity and functional properties. The closed pipeline design also reduces exposure to contaminants, which is critical in pharmaceutical and food industries. Additionally, the systems are easy to clean and maintain, adhering to stringent hygiene standards. Their flexibility allows for quick reconfiguration to accommodate changes in production volume or material types, enhancing overall operational efficiency.
Conclusion: Efficient and Reliable Material Transport
For industries relying on methylcellulose, the air-driven conveying system from Shandong HeadPowder Engineering Co., Ltd. provides a reliable and efficient solution for material transport. By leveraging pneumatic technology and tailored design, the system ensures consistent, high-quality transport of methylcellulose while meeting the demands of modern industrial production. With its headquarters in Shandong, China, headpowder continues to innovate in air-driven conveying solutions, supporting the needs of clients across various sectors.