

Principle and Working Scene Characteristics of Quartz Stone Material Pneumatic Conveying Equipment
Quartz stone, a widely used material in various industries such as construction, manufacturing, and decoration, often requires efficient and reliable transportation methods to move it from one location to another. Pneumatic conveying equipment offers a solution that addresses the challenges associated with handling quartz stone, including dust control, material loss prevention, and operational efficiency. This article explores the fundamental principles behind quartz stone pneumatic conveying systems and highlights the key working scene characteristics that make them suitable for different industrial applications.
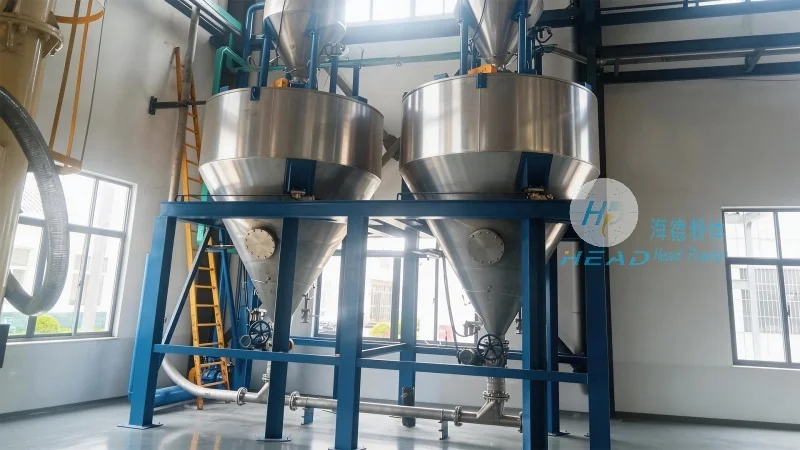
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of material handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and producing advanced pneumatic conveying solutions tailored to the needs of various industries. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses seeking efficient and reliable material transport systems. HeadPowder's expertise lies in understanding the unique requirements of different materials, including quartz stone, and developing customized solutions that meet the highest standards of performance and durability.
Principle of Quartz Stone Pneumatic Conveying
The core principle of quartz stone pneumatic conveying involves using compressed air to transport the material through a pipeline system. The process typically starts with the quartz stone being fed into a hopper or feeder, where it is then introduced into the conveying line. As compressed air is introduced into the pipeline, it creates a flow that lifts and propels the quartz stone particles through the system. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing material degradation. The pneumatic conveying system operates by creating a pressure differential between the inlet and outlet of the pipeline, ensuring a continuous and controlled flow of quartz stone.
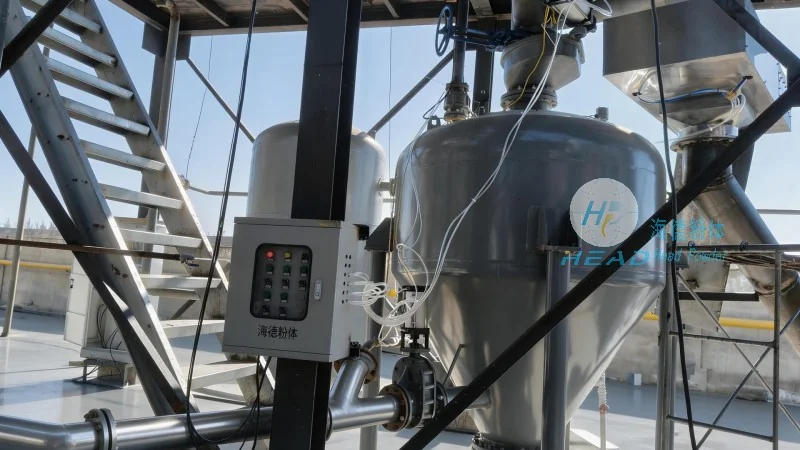
Working Scene Characteristics of Quartz Stone Pneumatic Conveying Equipment
The working scene characteristics of quartz stone pneumatic conveying equipment are crucial in determining its suitability for specific industrial applications. These characteristics include the material's particle size, density, and moisture content, as well as the required conveying distance and throughput. For quartz stone, which often consists of fine to medium-sized particles, the pneumatic conveying system must be designed to handle these characteristics effectively. The equipment must also be capable of maintaining a consistent flow rate and pressure to ensure reliable operation. Additionally, the system should incorporate features such as dust collection and filtration to comply with environmental regulations and maintain a clean working environment.
Key Features and Advantages of Quartz Stone Pneumatic Conveying Systems
Quartz stone pneumatic conveying systems offer several advantages over traditional material handling methods. One of the primary benefits is the ability to transport the material in a closed system, which reduces dust emissions and minimizes the risk of material contamination. This is particularly important for quartz stone, which can be abrasive and may cause wear on mechanical components if not handled properly. The closed system also helps in maintaining the purity of the material, which is essential for applications where the quality of quartz stone is critical, such as in the production of countertops or decorative tiles. Another advantage is the flexibility of the system, which allows for easy integration with existing production lines and the ability to adjust the conveying rate as per the production requirements.
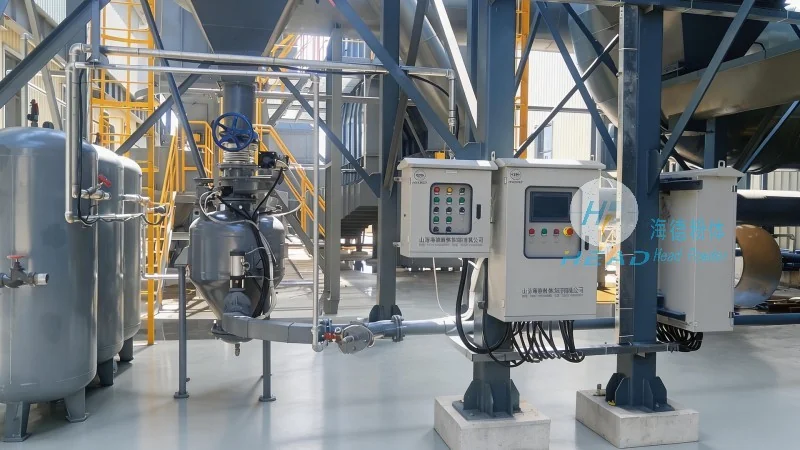
Application Scenarios and Operational Efficiency
Quartz stone pneumatic conveying equipment is widely used in various industrial settings, including quartz processing plants, construction material manufacturing facilities, and decorative stone production sites. In these applications, the equipment is designed to handle large volumes of quartz stone efficiently, ensuring that the production process remains uninterrupted. The operational efficiency of the system is enhanced by features such as automatic feeding and control systems, which allow for precise control over the material flow. Additionally, the system's ability to handle different particle sizes and moisture levels makes it versatile and suitable for a wide range of applications. The equipment's durability and low maintenance requirements further contribute to its operational efficiency, reducing downtime and increasing overall productivity.
Conclusion and Company Commitment
In conclusion, quartz stone pneumatic conveying equipment is a highly effective solution for transporting quartz stone in various industrial applications. The principles behind this technology, combined with the working scene characteristics and key features of the system, make it an ideal choice for businesses seeking reliable and efficient material handling solutions. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and improve its pneumatic conveying systems to meet the evolving needs of the industry, ensuring that customers receive high-quality equipment that delivers optimal performance and durability. With its commitment to quality and customer satisfaction, HeadPowder remains a leading provider of material handling solutions for quartz stone and other similar materials.