

Introduction to Red Bean Pneumatic Conveying System: Structure and Working Principle Explanation
Red Bean Pneumatic Conveying Systems are advanced industrial equipment designed for efficient material handling and transportation. This article provides a comprehensive overview of the system's structure and operational principles, highlighting key components and their functions. The system is engineered to deliver reliable performance in various industrial applications, ensuring smooth and continuous material flow.
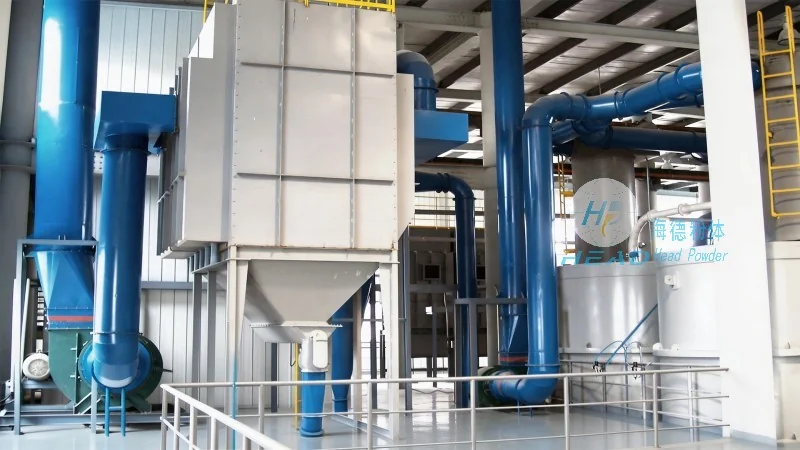
Overview of Red Bean Pneumatic Conveying System
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of high-quality pneumatic conveying solutions. The Red Bean Pneumatic Conveying System is a prime example of their expertise, combining innovative technology with robust construction to meet diverse industrial needs. This system is particularly suitable for transporting bulk materials such as powders, granules, and small particles, offering a cost-effective alternative to traditional mechanical conveying methods.
Key Structural Components and Their Functions
The Red Bean Pneumatic Conveying System comprises several critical components that work in tandem to ensure efficient operation. The main components include the hopper, air compressor, conveying line, and control system. The hopper serves as the material storage and feeding unit, where bulk materials are loaded and prepared for transport. The air compressor generates the necessary air pressure to create a flow of air within the conveying line, which then propels the material particles through the system. The conveying line, typically made of stainless steel or other corrosion-resistant materials, ensures the safe and efficient transport of materials over long distances. The control system monitors and regulates the air pressure, flow rate, and material feed, maintaining optimal performance and preventing system failures.
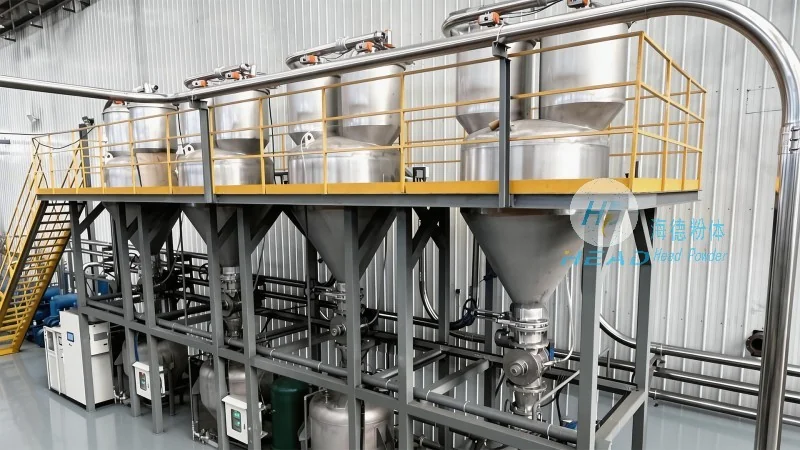
Working Principle of the Pneumatic Conveying Process
The operation of the Red Bean Pneumatic Conveying System follows a straightforward yet effective principle. When the system is activated, the air compressor starts, and compressed air is introduced into the conveying line. Simultaneously, the material from the hopper is fed into the line. The high-pressure air creates a flow that carries the material particles along the line, transporting them to the destination point. The system utilizes the principle of fluidization, where the air flow suspends the material particles, allowing them to move smoothly without the need for mechanical contact. This process minimizes material degradation and ensures consistent quality of the transported product.
Advantages of Red Bean Pneumatic Conveying System
Compared to traditional mechanical conveying systems, the Red Bean Pneumatic Conveying System offers several advantages. Firstly, it eliminates the need for mechanical components such as belts, chains, or screws, reducing maintenance costs and increasing system reliability. Secondly, the system is highly flexible, allowing for easy adjustment of conveying distances and material types. Thirdly, it provides a hygienic and dust-free environment, which is crucial for industries handling food, pharmaceuticals, or other sensitive materials. Additionally, the system is energy-efficient, as it uses compressed air to transport materials, reducing overall operational costs.
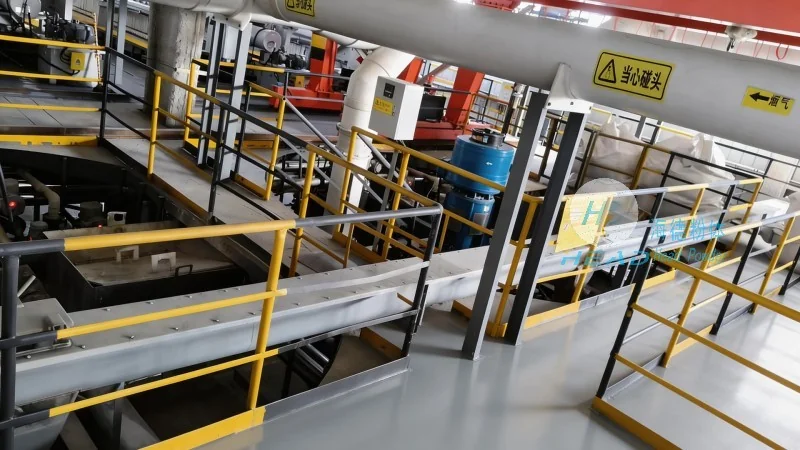
Application Scenarios and Industrial Use Cases
The Red Bean Pneumatic Conveying System is widely used in various industries, including food processing, pharmaceutical manufacturing, chemical production, and mining. In the food industry, it is used to transport ingredients such as flour, sugar, and spices, ensuring hygienic and efficient handling. In pharmaceuticals, the system is employed to convey active pharmaceutical ingredients (APIs) and excipients, maintaining strict quality control and preventing contamination. In chemical plants, it handles various powders and granules, such as catalysts and reagents, with precision and reliability. The system's adaptability makes it suitable for both small-scale and large-scale industrial applications, providing a versatile solution for material handling needs.
Quality Assurance and Technical Specifications
HeadPowder ensures the Red Bean Pneumatic Conveying System meets the highest quality standards through rigorous testing and quality control processes. The system is manufactured using premium materials and advanced manufacturing techniques, ensuring durability and long service life. Technical specifications include a conveying capacity ranging from 0.5 to 50 tons per hour, depending on the material type and system configuration. The system operates at air pressures from 0.5 to 1.0 MPa, with adjustable flow rates to accommodate different material characteristics. The control system is equipped with safety features such as pressure relief valves and emergency stop buttons, ensuring safe operation and preventing accidents.