

[Ambient Fertilizer Pneumatic Conveying Design and Equipment Selection]
For industrial applications involving the transport of ambient fertilizer, the design and selection of a pneumatic conveying system are critical to ensure efficiency, reliability, and cost-effectiveness. Proper design calculation and equipment selection can significantly impact the overall performance and longevity of the conveying system. This article provides an overview of the key considerations in designing and selecting equipment for ambient fertilizer pneumatic conveying, with a focus on the expertise offered by Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder.
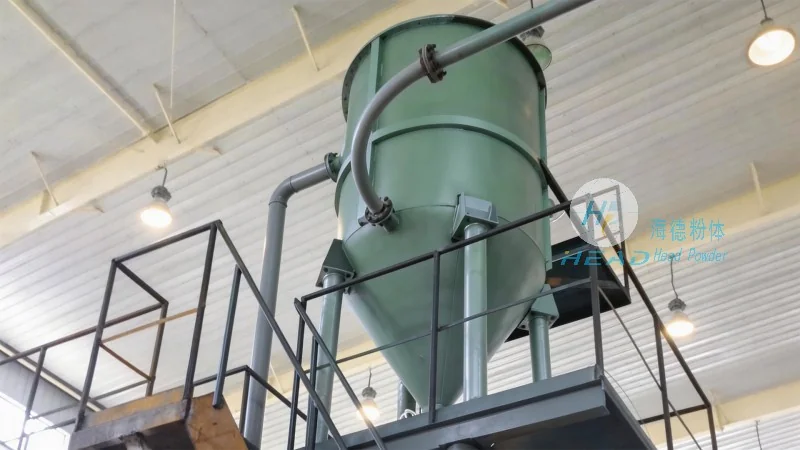
Understanding Ambient Fertilizer Pneumatic Conveying
Ambient fertilizer, typically in granular or powder form, requires specialized handling due to its physical properties such as particle size, density, and flowability. Pneumatic conveying systems use air or other gases to transport these materials, offering advantages over traditional mechanical methods like belt conveyors or screw conveyors. These systems are particularly suitable for applications where dust control, minimal product degradation, and flexibility in layout are essential.
Key Design Calculations for Pneumatic Conveying Systems
The success of a pneumatic conveying system for ambient fertilizer hinges on accurate design calculations. Several critical parameters must be determined to ensure optimal operation. First, the required conveying capacity, measured in tons per hour or cubic meters per hour, is determined based on the production rate and material flow requirements. Next, the air velocity and pressure drop along the pipeline must be calculated to maintain the material in suspension and prevent blockages. This involves analyzing the gas-solid flow regime, which can be classified as dilute phase or dense phase, depending on the air-to-solid ratio and system design.
Another crucial calculation is the selection of the appropriate gas source, typically a centrifugal or axial flow fan, which must provide sufficient pressure and flow rate to overcome system resistance. The fan's power consumption and efficiency are also critical factors in the overall system design. Additionally, the pipeline layout, including the number of bends, vertical rises, and horizontal runs, affects the pressure drop and must be optimized to minimize energy consumption while ensuring smooth material transport.
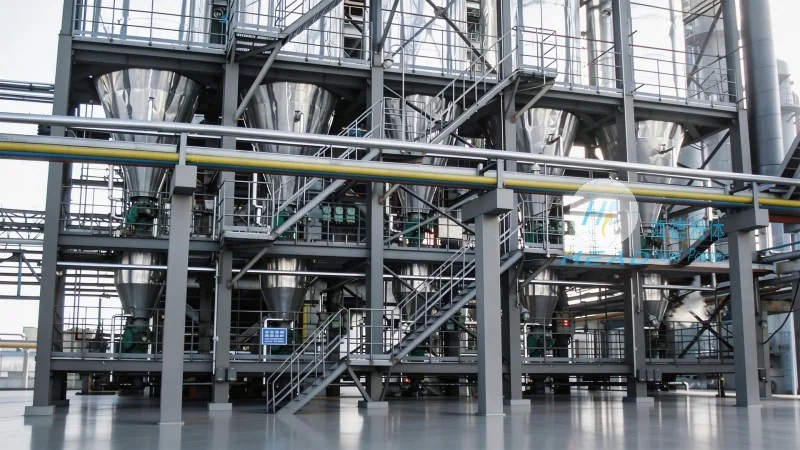
Equipment Selection for Ambient Fertilizer Conveying
Choosing the right equipment for ambient fertilizer pneumatic conveying involves evaluating various components, each with specific functions. The primary equipment includes the material feed system, such as a hopper or rotary valve, which controls the material flow into the conveying line. The conveying line itself, made of materials like stainless steel or PVC, must be selected based on the fertilizer's chemical compatibility and the need for corrosion resistance.
At the heart of the system is the air mover, which can be a positive displacement blower or a high-pressure fan, depending on the system's pressure and flow requirements. The selection of the air mover is critical as it directly impacts energy efficiency and operational costs. The system also includes separation and collection equipment, such as cyclones or bag filters, to remove the fertilizer from the air stream and prevent product loss or environmental contamination.
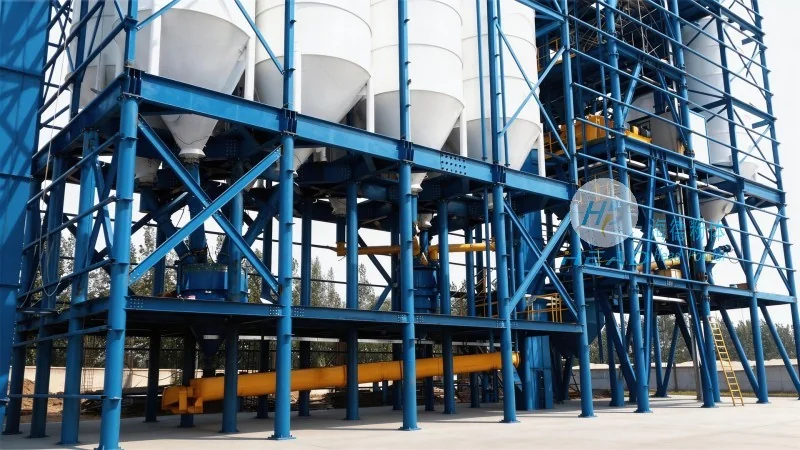
Customized Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of fertilizer processing facilities. With years of experience in the industry, headpowder's team of engineers employs advanced computational tools and methodologies to perform precise design calculations, ensuring that each system meets the specific requirements of the client.
headpowder's approach to equipment selection is comprehensive, considering not only the technical specifications but also the operational environment, maintenance requirements, and long-term cost implications. The company offers a range of standard and custom-designed components, including conveyors, fans, and separation units, all built to withstand the harsh conditions of fertilizer handling and provide reliable performance over extended periods.
Conclusion
Designing and selecting a pneumatic conveying system for ambient fertilizer requires a thorough understanding of material properties, system dynamics, and equipment capabilities. By adhering to proper design calculations and choosing the right equipment, facilities can achieve efficient, safe, and cost-effective material transport. Shandong HeadPowder Engineering Co., Ltd. (headpowder) stands as a trusted partner in this process, providing expert guidance and high-quality solutions to meet the diverse needs of the fertilizer industry.