

What is a Quartz Sand Material Pneumatic Conveying System? What are its Design Principles?
Quartz sand, a widely used industrial material, often requires efficient and reliable transportation methods for processing and distribution. The quartz sand material pneumatic conveying system is a specialized solution designed to handle this material with precision and effectiveness. This system utilizes air as the primary medium to transport quartz sand particles from one location to another, offering advantages such as reduced equipment wear, minimal contamination, and the ability to handle fine or abrasive materials like quartz sand.
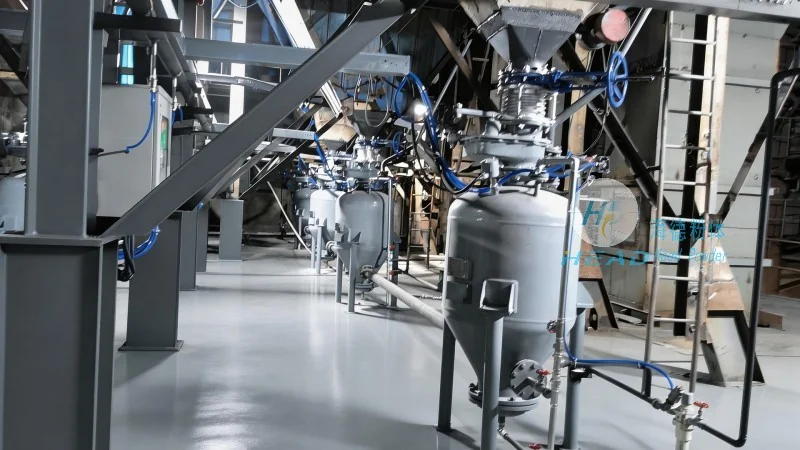
Understanding the Quartz Sand Material Pneumatic Conveying System
At its core, a quartz sand material pneumatic conveying system is a closed-loop or open-loop system that uses compressed air to move quartz sand particles through a pipeline network. The system typically consists of a material hopper, an air compressor, a conveying line, and a receiver or discharge point. The material hopper holds the quartz sand, while the air compressor generates the necessary pressure to propel the particles through the conveying line. The conveying line can be made of various materials, including stainless steel or plastic, depending on the application and the characteristics of the quartz sand.
Key Design Principles of the System
The design of a quartz sand material pneumatic conveying system is governed by several critical principles to ensure optimal performance and efficiency. One of the primary principles is the selection of the appropriate air velocity. The air velocity must be high enough to keep the quartz sand particles in suspension but low enough to prevent excessive pressure drop and energy consumption. This balance is crucial for maintaining the system's efficiency and minimizing operational costs. Another key principle is the proper sizing of the conveying line and components. The diameter of the conveying line is determined by the particle size, flow rate, and air velocity, ensuring that the system can handle the required volume of quartz sand without causing blockages or excessive pressure losses.
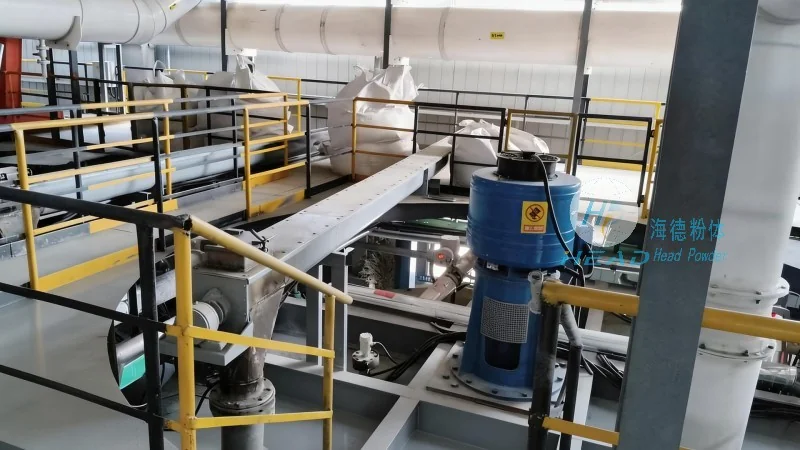
Components and Their Functions in the System
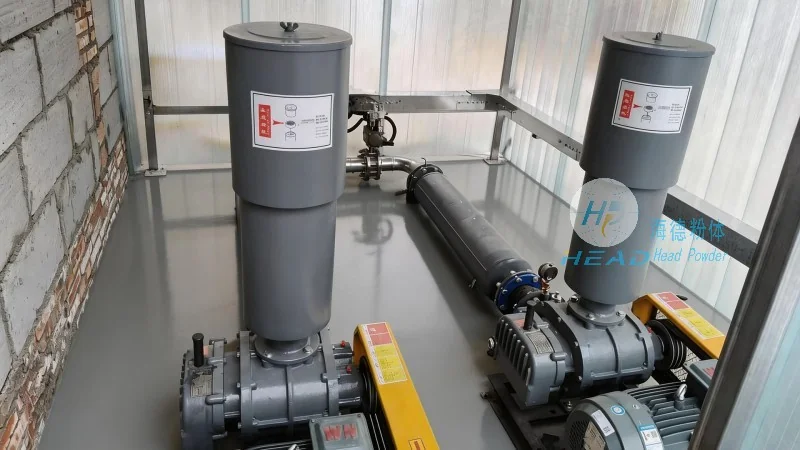
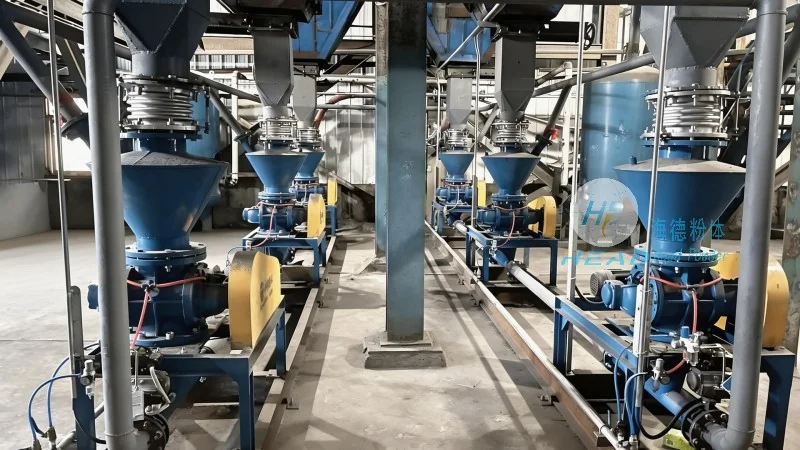
Each component of the quartz sand material pneumatic conveying system plays a vital role in the overall operation. The material hopper is designed to store the quartz sand and provide a consistent feed to the system. It often includes a feeder, such as a rotary valve or a screw feeder, to control the flow rate of the material. The air compressor is responsible for generating the compressed air that propels the quartz sand particles. The choice of compressor type, such as a positive displacement or centrifugal compressor, depends on the system's requirements, including the pressure and flow rate needed. The conveying line connects the hopper to the receiver and is equipped with bends, elbows, and other fittings to direct the flow of the material. The receiver, or discharge point, collects the quartz sand and may include a dust collection system to prevent air leakage and maintain a clean environment.
Advantages of Using a Quartz Sand Material Pneumatic Conveying System
Implementing a quartz sand material pneumatic conveying system offers several advantages over traditional mechanical conveying methods. One of the main benefits is the reduction in equipment wear and tear. Since the quartz sand particles are transported by air rather than mechanical components, the system experiences less friction and abrasion, leading to longer equipment life and lower maintenance costs. Another advantage is the minimal contamination of the material. The closed-loop design of the system prevents the quartz sand from coming into contact with external elements, ensuring that the material remains clean and free from contaminants. Additionally, the system can handle fine or abrasive quartz sand particles without causing blockages or damage to the equipment, making it suitable for a wide range of applications.
Applications of Quartz Sand Material Pneumatic Conveying Systems
The quartz sand material pneumatic conveying system is widely used in various industries that require the transportation of quartz sand. These applications include the glass manufacturing industry, where quartz sand is a key raw material for glass production. The system efficiently transports the quartz sand from storage to the glass melting furnace. In the construction industry, the system is used to move quartz sand for concrete production and other building materials. Additionally, the system is employed in the mining and processing of quartz sand, where it is used to transport the material from the mine to processing facilities. The versatility of the system makes it suitable for various industrial applications, providing a reliable and efficient solution for quartz sand transportation.
Customization and Scalability of the System
Quartz sand material pneumatic conveying systems can be customized to meet the specific needs of different industries and applications. The system can be scaled up or down to handle varying volumes of quartz sand, from small-scale operations to large industrial plants. The components of the system, such as the conveying line diameter, air compressor capacity, and material hopper size, can be adjusted to accommodate different particle sizes and flow rates. This flexibility allows the system to be adapted to various production requirements, ensuring optimal performance and efficiency. Additionally, the system can be integrated with other processing equipment, such as crushers or classifiers, to form a complete quartz sand processing line.