

What is a Calcium Carbonate Stone Powder Pneumatic Conveying System? And What Are Its Design Princip
A calcium carbonate stone powder pneumatic conveying system is a specialized industrial solution designed to transport fine powder materials, such as calcium carbonate, through a pipeline using air or gas as the conveying medium. This technology is widely used in industries like chemical manufacturing, food processing, and pharmaceuticals, where the efficient and dust-free transfer of powders is critical for maintaining product quality and operational safety. The system typically consists of several key components, including a hopper for material storage, a blower or compressor to generate the conveying air, a pipeline network to transport the material, and a receiver or discharge unit to collect the material at the destination. The primary advantage of this system is its ability to move powders over long distances without the need for mechanical components like belts or buckets, reducing maintenance costs and minimizing product contamination.
Design Principles of Pneumatic Conveying Systems for Calcium Carbonate
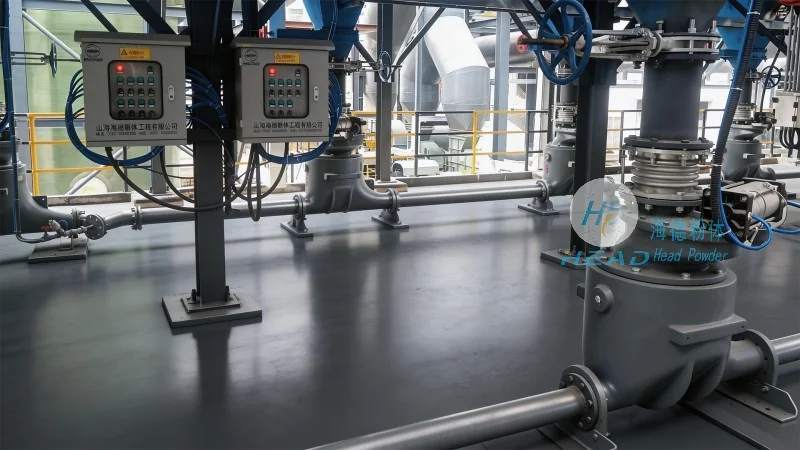
The design of a calcium carbonate stone powder pneumatic conveying system is based on several fundamental principles to ensure efficient and reliable operation. First, the system must be designed to handle the specific properties of calcium carbonate, including its particle size, density, and flow characteristics. The particle size distribution is a critical factor, as finer particles require higher air velocities to maintain suspension and prevent clogging in the pipeline. Design engineers must calculate the appropriate air velocity and pressure to achieve stable conveying, typically using the "triple-s" or "venturi" methods for high-capacity systems. The system's layout, including the number and length of pipelines, the placement of bends and elbows, and the size of the hopper and receiver, all impact the overall efficiency and energy consumption. Additionally, the system must be equipped with proper filtration and dust collection to comply with environmental regulations and maintain a clean working environment. The design process also considers factors like material handling capacity, required conveying distance, and the need for flexibility in the system's operation, such as the ability to switch between different material types or adjust conveying rates.
Key Components and Their Roles in the System
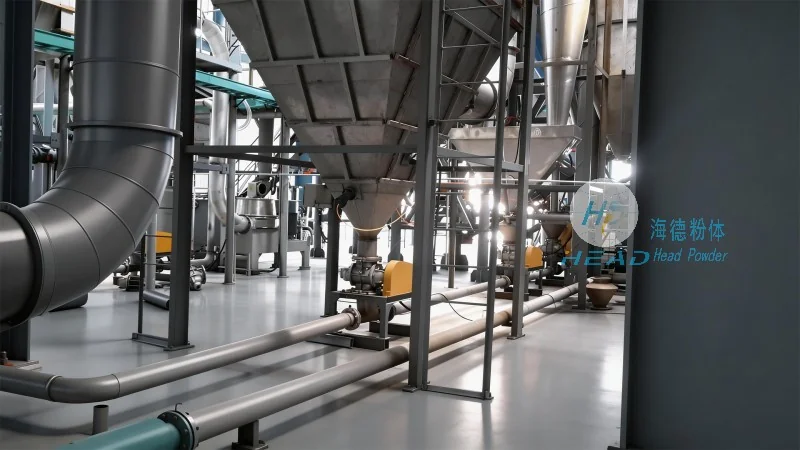
Each component of a calcium carbonate stone powder pneumatic conveying system plays a crucial role in the overall performance and reliability of the system. The material hopper is the first component where the calcium carbonate powder is stored before being fed into the system. It is typically designed with a conical or hopper-shaped bottom to facilitate smooth material flow and prevent agglomeration. The hopper is equipped with a feeder, such as a rotary valve or a screw feeder, which controls the rate at which the material is discharged into the pipeline. The feeder must be designed to handle the specific characteristics of calcium carbonate, ensuring consistent material flow without blocking or clogging. The blower or compressor is the heart of the system, responsible for generating the air or gas that propels the powder through the pipeline. The choice of blower type—such as a centrifugal or positive displacement blower—depends on the system's capacity and the required air pressure. The pipeline network connects the hopper to the receiver and includes various components like bends, elbows, and straight sections. The design of these components is critical to minimize pressure drop and maintain the air-powder mixture's stability. The receiver or discharge unit is where the calcium carbonate powder is collected at the end of the conveying process. It is typically a hopper or tank with a discharge valve, allowing the material to be transferred to the next stage of the production process. The receiver may also include a filter or cyclone to separate any fine particles from the air before it is released into the environment.
Advantages and Applications of Calcium Carbonate Pneumatic Conveying
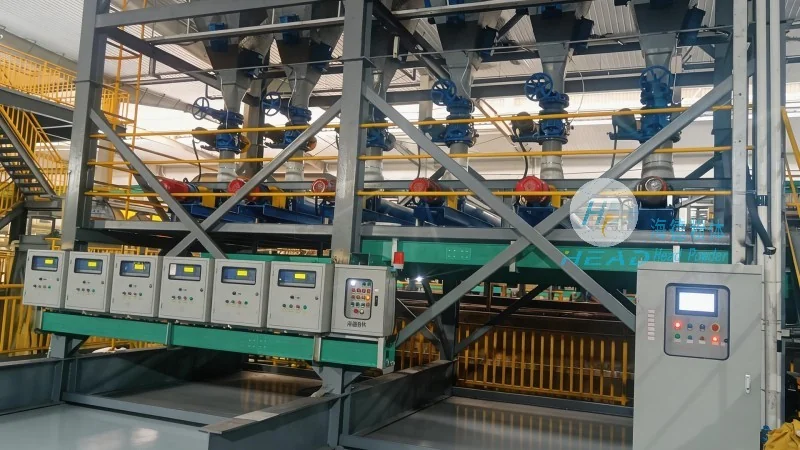
The use of a pneumatic conveying system for calcium carbonate offers several advantages over traditional mechanical conveying methods. One of the main benefits is the ability to transport powders over long distances without the need for intermediate transfer points, which reduces the risk of material loss and contamination. The system also provides a dust-free environment, which is essential for maintaining product quality and ensuring workplace safety. Additionally, pneumatic conveying systems are more energy-efficient than mechanical systems, as they use air as the conveying medium rather than mechanical components that require constant power. This results in lower operational costs and reduced maintenance requirements. The applications of calcium carbonate pneumatic conveying systems are diverse and include the production of coatings, plastics, and paper, as well as in the food and pharmaceutical industries where the purity of the material is paramount. The system's flexibility allows it to be adapted to different production requirements, such as varying material flow rates or changing production schedules, making it a versatile solution for many industrial processes.
About Shandong HeadPowder Engineering Co., Ltd.
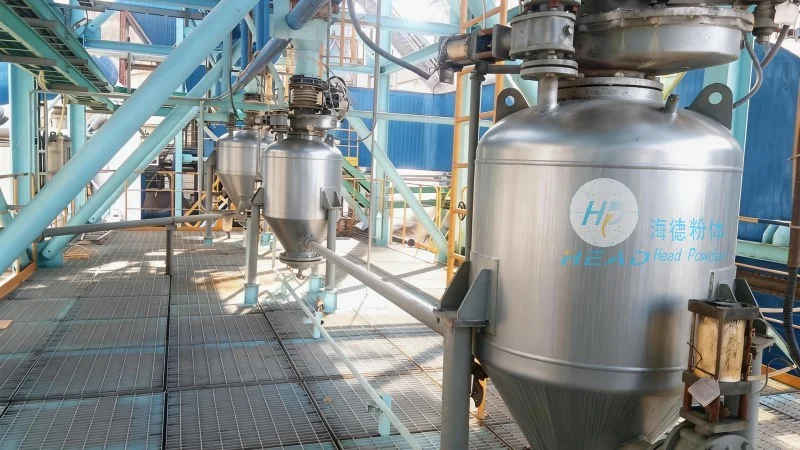
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including calcium carbonate stone powder pneumatic conveying systems. The company is headquartered in Shandong, China, and has a strong reputation for providing high-quality, reliable, and efficient solutions for material handling in various industries. HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients, ensuring that each system meets the unique requirements of the application. The company's team of experienced engineers and technicians work closely with clients to understand their production processes and develop solutions that optimize material flow, reduce costs, and improve overall operational efficiency. With a focus on innovation and quality, HeadPowder has become a trusted partner for many companies in the chemical, food, and pharmaceutical industries, providing them with the tools they need to achieve their production goals efficiently and safely.