

What is a Sorghum Residue Material Pneumatic Conveying System? And What Are Its Design Principles?
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier specializing in advanced material handling solutions. With a focus on innovation and precision engineering, the company has established itself as a trusted partner in the industry, delivering high-quality equipment for various industrial applications. HeadPowder's commitment to excellence is reflected in its state-of-the-art products, including the sorghum residue material pneumatic conveying system, which addresses the specific needs of the food and beverage sector, particularly in the production of sorghum-based alcoholic beverages.
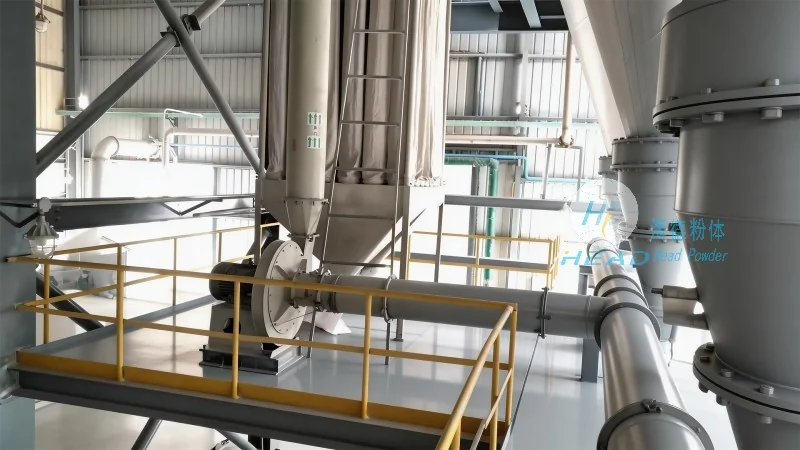
Understanding the Sorghum Residue Material Pneumatic Conveying System
The sorghum residue material pneumatic conveying system is a specialized equipment designed to efficiently transport sorghum residue, a byproduct of sorghum processing, from one location to another. This system is particularly relevant in the context of distilleries and breweries where sorghum is used as a primary ingredient for producing sorghum liquor. The system ensures that the residue, which may contain moisture and other impurities, is handled safely and effectively, minimizing material loss and optimizing the overall production process.
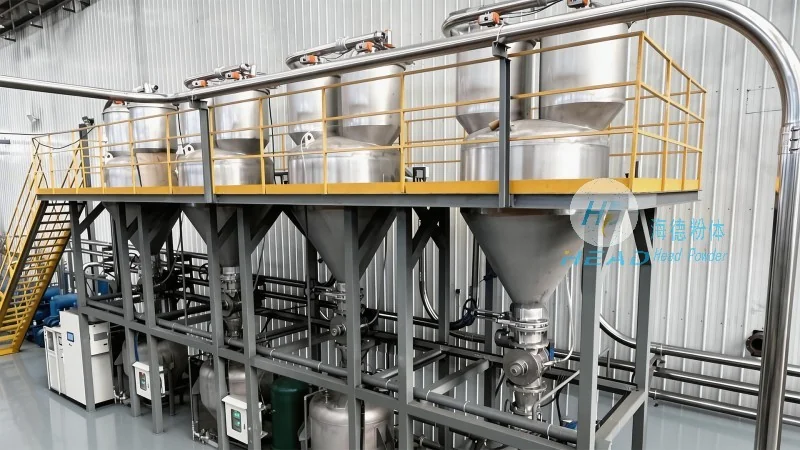
Design Principles of the Pneumatic Conveying System
The design of the sorghum residue material pneumatic conveying system is based on the fundamental principles of pneumatic transport, which involves the use of air or gas to move bulk materials through a pipeline. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a compressor to generate the necessary air pressure, and a pipeline network to transport the material. The design also incorporates features such as air filtration and moisture control to ensure the material remains in optimal condition during transport. The system is engineered to handle the unique characteristics of sorghum residue, such as its particle size, density, and moisture content, ensuring reliable and consistent performance.
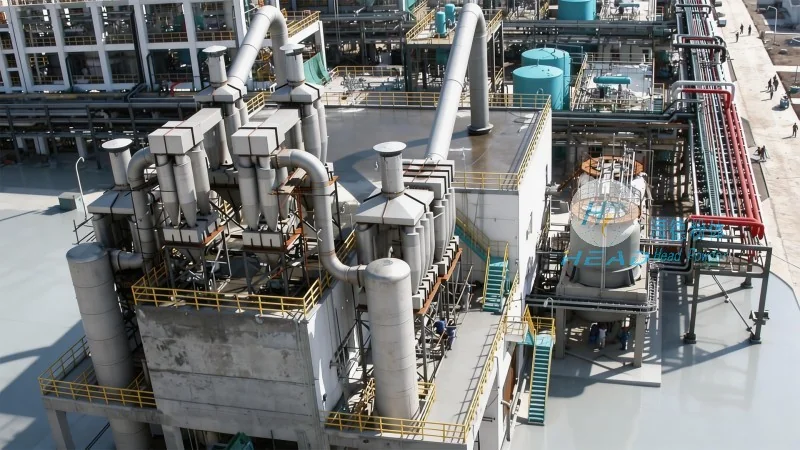
Advantages of the Pneumatic Conveying System
One of the primary advantages of the sorghum residue material pneumatic conveying system is its ability to handle materials that are difficult to transport using traditional methods, such as screw conveyors or belt conveyors. The system eliminates the need for multiple transfer points and reduces the risk of material contamination, as the entire process is enclosed and controlled. Additionally, the system is highly flexible, allowing for easy integration with existing production lines and the ability to adjust the flow rate according to production demands. The use of air as the conveying medium also minimizes the risk of material degradation and reduces the need for additional cleaning and maintenance.
Applications and Use Cases
The sorghum residue material pneumatic conveying system is widely used in the food and beverage industry, particularly in the production of sorghum-based alcoholic beverages. It is also applicable in other industries where bulk materials need to be transported efficiently, such as in the agricultural and chemical sectors. The system is particularly beneficial for facilities that require high throughput and minimal downtime, as it can handle large volumes of material with minimal maintenance. The system's ability to transport materials over long distances without the need for intermediate storage makes it an ideal solution for large-scale production operations.
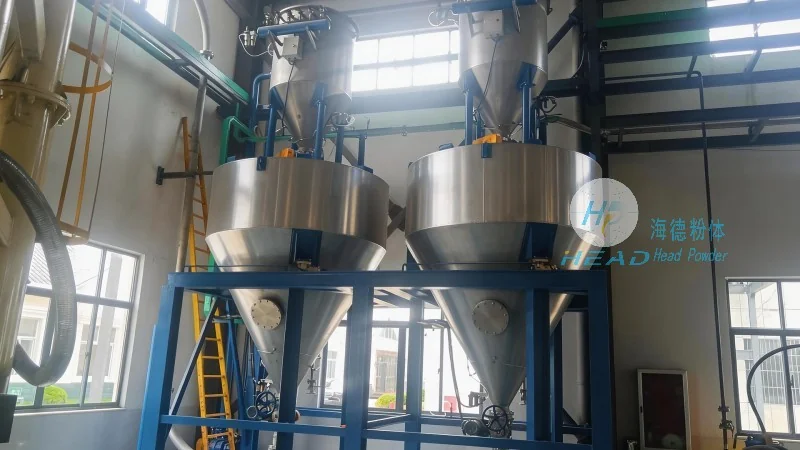
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides a comprehensive solution for the efficient handling of sorghum residue through its advanced pneumatic conveying system. The system is designed with precision engineering and incorporates the latest technology to ensure optimal performance and reliability. By leveraging the principles of pneumatic transport, the system addresses the unique challenges of sorghum residue handling, offering a cost-effective and sustainable solution for industrial applications. HeadPowder's commitment to quality and customer satisfaction ensures that its products meet the highest standards, making it a preferred choice for businesses seeking reliable material handling solutions.