

Working Principle and Features of Automatic Quantitative Ingredient Pneumatic Conveying
Automatic quantitative pneumatic conveying systems represent a sophisticated industrial technology used for the efficient transport of bulk materials with precise measurement and control. These systems are widely employed across diverse sectors such as food processing, pharmaceuticals, and chemical manufacturing, where maintaining consistent material handling is essential for product quality and operational efficiency.
Working Principle of Automatic Quantitative Pneumatic Conveying
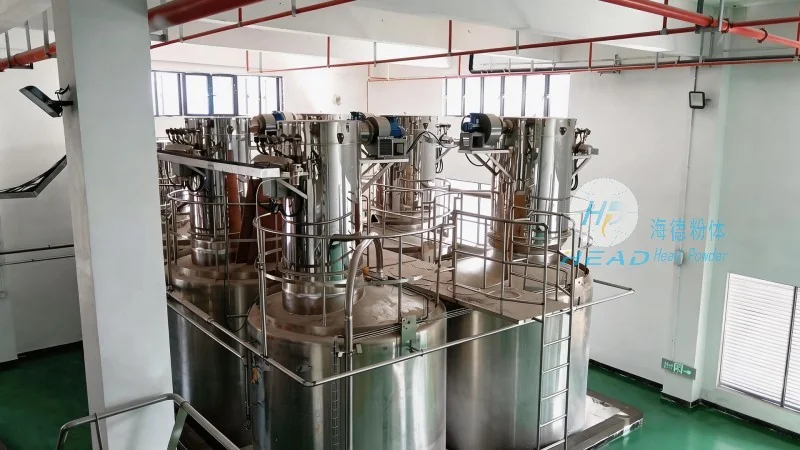
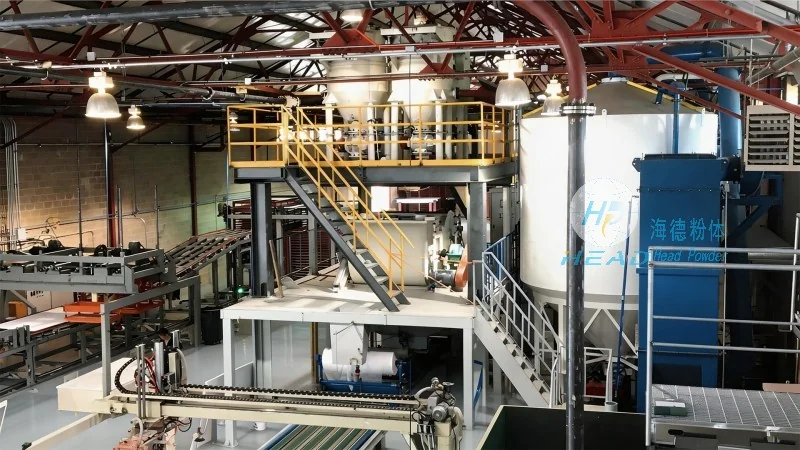
The fundamental operation of an automatic quantitative pneumatic conveying system revolves around the utilization of compressed air to move materials through a network of pipelines. The process typically initiates with a material storage hopper or bin, which feeds the bulk material into a feeder unit. The feeder, often equipped with a rotary valve or screw mechanism, regulates the flow rate of the material, ensuring a consistent and controlled quantity is released. This material then enters a conveying line where it is propelled by the air flow, traveling through the system to the discharge point. The system may incorporate additional components like cyclones, filters, and silos to separate and store the conveyed material, maintaining cleanliness and preventing contamination. The entire process is automated, allowing for real-time monitoring and adjustment to maintain optimal performance.
Key Features and Advantages of Automatic Quantitative Pneumatic Conveying
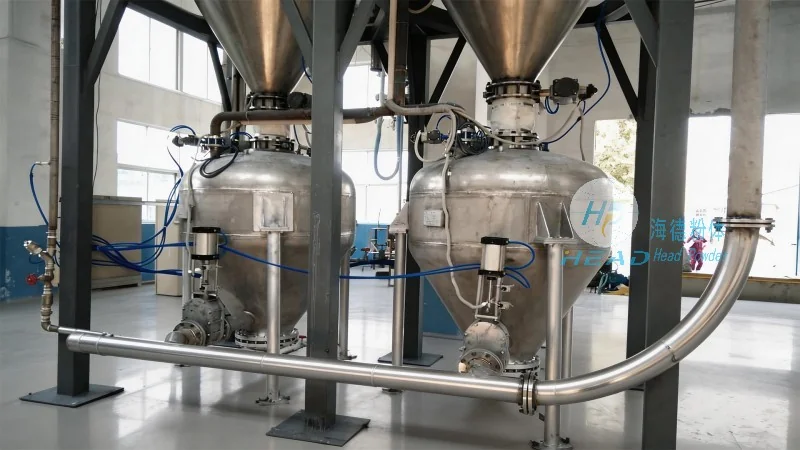
Automatic quantitative pneumatic conveying systems offer several notable features and advantages that enhance their applicability in modern industrial settings. One of the primary benefits is the high level of accuracy in material measurement, with some systems capable of delivering precise quantities within tight tolerances. This precision is critical for processes that require exact dosing, such as in pharmaceutical production or food packaging, where product consistency directly impacts safety and consumer satisfaction. Another key feature is the hygienic and enclosed design, which reduces the risk of contamination and dust exposure, making these systems suitable for industries where product purity is paramount. The flexible layout capabilities also allow for easy integration into existing production lines without extensive modifications, providing cost-effective solutions for upgrading or expanding operations. Furthermore, the use of compressed air as the conveying medium eliminates the need for mechanical components in the conveying path, minimizing wear and tear and reducing maintenance requirements. This results in lower operational costs and increased system reliability over time, contributing to long-term sustainability and efficiency.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a prominent manufacturer specializing in the design and production of advanced pneumatic conveying systems. The company has built a strong reputation for innovation and quality, serving as a trusted partner in the industry by providing customized solutions tailored to the specific needs of clients. HeadPowder's expertise lies in developing systems that combine precision, efficiency, and durability, ensuring optimal performance in demanding industrial environments. The company's facilities are located in Shandong, China, where it leverages local manufacturing capabilities to deliver high-quality products to global markets. With a commitment to customer satisfaction and technological advancement, HeadPowder continues to lead the way in pneumatic conveying technology, supporting industries worldwide in achieving their operational goals.