

Working Principle and Features of Aggregate Powder Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment tailored for the efficient handling of aggregate and powder materials. This equipment is essential for industries such as construction, mining, and chemical processing, where reliable material transport is critical to operational efficiency and safety.
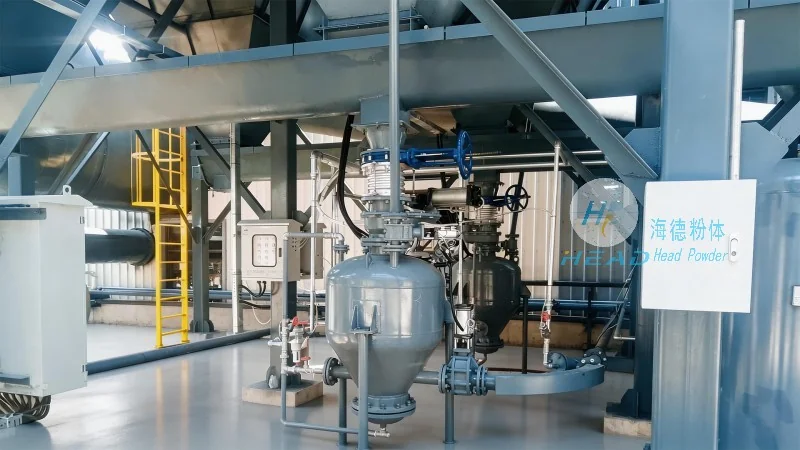
Working Principle of Aggregate Powder Pneumatic Conveying Equipment
The core of pneumatic conveying systems lies in the use of air as the primary medium to transport bulk materials. The process typically involves a series of components, including a hopper for material storage, a blower or compressor to generate airflow, and a pipeline network that guides the material from the source to the destination. As material is fed into the system, it is entrained by the high-velocity air stream, creating a slurry-like mixture that travels through the pipeline. The design of the system, including the type of airlock, cyclone separator, and filter, is crucial for maintaining material integrity and preventing system blockages. The working principle ensures that materials are moved without the need for mechanical components like belts or buckets, reducing maintenance requirements and operational costs.
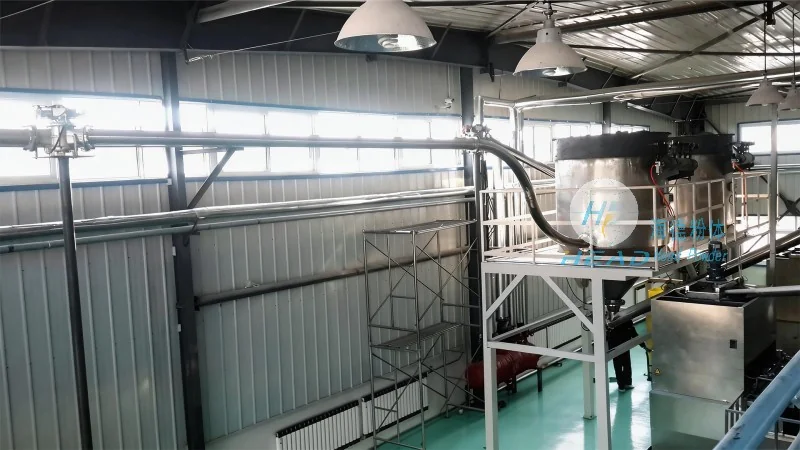
Key Features of Pneumatic Conveying Equipment
HeadPowder's pneumatic conveying systems are characterized by several key features that enhance performance and reliability. Firstly, the equipment is designed for high efficiency, with minimal material degradation during transport. This is achieved through optimized airflow velocities and pipeline diameters that prevent abrasion or breakage of the material particles. Secondly, the systems offer flexibility in application, as they can handle a wide range of materials, from fine powders to coarse aggregates, with adjustable settings to accommodate different material properties. Thirdly, the equipment is built for durability and longevity, using high-quality materials such as stainless steel and corrosion-resistant coatings to withstand harsh operating conditions. Additionally, the systems are equipped with advanced control mechanisms that allow for real-time monitoring and adjustment of airflow and material flow rates, ensuring consistent performance and reducing downtime. The integration of these features makes the equipment suitable for both small-scale and large-scale industrial applications, providing a cost-effective solution for material handling needs.
Advantages of Using Pneumatic Conveying Systems
Implementing pneumatic conveying systems for aggregate and powder materials offers numerous advantages over traditional mechanical methods. One of the most significant benefits is the reduction in labor costs, as the automated process minimizes the need for manual handling and reduces the risk of workplace injuries. Additionally, the systems enhance safety by eliminating the need for manual loading and unloading of materials, which can be hazardous. The equipment also contributes to improved product quality by preventing contamination and material loss during transport. Furthermore, the compact design of the systems allows for easy integration into existing industrial facilities, saving space and reducing installation costs. The long-term operational efficiency of pneumatic conveying systems, combined with lower maintenance requirements, results in substantial cost savings over the equipment's lifespan. These advantages make the technology a preferred choice for industries seeking to optimize their material handling processes.
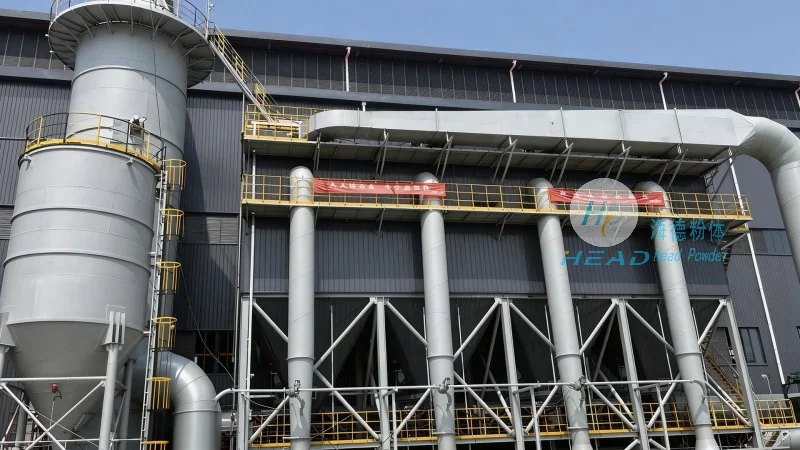
Application Examples and Industry Impact
The versatility of HeadPowder's pneumatic conveying equipment is demonstrated through its application in various industries. In the construction sector, the systems are used to transport sand, gravel, and cement from storage silos to mixing plants, ensuring a continuous and controlled supply of raw materials. In the mining industry, the equipment efficiently moves crushed ore and fine powders from processing plants to storage or shipping facilities, improving the overall productivity of mining operations. The chemical industry also benefits from the use of pneumatic conveying systems, as they handle sensitive powders and chemicals without the risk of cross-contamination or material degradation. The consistent performance of these systems has a positive impact on production efficiency, as they enable smooth material flow and reduce bottlenecks in the production process. By addressing the challenges of material handling, the equipment supports the growth and sustainability of industries that rely on bulk material transport.