

Working Principle and Features of Brown Sugar Powder Pneumatic Conveying System
For industrial operations involving the handling of brown sugar powder, efficient and reliable material transport is crucial. This article explores the working principle and key features of a brown sugar powder pneumatic conveying system, presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field. The system is designed to address the unique challenges associated with transporting fine powders like brown sugar, ensuring high performance and operational efficiency.
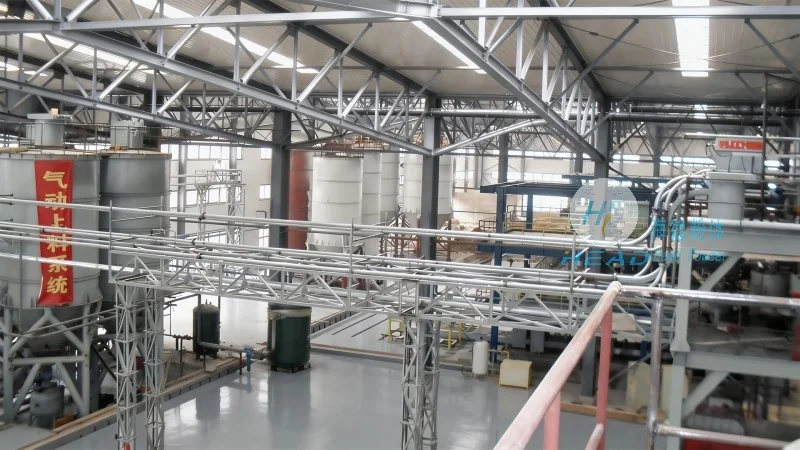
Overview of the Brown Sugar Powder Pneumatic Conveying System
The brown sugar powder pneumatic conveying system is a specialized equipment solution tailored for the transport of brown sugar powder in industrial settings. Developed by Shandong HeadPowder Engineering Co., Ltd., this system integrates advanced pneumatic conveying technology to handle the material with precision and minimal loss. The system is engineered to meet the specific requirements of brown sugar processing facilities, offering a robust and efficient method for material handling.
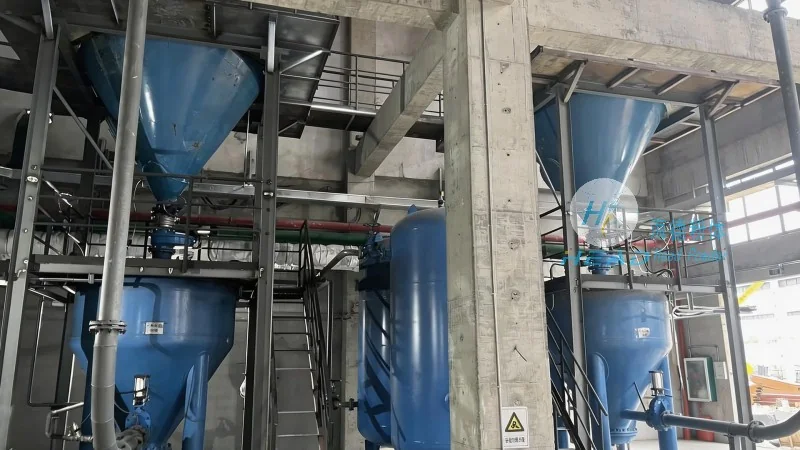
Working Principle of the Pneumatic Conveying System
The core working principle of the brown sugar powder pneumatic conveying system relies on the use of air pressure to move the powder. The system typically operates under positive pressure, where a fan or blower generates a flow of air that carries the brown sugar powder through a network of pipes. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. The air flow, controlled by the system's pressure and flow rate settings, propels the powder through the pipeline to the destination point, such as a storage silo or processing unit. The system ensures that the brown sugar powder is transported without clogging or degradation, maintaining the quality of the material throughout the process.
Key Features and Advantages
Several notable features distinguish the brown sugar powder pneumatic conveying system from traditional methods. Firstly, the system offers high efficiency in material transport, with the ability to move large volumes of brown sugar powder over significant distances with minimal energy consumption. This is achieved through optimized air flow management and efficient pipeline design. Secondly, the system is highly flexible, allowing for easy integration into existing brown sugar processing lines and the ability to adapt to varying production rates. The system also provides excellent dust control, reducing the risk of airborne contamination and improving workplace safety. Additionally, the equipment is designed for easy maintenance and cleaning, ensuring long-term operational reliability. The use of advanced materials and components in the construction of the system enhances its durability and resistance to corrosion, which is particularly important when handling brown sugar powder that may contain moisture or other corrosive elements.
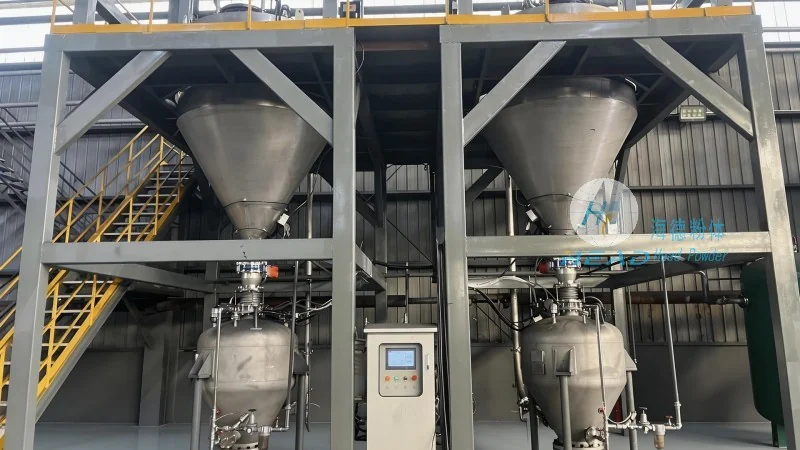
Application and Operational Benefits
The brown sugar powder pneumatic conveying system is widely used in brown sugar processing plants, sugar refineries, and related industries. Its primary operational benefits include improved material handling efficiency, reduced labor costs associated with manual handling, and enhanced product quality through minimized material degradation. The system also contributes to better environmental management by reducing dust emissions and the need for additional dust collection equipment. For companies like Shandong HeadPowder Engineering Co., Ltd., the system represents a cost-effective solution that aligns with modern industrial standards for material transport and processing.