

Operating Process and Working Principle of Sesame Pneumatic Conveying System Equipment
Headpowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for various industrial applications. The company’s flagship product, the sesame pneumatic conveying system, is engineered to efficiently handle sesame seeds and other similar bulk materials with precision and reliability. This equipment is widely utilized in the food processing industry, particularly in sesame processing plants, where it plays a crucial role in material transport and processing. The system combines innovative technology with robust construction to ensure optimal performance under diverse operational conditions.
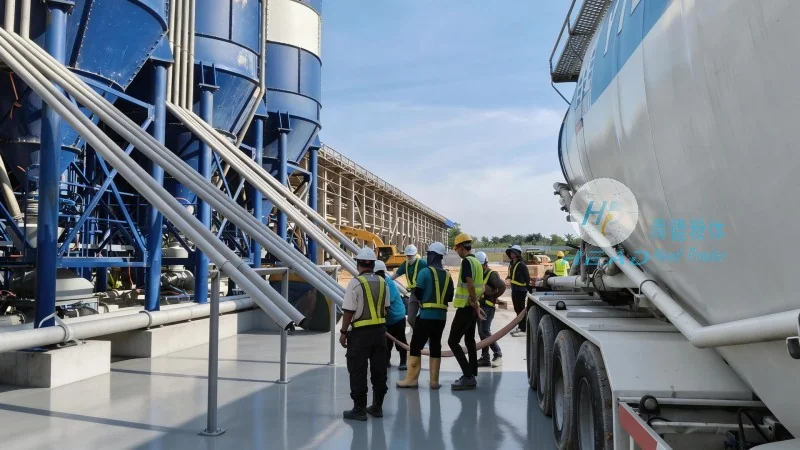
Working Principle of the Sesame Pneumatic Conveying System
The core of the sesame pneumatic conveying system lies in its pneumatic transport mechanism, which utilizes compressed air to move materials through a network of pipes and components. The system operates on the principle of air-assisted transport, where a vacuum or pressure differential is created to draw or push the material along the conveying line. For the sesame pneumatic conveying system, the process typically involves the following key components and their functions:
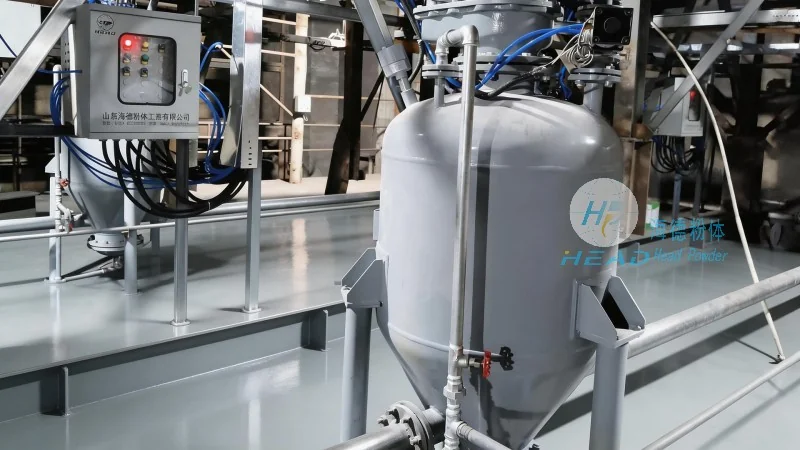
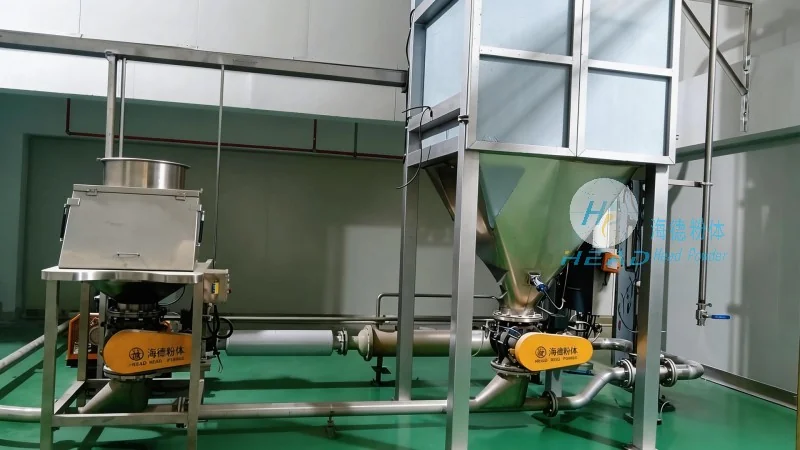
- Feeder: The feeder is responsible for uniformly feeding the sesame seeds into the conveying line. It ensures a consistent flow rate, preventing blockages and maintaining system efficiency.
- Conveying Line: The main pipeline where the sesame seeds are transported. The line is designed with appropriate diameter and material to withstand the pressure and friction caused by the moving material.
- Compressor or Vacuum Pump: This component generates the necessary air pressure or vacuum to move the material. In a pressure system, compressed air is introduced at one end, while in a vacuum system, air is drawn out from the other end.
- Separation and Cleaning Equipment: After the material reaches its destination, this equipment separates the sesame seeds from the air and cleans the system to prevent contamination and maintain hygiene standards.
Operating Process of the Sesame Pneumatic Conveying System
The operation of the sesame pneumatic conveying system follows a systematic sequence to ensure smooth and continuous material transport. The process begins with the preparation of the sesame seeds, which are typically cleaned and conditioned before being fed into the system. The feeder then starts to deliver the material at a controlled rate. Simultaneously, the compressor or vacuum pump activates, creating the required air flow. The air and material mixture travels through the conveying line, with the pressure or vacuum differential propelling the material forward. At the receiving end, the material is deposited into the target container or processing unit. The system also includes automatic controls that monitor pressure, flow rate, and other parameters to maintain optimal performance and prevent system failures.
Technical Advantages and Applications
The sesame pneumatic conveying system offers several technical advantages that make it an ideal choice for sesame processing applications. These include high efficiency in material transport, minimal product degradation due to gentle handling, and reduced labor costs compared to traditional methods. The system is also designed for easy maintenance and cleaning, which is crucial for maintaining food safety standards. Additionally, the system can be customized to meet specific production requirements, such as varying throughput rates or handling different types of bulk materials. In the sesame processing industry, this equipment is commonly used for transporting sesame seeds from storage bins to processing lines, or from processing units to packaging areas. Its ability to handle large volumes of material with minimal downtime makes it a vital component in modern sesame processing facilities.
Conclusion
Headpowder’s sesame pneumatic conveying system equipment exemplifies advanced engineering and practical application in the food processing industry. By leveraging pneumatic transport technology, the system ensures efficient, reliable, and hygienic handling of sesame seeds. The company’s commitment to quality and innovation has positioned it as a trusted provider of pneumatic conveying solutions. For businesses in the sesame processing sector, investing in such equipment can significantly enhance operational efficiency and product quality, contributing to long-term success in a competitive market.