

Operation Process and Working Principle of Brown Sugar Powder Conveying System Equipment
The brown sugar powder conveying system equipment, as a specialized device in the powder handling field, plays a crucial role in the production and processing of brown sugar. This equipment is designed to efficiently transport brown sugar powder from the storage area to the processing line, ensuring smooth production flow and high operational efficiency. The system integrates advanced mechanical and pneumatic technologies, providing stable and reliable conveying performance under various working conditions.
Key Components and Their Functions
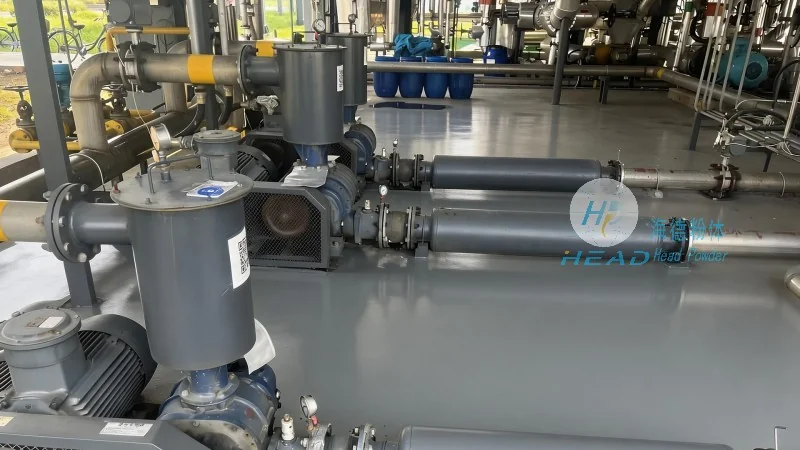
The brown sugar powder conveying system typically consists of several core components, each with specific functions to ensure the system operates as a cohesive unit. The main components include the hopper, which serves as the material storage and feeding device; the conveying pipeline, which transports the powder through air pressure or mechanical force; the control valve, which regulates the flow rate and direction of the powder; and the dust collection system, which ensures environmental safety by capturing and filtering airborne particles. Each component is carefully designed to handle the unique properties of brown sugar powder, such as its moisture content and particle size distribution, to prevent caking or blockages during operation.
Operation Process of the Conveying System
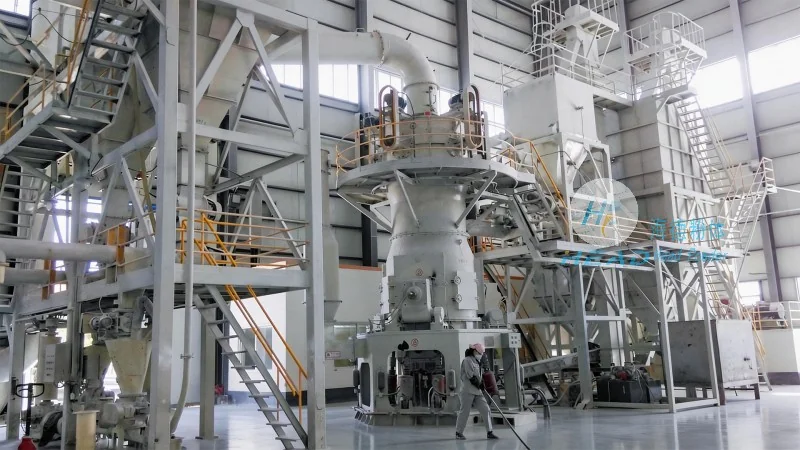
The operation process of the brown sugar powder conveying system involves several sequential steps to ensure efficient material transfer. First, the brown sugar powder is fed into the hopper from the storage silo or batch mixer. The hopper is equipped with a feeding mechanism, such as a rotary valve or screw feeder, which controls the initial flow rate of the powder. Next, the powder is drawn into the conveying pipeline by the air flow generated by the blower or vacuum pump. The air flow carries the powder particles through the pipeline to the discharge point, where the powder is deposited into the next processing equipment, such as a mixer or packaging machine. The system’s control panel monitors and adjusts the air pressure, flow rate, and feeding speed in real-time, allowing operators to maintain optimal conveying conditions. The entire process is automated, reducing manual intervention and minimizing the risk of human error.
Working Principle of the Conveying System
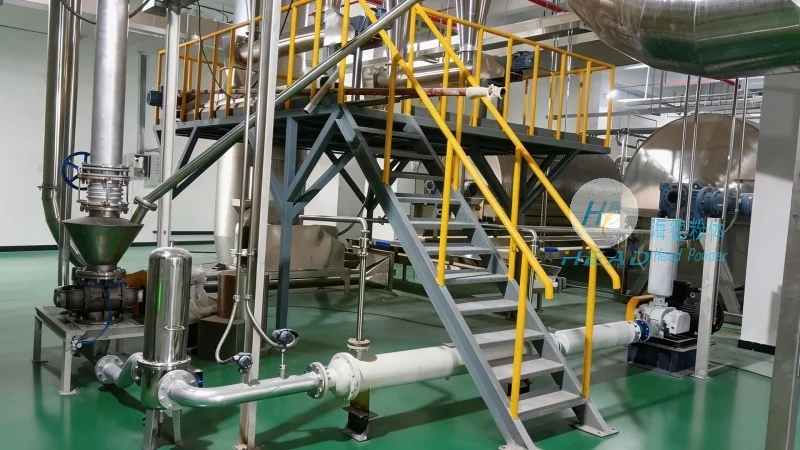
The working principle of the brown sugar powder conveying system is based on the combination of pneumatic conveying technology and mechanical feeding. The system utilizes a pressure or vacuum system to create a flow of air through the conveying pipeline. When the system operates under pressure, the blower pushes air into the pipeline, creating a positive pressure that lifts the powder particles and carries them to the discharge point. Conversely, under vacuum conditions, the vacuum pump draws air out of the pipeline, creating a negative pressure that pulls the powder into the system. The air flow velocity is carefully controlled to ensure that the powder particles are transported without excessive wear or degradation. The system also incorporates a dust collection system, which uses filters and cyclones to separate the powder from the air, preventing dust contamination and maintaining air quality. This integrated approach ensures that the brown sugar powder is conveyed safely and efficiently, with minimal loss or degradation of the product quality.
Advantages of the Brown Sugar Powder Conveying System
The brown sugar powder conveying system offers several advantages over traditional conveying methods, such as bucket elevators or belt conveyors. Firstly, it provides a continuous and uniform flow of powder, reducing the risk of material accumulation or blockages. Secondly, the system is highly flexible, allowing for changes in the conveying route or capacity without major modifications. Thirdly, it operates with low energy consumption, as the air flow is the primary driving force, which is more energy-efficient than mechanical systems. Additionally, the system is easy to maintain and clean, with components that can be easily accessed and replaced. The dust collection system also ensures that the working environment is clean and safe, complying with industrial hygiene standards. These advantages make the brown sugar powder conveying system an ideal choice for modern brown sugar production facilities, where efficiency, safety, and product quality are paramount.
About Shandong HeadPowder Engineering Co., Ltd.
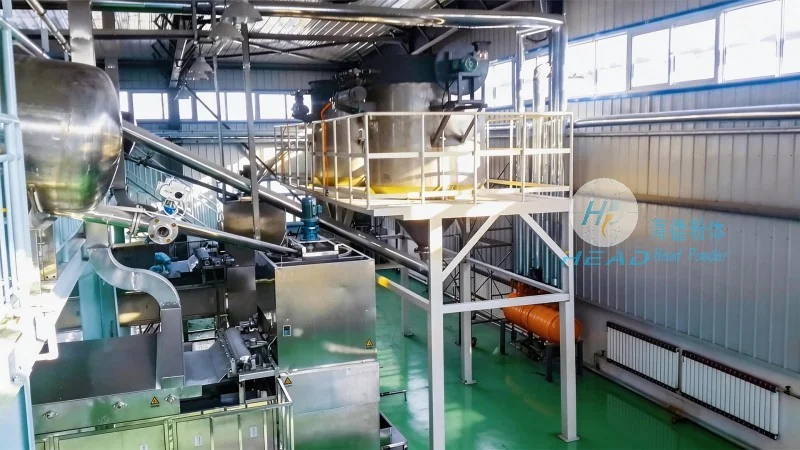
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of powder handling equipment in China. With a focus on innovation and quality, the company has developed a wide range of conveying systems tailored to the specific needs of various industries, including food processing, pharmaceuticals, and chemicals. The company’s brown sugar powder conveying system is a result of years of research and development, incorporating the latest technological advancements to meet the demands of modern production. Headpowder is committed to providing reliable and efficient equipment that enhances the productivity and safety of its clients’ operations. The company’s headquarters is located in Shandong, China, where it has a strong team of engineers and technicians dedicated to product development and customer support. With a reputation for excellence, headpowder continues to be a trusted partner for businesses seeking high-quality powder handling solutions.