

Operation Process and Working Principle of Tonne Bag Unloading Material Pneumatic Conveying Machine
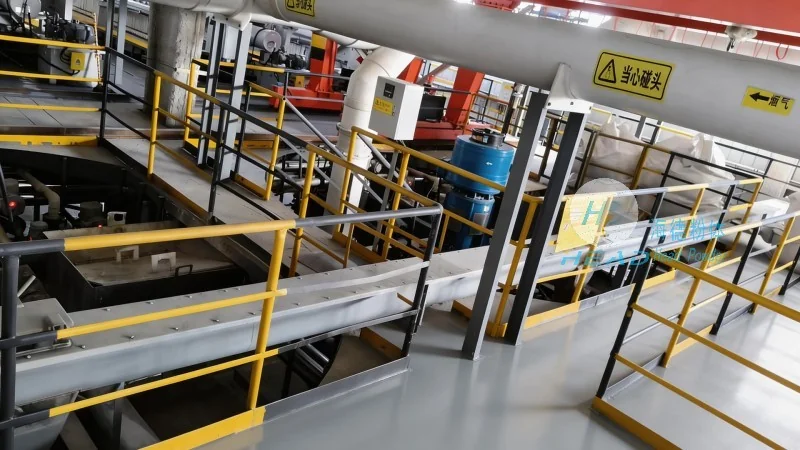
For industries dealing with bulk material handling, efficient and reliable equipment is crucial to streamline operations and enhance productivity. The Tonne Bag Unloading Material Pneumatic Conveying Machine, offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to address the challenges of handling large quantities of materials from tonne bags. This equipment integrates advanced pneumatic conveying technology with robust engineering to ensure seamless material transfer, reduced downtime, and improved safety in industrial settings.
Company Overview
HeadPowder, as the brand of Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in bulk material handling solutions. With a strong presence in China, particularly in Shandong, the company has built a reputation for delivering high-quality, durable, and efficient equipment tailored to the needs of various industrial sectors. The company's commitment to innovation and customer satisfaction has positioned it as a trusted partner for businesses seeking reliable material handling systems.
Key Features and Technical Specifications
The Tonne Bag Unloading Material Pneumatic Conveying Machine is engineered with precision to handle a wide range of materials, including powders, granules, and other bulk substances. Key features include a robust bag opening mechanism, efficient airlock systems, and adjustable conveying speeds to accommodate different material properties and processing requirements. The machine is designed to handle up to several tonnes of material per hour, making it suitable for high-volume applications in industries such as chemicals, food processing, and mining. Advanced materials are used in the construction to ensure durability and resistance to corrosion, extending the equipment's service life and reducing maintenance costs.
Operation Process
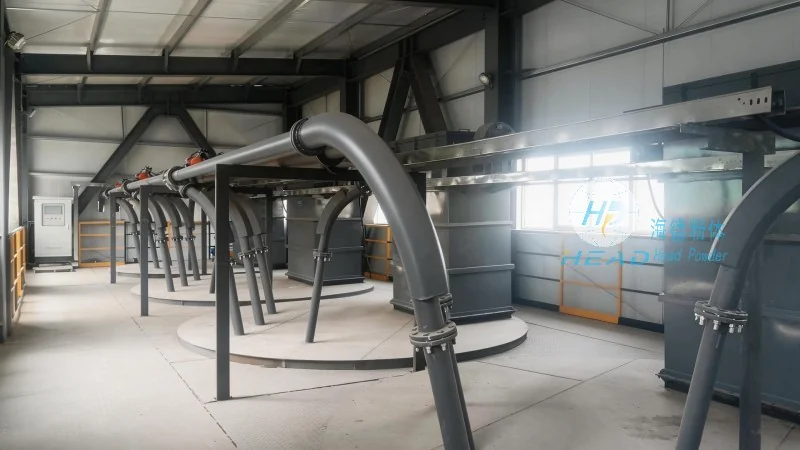
The operation of the Tonne Bag Unloading Material Pneumatic Conveying Machine involves several key steps that ensure efficient material transfer from the tonne bag to the processing line. First, the tonne bag is positioned on the machine's loading platform, and the bag opening mechanism is activated to break the seal and release the material. Simultaneously, the airlock system is engaged to create a controlled airflow that draws the material into the conveying pipeline. The material is then transported through the pipeline using compressed air, which is regulated to maintain optimal flow rates and prevent blockages. At the discharge end, the material is deposited into a storage hopper or directly into the processing equipment. The entire process is automated, with sensors monitoring the flow rate and pressure to ensure smooth operation and prevent overloading or underflow.
Working Principle
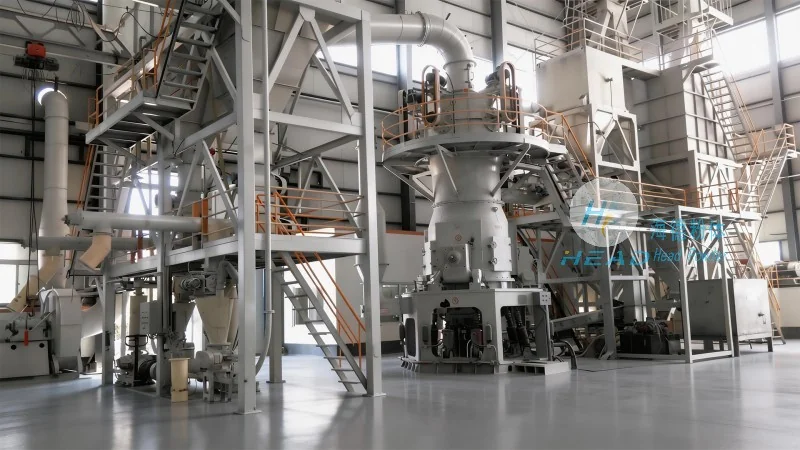
The working principle of the pneumatic conveying machine is based on the use of compressed air to transport bulk materials in a closed system. The machine operates by creating a pressure differential between the inlet and outlet of the conveying pipeline. As compressed air is introduced into the system, it creates a low-pressure zone at the inlet, which draws the material from the tonne bag into the pipeline. The material is then carried by the air stream through the pipeline to the discharge point. The air and material mixture is separated at the discharge end using a cyclone or other separation equipment, with the air being recirculated back to the system and the material being collected. This closed-loop system minimizes material loss and environmental contamination, making it an environmentally friendly solution for bulk material handling.
Benefits and Applications
The Tonne Bag Unloading Material Pneumatic Conveying Machine offers numerous benefits to industrial operations, including increased efficiency, reduced labor costs, and improved safety. By automating the material unloading process, the machine minimizes the need for manual handling, which reduces the risk of accidents and exposure to hazardous materials. The efficient conveying system ensures that material is transferred quickly and reliably, reducing downtime and increasing overall productivity. The machine is suitable for a wide range of applications, including the handling of chemicals, food products, pharmaceuticals, and mining materials. Its versatility and adaptability make it an ideal solution for businesses looking to streamline their material handling processes and improve operational efficiency.