

Classification and Composition of Barley Pneumatic Conveying Systems
Barley pneumatic conveying systems are essential in the agricultural and food processing industries, designed to efficiently transport barley grains from storage facilities to processing units. These systems leverage air pressure to move bulk materials, offering advantages such as reduced labor costs, improved hygiene, and enhanced safety compared to traditional mechanical conveyors. Understanding the classification and composition of these systems is crucial for selecting the most suitable solution for specific operational needs.
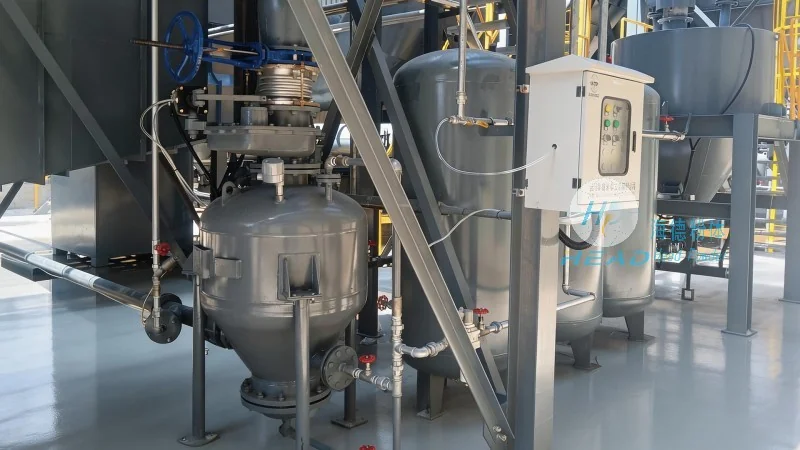
Classification of Barley Pneumatic Conveying Systems
Barley pneumatic conveying systems can be classified based on several key parameters, including the pressure differential between the conveying air and the ambient air, the type of material handling, and the system configuration. The primary classifications include:
- Positive Pressure Systems: These systems operate by blowing air into the conveying line, creating positive pressure that pushes the barley grains forward. They are commonly used for short to medium-distance transport and are suitable for handling fine or dusty materials.
- Negative Pressure (Suction) Systems: In contrast, negative pressure systems draw air and material through a vacuum, pulling the barley grains into the system. This method is ideal for long-distance transport and for handling materials that are prone to dust generation or require a clean environment.
- Combined Systems: Some applications utilize a combination of both positive and negative pressure, allowing for flexibility in material handling and system design.
Key Components of Barley Pneumatic Conveying Systems
Regardless of the classification, barley pneumatic conveying systems typically consist of several core components that work in tandem to ensure efficient operation. These components include:
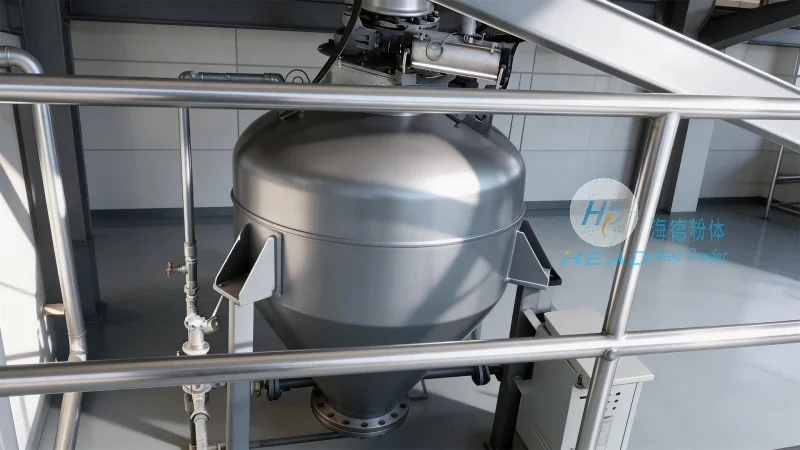
- Feed Hopper and Metering Device: The feed hopper stores the barley and feeds it into the system at a controlled rate. The metering device, often a rotary valve or a screw feeder, regulates the flow of material to maintain consistent conveying performance.
- Pneumatic Conveying Pipe: The pipe network forms the backbone of the system, transporting the barley grains mixed with air. The pipe material is usually stainless steel or plastic, chosen for its durability, corrosion resistance, and ability to handle abrasive materials like barley.
- Air Source and Blower Unit: The blower or compressor generates the necessary air pressure or vacuum. The air source is typically equipped with filters to remove contaminants and ensure clean air for the conveying process.
- Separation and Cleaning Equipment: At the receiving end, separation equipment, such as cyclones or filters, separates the barley from the air stream. This step is critical for maintaining product quality and preventing dust accumulation in downstream processes.
- Control System: Modern barley pneumatic conveying systems are often equipped with a control panel that monitors and regulates the operation of the system. This includes sensors for pressure, flow, and material level, ensuring safe and efficient operation.
Application and Operational Considerations
The choice of a specific barley pneumatic conveying system depends on various factors, including the distance of transport, the volume of material to be handled, and the required level of dust control. For example, positive pressure systems are preferred for short-distance transport in grain elevators, while negative pressure systems are more suitable for long-distance transport in agricultural processing facilities.
Operational considerations also include the need to maintain proper air-to-material ratios to prevent blockages or excessive pressure drops. Regular maintenance of the system components, such as cleaning the filters and checking the blower performance, is essential to ensure long-term reliability and efficiency.
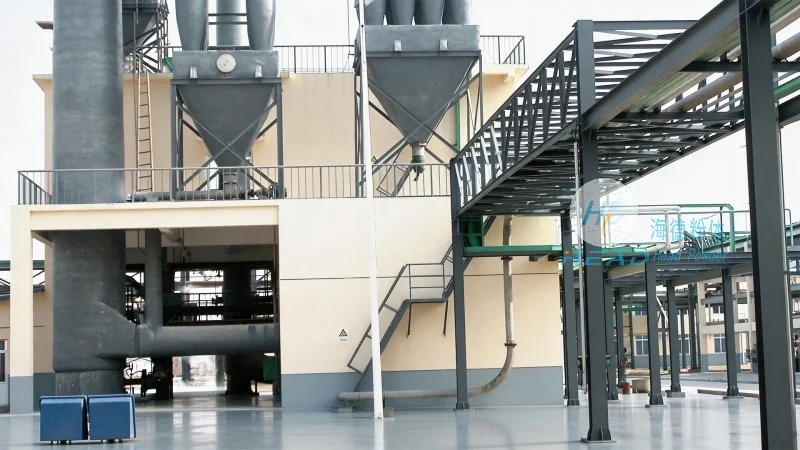
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for the agricultural and food processing sectors. With a focus on innovation and quality, the company provides customized solutions tailored to the specific needs of its clients, ensuring optimal performance and reliability in barley handling operations.
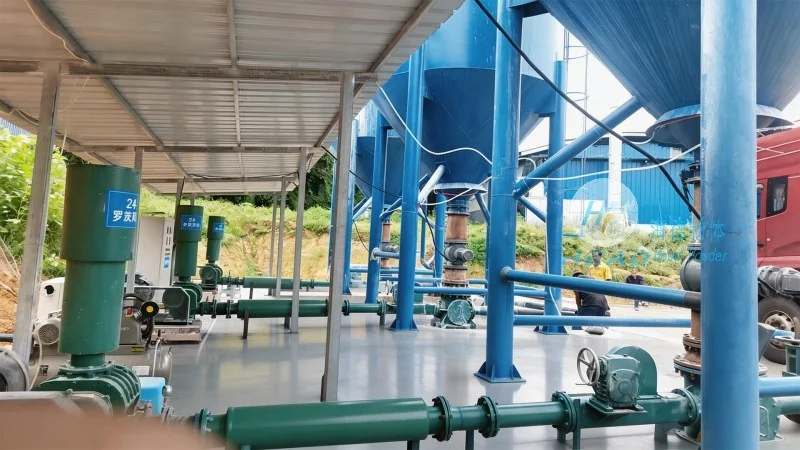
HeadPowder's expertise lies in understanding the unique challenges of barley processing, such as the material's density, moisture content, and potential for dust generation. By leveraging state-of-the-art technology and rigorous quality control, the company delivers systems that meet the highest industry standards, contributing to improved productivity and operational efficiency for its clients.
Headquartered in Shandong, China, headpowder serves a global market, providing comprehensive support from system design and engineering to installation and after-sales service. The company's commitment to customer satisfaction and technological advancement has established it as a trusted partner in the pneumatic conveying industry.