

Classification and Composition of Borax Granule Pneumatic Conveying Systems
HeadPowder, a leading provider in the field, specializes in the design and implementation of pneumatic conveying systems for borax granules. This article outlines the classification and key components of such systems, offering insights into their functionality and application.
Classification of Borax Granule Pneumatic Conveying Systems
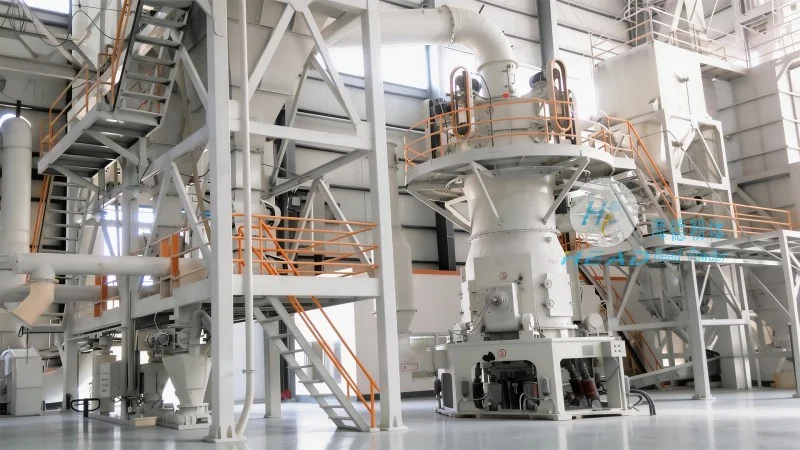
Borax granule pneumatic conveying systems are typically classified based on the air flow rate and the density of the material being transported. The primary categories include dense-phase and dilute-phase systems. Dense-phase systems operate at lower air velocities, ensuring a more controlled and efficient transfer of granules, which is crucial for handling borax granules that may be sensitive to high velocities or pressure changes. Dilute-phase systems, on the other hand, use higher air velocities to transport materials in a more fluidized state, suitable for longer distances or when the material is less abrasive. The choice between these systems depends on factors such as the required conveying distance, material characteristics, and operational efficiency.
Key Components of Borax Granule Pneumatic Conveying Systems
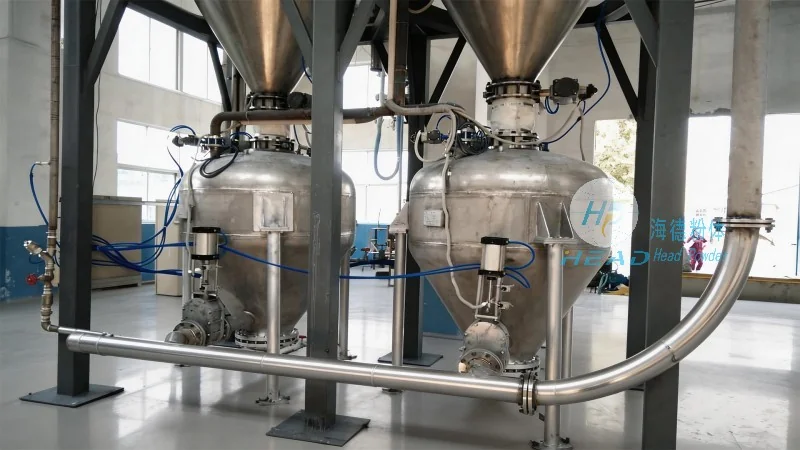
The effective operation of a borax granule pneumatic conveying system relies on several critical components, each designed to perform a specific function. The primary components include:
- Feeding Unit: This component is responsible for introducing the borax granules into the system. It may consist of a hopper, a rotary valve, or a screw feeder, ensuring a consistent and controlled flow of material into the conveying line. The feeding unit is crucial for maintaining the integrity of the granules and preventing blockages or uneven flow.
- Pneumatic Conveying Line: The pipeline system that transports the borax granules and air mixture. It is typically made of materials such as stainless steel or plastic, chosen for their resistance to corrosion and abrasion from the borax granules. The design of the pipeline, including the use of bends, elbows, and expansion joints, is critical to minimize pressure losses and maintain the efficiency of the conveying process.
- Air Source System: This includes the compressor, air dryer, and filter. The compressor provides the necessary pressure and volume of air to move the borax granules through the pipeline. The air dryer removes moisture from the air, preventing the formation of clumps or moisture-related issues in the borax granules. The filter ensures that the air is clean, protecting the system components from dust and debris.
- Separation and Collection Equipment: At the receiving end of the system, this component separates the borax granules from the air stream. It may include a cyclone separator, a bag filter, or a venturi scrubber. The cyclone separator uses centrifugal force to separate the granules from the air, while the bag filter captures fine particles. The choice of equipment depends on the required separation efficiency and the characteristics of the borax granules.
Application and Benefits of Borax Granule Pneumatic Conveying Systems
Borax granule pneumatic conveying systems are widely used in industries such as chemical manufacturing, food processing, and pharmaceuticals, where the efficient and safe transfer of borax granules is essential. The benefits of these systems include improved safety by eliminating the need for manual handling of granules, increased efficiency through automated operation, and reduced maintenance costs due to the use of durable materials and components. Additionally, the systems can be designed to handle varying volumes of borax granules, making them adaptable to different production needs.
About HeadPowder Engineering Co., Ltd.
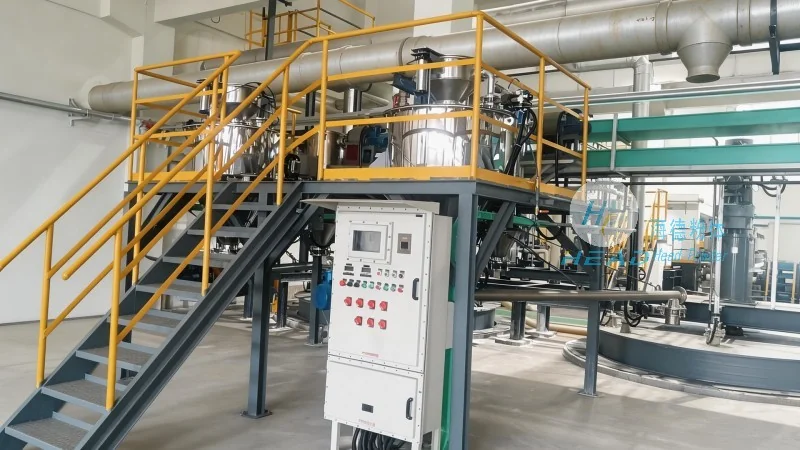
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable company specializing in the design, manufacturing, and installation of pneumatic conveying systems. With years of experience in the industry, HeadPowder provides customized solutions tailored to the specific requirements of clients, ensuring high-quality and reliable operation of borax granule pneumatic conveying systems. The company's commitment to innovation and customer satisfaction has made it a trusted partner in the field of material handling.