

Analysis of Fly Ash Pneumatic Conveying Systems
For industrial facilities dealing with fly ash, the efficient and reliable transportation of this material is crucial. Fly ash, a byproduct of coal combustion, requires specialized handling systems to ensure safety, environmental compliance, and operational efficiency. This article provides an in-depth analysis of fly ash pneumatic conveying systems, exploring their design, functionality, and the key considerations for implementation in industrial settings.
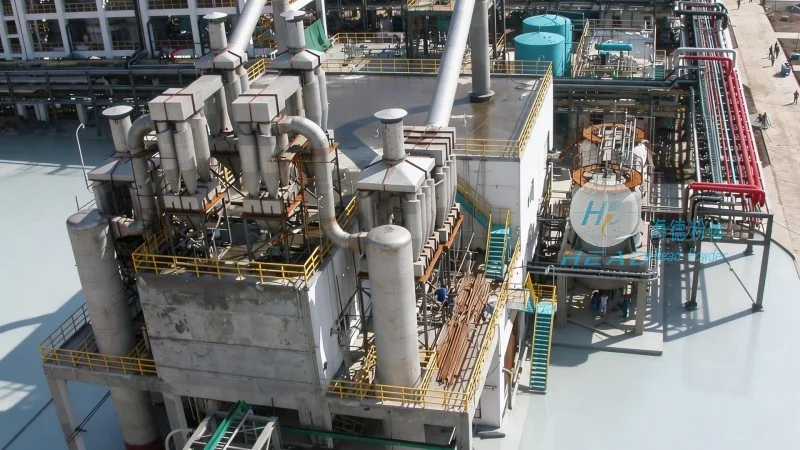
Overview of Fly Ash Pneumatic Conveying Systems
Fly ash pneumatic conveying systems are engineered to transport fly ash from its source, such as a boiler or storage silo, to a disposal or utilization destination. These systems utilize air pressure or vacuum to move the fine, abrasive material through a network of pipes. The technology offers significant advantages over traditional methods like belt conveyors or bucket elevators, including reduced dust emissions, lower maintenance costs, and the ability to handle high volumes of material over long distances.
Key Components and Working Principle
The core components of a fly ash pneumatic conveying system typically include a feeder, a conveying line, a separation unit, and a control system. The feeder, often a rotary valve or screw feeder, introduces the fly ash into the system at a controlled rate. The conveying line, made of materials resistant to abrasion and corrosion (such as stainless steel or high-density polyethylene), transports the material using either positive pressure (where air is forced through the line) or negative pressure (where air is drawn out). The separation unit, such as a cyclone or bag filter, separates the ash from the air stream, allowing the air to be recirculated or discharged while the ash is collected for further use or disposal.
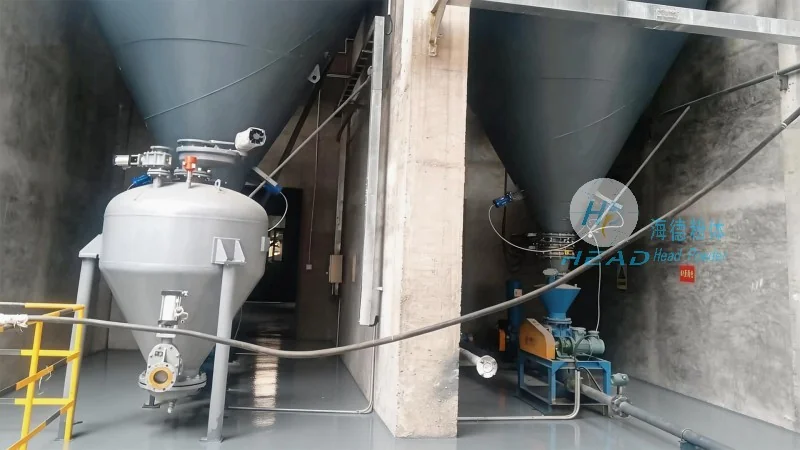
Advantages of Pneumatic Conveying for Fly Ash
Implementing a pneumatic conveying system for fly ash offers several benefits that enhance operational performance and sustainability. First, it minimizes dust generation, which is critical for maintaining a clean working environment and complying with environmental regulations. Second, the system reduces the need for multiple transfer points, streamlining the material handling process and lowering labor costs. Third, the technology is highly flexible, allowing for changes in material flow rates or destinations without major modifications to the infrastructure. Additionally, the system can be integrated with other industrial processes, such as ash utilization in cement production, improving overall plant efficiency.
Application Scenarios and Industrial Use Cases
Fly ash pneumatic conveying systems are widely used in power plants, cement factories, and other industrial facilities that generate large quantities of fly ash. In power plants, the system efficiently transports ash from the boiler to storage silos or directly to utilization sites, such as cement kilns. In cement factories, fly ash is often used as a supplementary cementitious material, and the conveying system ensures a consistent and high-quality feed to the production line. The system's ability to handle fine, abrasive materials makes it suitable for applications where traditional conveyors may experience wear and tear or clogging.
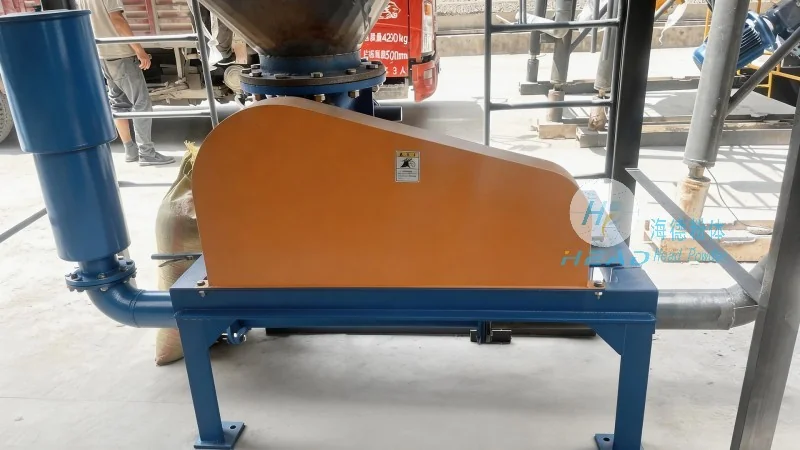
Engineering and Installation by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, specializes in designing and implementing fly ash pneumatic conveying systems tailored to the specific needs of clients. With offices in China, the company leverages decades of experience in the field to deliver customized solutions that meet regulatory standards and operational requirements. The engineering team at HeadPowder conducts thorough assessments of client facilities, including material characteristics, flow rates, and distance requirements, to design systems that optimize performance and longevity. The company's commitment to quality and innovation ensures that each system is built to withstand the harsh conditions associated with fly ash handling, providing reliable operation over the long term.
Conclusion and Future Considerations
As industrial facilities continue to prioritize efficiency and sustainability, fly ash pneumatic conveying systems remain a critical component of modern material handling infrastructure. By leveraging advanced engineering and robust design, these systems offer a reliable solution for transporting fly ash while minimizing environmental impact. For companies seeking to upgrade their ash handling processes, partnering with experienced providers like Shandong HeadPowder Engineering Co., Ltd. ensures access to tailored solutions that enhance operational performance and support long-term business goals.