

Principle and Classification Application of Coal Sand Pneumatic Conveying
Coal sand pneumatic conveying is a critical technology in material handling, particularly for transporting coal and sand particles efficiently. This method utilizes air as the medium to move bulk materials through a pipeline system. The process involves creating a pressure or vacuum difference to transport the material, which is essential for industries dealing with bulk solids like coal and sand. Understanding the working principle and classification of this technology is vital for optimizing material handling operations.
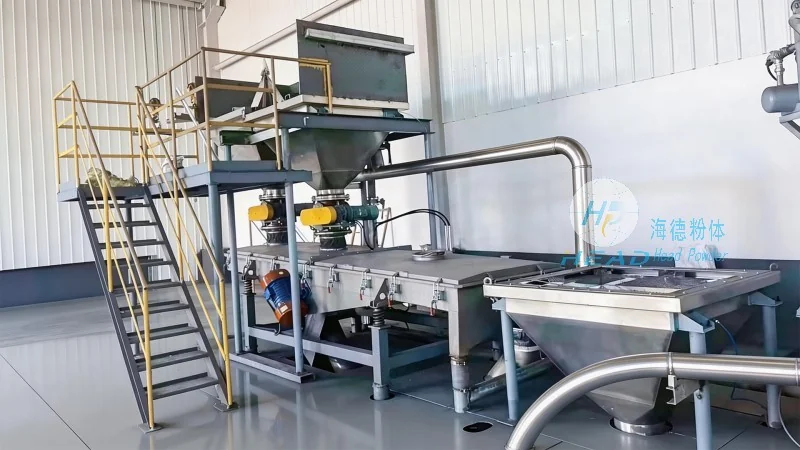
Working Principle of Coal Sand Pneumatic Conveying
The core principle of coal sand pneumatic conveying is the use of air flow to transport solid particles. The system typically consists of a source of material, a conveying line, and a receiver. The operation can be categorized into two main types: suction (or vacuum) conveying and pressure conveying. In suction conveying, a vacuum is created at the material inlet to draw the particles into the pipeline. This method is suitable for short distances and low material density. Pressure conveying, on the other hand, uses compressed air to push the material through the pipeline. This approach is ideal for longer distances and higher material loads. The choice between these methods depends on factors such as the distance of transport, the material's properties, and the required system pressure.
Classification of Coal Sand Pneumatic Conveying Systems
Coal sand pneumatic conveying systems are classified based on the pressure differentials and the method of air and material introduction. The primary classifications include:
1. Single-Stage Suction Conveying: This system uses a single vacuum source to transport material from the source to the receiver. It is commonly used for short-distance transport of light materials like coal dust or fine sand. The simplicity of this system makes it cost-effective for small-scale applications.
2. Multi-Stage Suction Conveying: For longer distances, multi-stage suction systems are employed. These systems use intermediate vacuum boosters to maintain the pressure differential over extended pipelines. This approach is suitable for transporting materials over several hundred meters while maintaining efficiency.
3. Pressure Conveying: In pressure systems, compressed air is used to push the material through the pipeline. This method is more efficient for high-volume and long-distance transport. Pressure conveying can be further divided into positive pressure and negative pressure systems, depending on the direction of air flow relative to the material.
4. Mixed-Phase Conveying: Some systems combine both suction and pressure principles. This hybrid approach allows for flexible operation, adapting to varying material conditions and transport requirements. Mixed-phase systems are often used in complex material handling scenarios where both suction and pressure modes are beneficial.
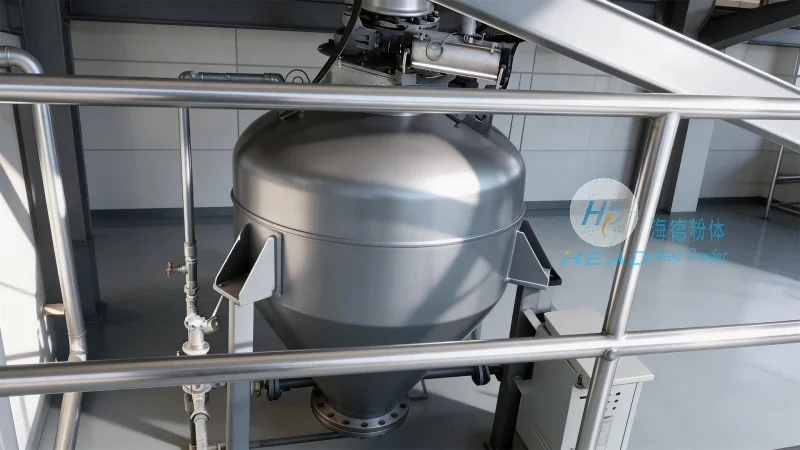
Application Scenarios in Industrial Settings
Coal sand pneumatic conveying is widely applied in various industrial sectors due to its efficiency and adaptability. Key applications include:
1. Coal Handling in Power Plants: Power plants require reliable coal transport from storage to boilers. Pneumatic conveying systems efficiently move coal from stockpiles to the boiler feed system, ensuring continuous operation. The technology minimizes dust and spillage, enhancing safety and environmental compliance.
2. Sand and Gravel Transport in Construction: Construction sites often need to transport sand and gravel for concrete production. Pneumatic conveyors can handle these bulk materials with minimal maintenance, reducing labor costs and improving productivity. The systems are designed to handle abrasive materials without significant wear, ensuring long-term durability.
3. Mineral Processing and Mining: In mining operations, pneumatic conveying is used to transport ore and sand from processing plants to storage or further processing facilities. The technology is robust and can handle high volumes of material, making it suitable for large-scale mining operations.
4. Industrial Dust Collection and Material Recovery: Pneumatic conveying systems are also used in dust collection processes, where they transport collected dust back to storage or disposal areas. This method helps in maintaining clean working environments and recovering valuable materials from industrial processes.
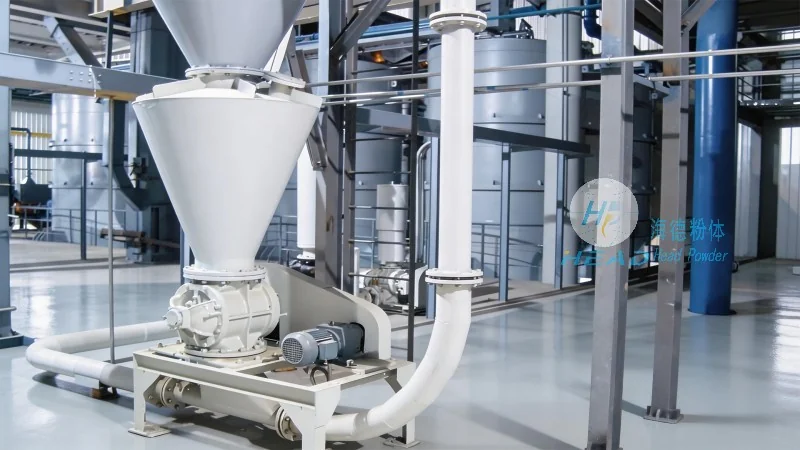
Advantages of Coal Sand Pneumatic Conveying
Implementing coal sand pneumatic conveying offers several advantages over traditional material handling methods. These benefits include:
1. Reduced Labor and Maintenance Costs: Automated systems minimize the need for manual handling, reducing labor expenses. The enclosed pipeline system also reduces wear and tear on equipment, lowering maintenance requirements.
2. Improved Safety and Environmental Control: Pneumatic conveying prevents dust emissions and material spillage, enhancing workplace safety. The enclosed system also helps in controlling dust pollution, meeting environmental regulations.
3. Efficient Material Transport: The technology allows for high-volume and continuous material transport, improving production efficiency. The speed and reliability of pneumatic systems ensure that materials are delivered on time, supporting smooth industrial operations.
4. Flexibility in Layout and Layout Adaptation: Pneumatic conveying systems can be easily integrated into existing industrial layouts. The flexible pipeline design allows for changes in transport routes without major structural modifications, providing operational flexibility.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems. With a focus on innovation and quality, HeadPowder specializes in designing and manufacturing coal sand pneumatic conveying solutions tailored to the needs of various industries. The company's headquarters is located in Shandong, China, where it leverages advanced technology and expertise to deliver reliable and efficient material handling systems. HeadPowder's products are known for their durability, efficiency, and compliance with industry standards, making them a trusted choice for businesses seeking to optimize their material transport processes.