

Principles and Classification Applications of Rare Earth Pneumatic Conveying
Rare earth materials are crucial in modern industrial applications, and efficient material handling is essential for their processing and distribution. Pneumatic conveying, a technology that uses air or gas to transport bulk materials, has become a preferred method for handling rare earth powders due to its advantages in cleanliness, speed, and flexibility. This article explores the fundamental principles of rare earth pneumatic conveying, its classification based on operational characteristics, and practical applications in various industrial settings. The discussion is presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions.
Basic Principles of Pneumatic Conveying for Rare Earth Materials
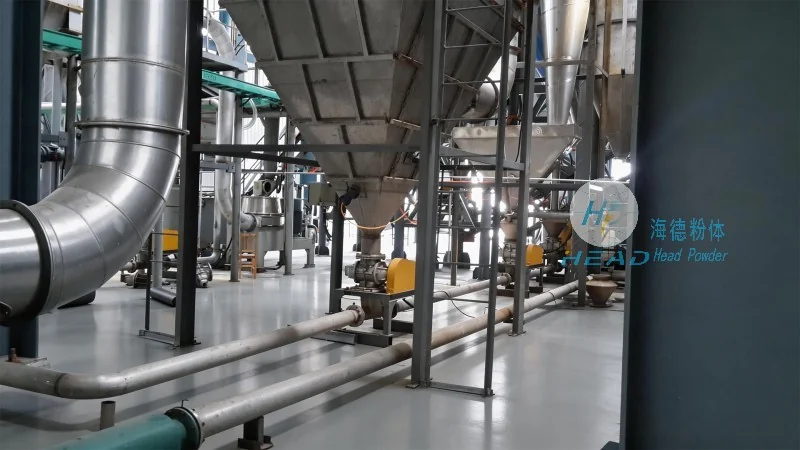
The core principle of pneumatic conveying is the use of a fluid (usually air) to move solid particles through a pipeline. In the context of rare earth materials, which often exist as fine powders or granules, the conveying process relies on creating a flow of air that can carry the particles. There are two main types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at higher velocities, where particles are suspended in the air stream, while dense-phase systems use lower velocities and higher air pressure to push particles along the pipeline. For rare earth powders, which can be abrasive and have specific handling requirements, the choice of system depends on factors such as particle size, moisture content, and the distance to be conveyed. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing these systems to ensure optimal performance and minimal material degradation.
Classification of Pneumatic Conveying Systems for Rare Earth Handling
Pneumatic conveying systems are classified based on their operational characteristics and the way they transport materials. The primary classifications include: 1. Positive Pressure Systems: These systems use a blower or compressor to generate air pressure that pushes the material through the pipeline. They are suitable for long-distance conveying and can handle a wide range of particle sizes. 2. Negative Pressure (Vacuum) Systems: These systems create a vacuum in the pipeline to draw material from a hopper or storage bin. They are ideal for applications where the material needs to be collected from multiple points or where the material is sensitive to air exposure. 3. Hybrid Systems: These combine elements of both positive and negative pressure, offering flexibility in handling different material types and conveying distances. For rare earth materials, the selection of a system type is critical to ensure efficient and safe material transport. Shandong HeadPowder Engineering Co., Ltd. offers customized solutions that match the specific requirements of each client, ensuring that the chosen system maximizes efficiency and minimizes operational costs.
Key Applications of Pneumatic Conveying in Rare Earth Processing
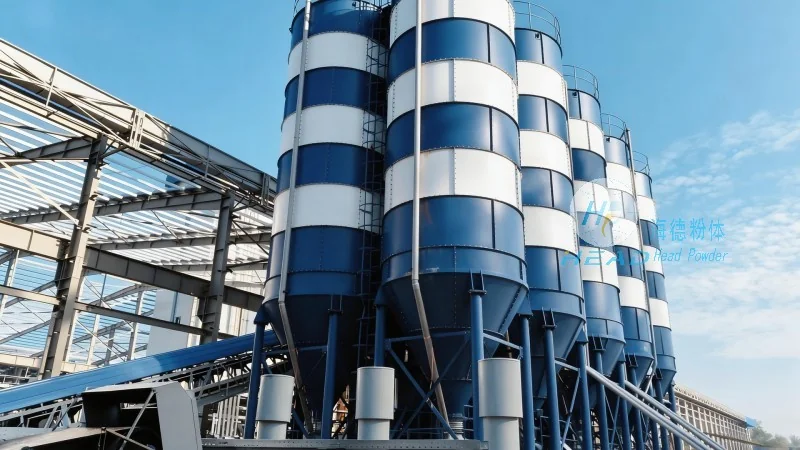
Rare earth pneumatic conveying is widely used in various stages of rare earth processing, from raw material handling to final product distribution. Some key applications include: 1. Raw Material Transport: Conveying rare earth ores or concentrates from mining sites to processing facilities. 2. Milling and Grinding: Moving fine powders between grinding mills and classifiers. 3. Drying and Conditioning: Transporting dried rare earth powders to storage or packaging areas. 4. Packaging and Filling: Conveying final products into containers for shipment. Each of these applications requires a tailored pneumatic conveying system to handle the specific characteristics of the rare earth material, such as its particle size distribution, moisture content, and chemical properties. Shandong HeadPowder Engineering Co., Ltd. has extensive experience in designing systems for these applications, ensuring that the material is handled with precision and minimal loss.
Advantages of Pneumatic Conveying for Rare Earth Materials
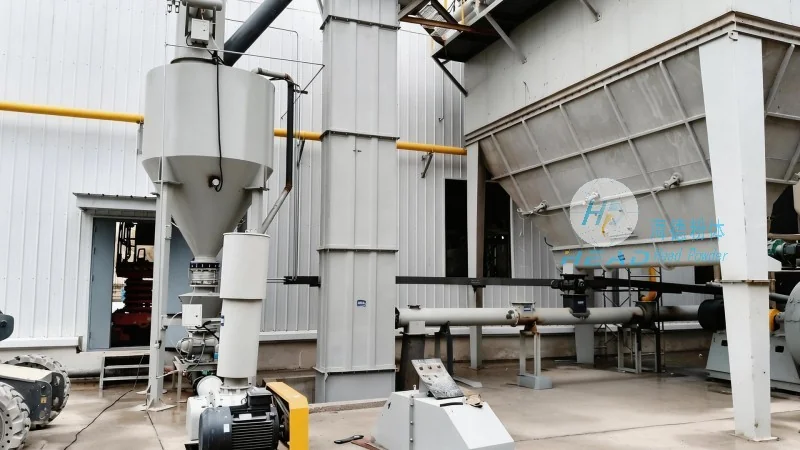
Compared to traditional material handling methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages for rare earth materials: 1. Cleanliness: The enclosed system prevents contamination from dust and other particles, which is crucial for rare earth materials used in high-purity applications. 2. Speed: Pneumatic conveying can transport materials at high speeds, reducing processing time and increasing productivity. 3. Flexibility: The system can be easily reconfigured to handle different material types or to change the conveying route. 4. Low Maintenance: With fewer moving parts compared to mechanical systems, pneumatic conveying systems require less maintenance and have longer service lives. 5. Energy Efficiency: Modern systems use advanced blowers and compressors that are more energy-efficient, reducing operational costs. These advantages make pneumatic conveying an attractive option for industries dealing with rare earth materials. Shandong HeadPowder Engineering Co., Ltd. leverages these benefits to provide clients with reliable and efficient material handling solutions.
Customization and Integration by Shandong HeadPowder Engineering Co., Ltd.
At Shandong HeadPowder Engineering Co., Ltd., we understand that each rare earth processing facility has unique requirements. Our approach to pneumatic conveying system design involves a thorough analysis of the material characteristics, processing needs, and operational constraints. We work closely with clients to develop customized solutions that meet their specific goals. Our team of engineers and technicians has extensive experience in designing and implementing both dilute-phase and dense-phase systems, ensuring that the chosen system is optimized for the material being handled. We also provide integration services, ensuring that the pneumatic conveying system works seamlessly with existing equipment and processes. Our commitment to quality and customer satisfaction has made us a trusted partner for industries dealing with rare earth materials. We are dedicated to providing solutions that enhance efficiency, reduce costs, and improve overall performance.