

Types, Features, and Application Ranges of Pneumatic Conveying for Wheat Starch
Wheat starch is a vital component in numerous industries, including food processing, pharmaceuticals, and cosmetics. Efficient material handling is crucial for preserving product quality and operational efficiency. Pneumatic conveying systems have become a preferred solution for transporting wheat starch due to their versatility, hygiene, and ability to handle fine powders. This article examines the different types of pneumatic conveying systems used for wheat starch, their key features, and the diverse application ranges where they are applied.
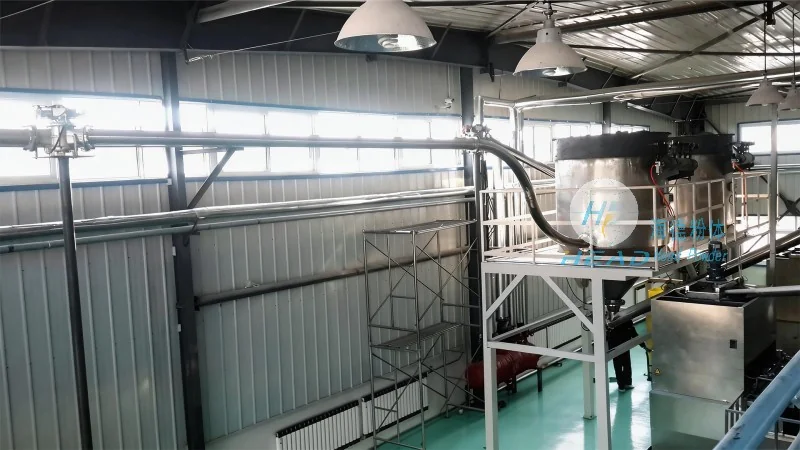
Types of Pneumatic Conveying Systems
Two primary types of pneumatic conveying systems are commonly utilized for wheat starch: pressure and vacuum systems. Each type has distinct operational characteristics and is suited to different requirements.
Pressure systems operate by forcing air or gas through the conveying line under pressure, typically using positive displacement blowers or compressors. These systems are ideal for long-distance and high-volume transport of wheat starch. They effectively handle abrasive materials and maintain consistent flow rates, minimizing product degradation. Pressure systems are particularly effective for conveying distances exceeding 100 meters and when transporting to multiple destinations.
Vacuum systems, conversely, create a negative pressure in the conveying line to draw wheat starch from the source. These systems are often used for shorter distances and when handling fine powders prone to dusting, requiring gentle handling. They are commonly employed for transferring wheat starch from hoppers or silos to processing units within a facility.
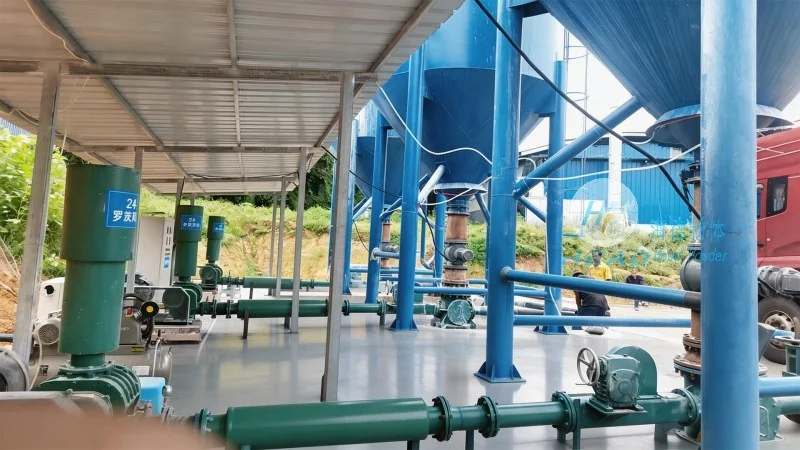
Key Features of Wheat Starch Pneumatic Conveying
The effectiveness of pneumatic conveying for wheat starch stems from several key features that enhance performance and product integrity.
Firstly, these systems are designed for high hygiene, critical for food-grade applications. Enclosed conveying lines prevent contamination and minimize dust exposure, ensuring wheat starch remains pure and safe. This is especially important in the food and pharmaceutical industries where product quality and safety are paramount.
Secondly, pneumatic conveying systems offer layout flexibility and easy integration with existing facilities. They can be adapted along walls or overhead, optimizing space utilization. The modular design allows for easy expansion or modification as production needs change, providing long-term cost efficiency.
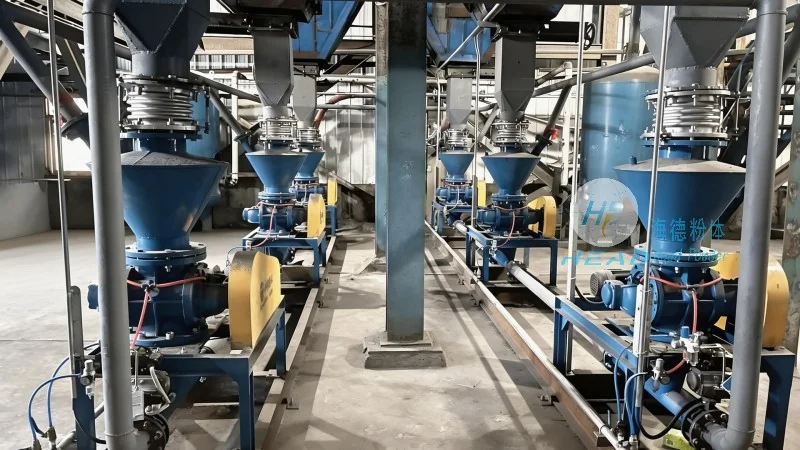
Thirdly, these systems are energy-efficient compared to traditional mechanical methods. Using air as the conveying medium reduces reliance on heavy machinery and lowers energy consumption. This not only cuts operational costs but also supports environmental sustainability. Low-pressure or vacuum systems further enhance energy efficiency, making them attractive for companies aiming to reduce their carbon footprint.
Application Ranges of Pneumatic Conveying for Wheat Starch
Pneumatic conveying systems for wheat starch find applications across various industries, each requiring specific handling characteristics.
In the food processing industry, these systems transport wheat starch from storage silos to mixing and packaging lines. The ability to handle fine powders without caking or agglomeration is crucial for maintaining the quality of baked goods and other food products. They are also used in producing modified starches, where precise control over the conveying process ensures consistent product properties.
In the pharmaceutical sector, pneumatic conveying is used to transport wheat starch as a filler or binder in tablet and capsule formulations. The hygienic design ensures the starch remains free from contaminants, meeting stringent regulatory requirements. Gentle handling prevents degradation, critical for maintaining the efficacy and stability of pharmaceutical products.
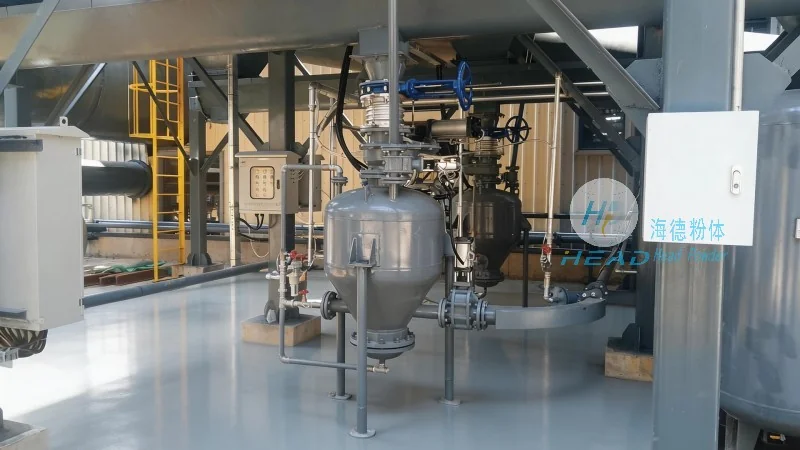
In the cosmetics industry, wheat starch is an ingredient in powders and creams. Pneumatic conveying systems transport the starch from raw material storage to production lines, ensuring a clean and controlled environment. This maintains the purity and quality of final cosmetic products, often marketed as natural or organic.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of pneumatic conveying systems tailored for wheat starch and other fine powders. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry. Based in Shandong, China, HeadPowder Engineering leverages advanced technology and years of experience to design and produce systems that meet unique client needs.
The company's products provide reliable and efficient material handling solutions, ensuring wheat starch is transported safely and efficiently. By combining expertise in material science, engineering, and manufacturing, HeadPowder Engineering delivers systems that enhance operational performance and product quality. The company's commitment to customer satisfaction and continuous improvement has earned it a reputation for excellence in the market.