

Classification and Application Analysis of Glucose Powder Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and application of advanced pneumatic conveying systems for glucose powder. The company, commonly known as HeadPowder, is headquartered in Shandong, China, and has established itself as a key player in providing efficient and reliable solutions for the transportation of glucose powder in various industrial settings.
Classification of Glucose Powder Pneumatic Conveying Systems
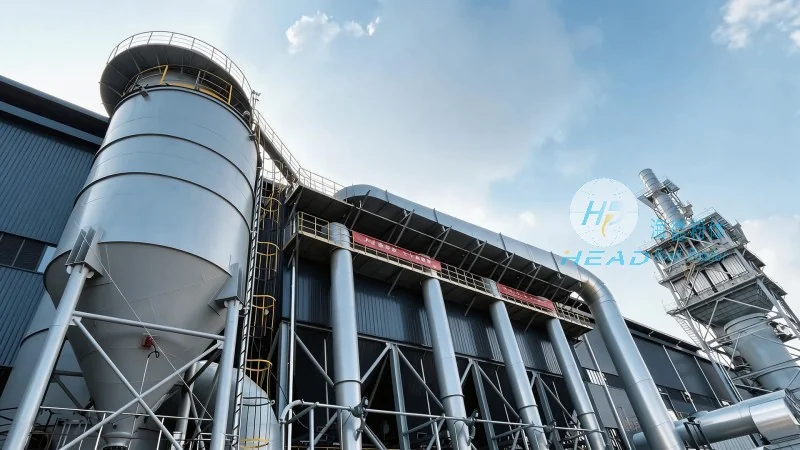
Glucose powder pneumatic conveying systems can be classified based on several key parameters, including the conveying method, pressure level, and application requirements. The primary classification includes positive pressure systems, negative pressure systems, and mixed pressure systems. Positive pressure systems, such as pressure vessels and blowers, generate air pressure to push the powder forward, making them suitable for long-distance and high-capacity applications. Negative pressure systems, often utilizing vacuum pumps, draw the powder into the system, which is ideal for handling fine powders and preventing dust emissions. Mixed pressure systems combine elements of both, offering flexibility for different operational conditions. Additionally, systems can be categorized by the type of air flow, including dilute phase and dense phase conveying. Dilute phase systems use high-velocity air to transport particles in a dispersed state, while dense phase systems employ lower air velocities to move particles in a more concentrated manner, reducing particle degradation and improving material integrity.
Application Analysis of Glucose Powder Pneumatic Conveying Systems
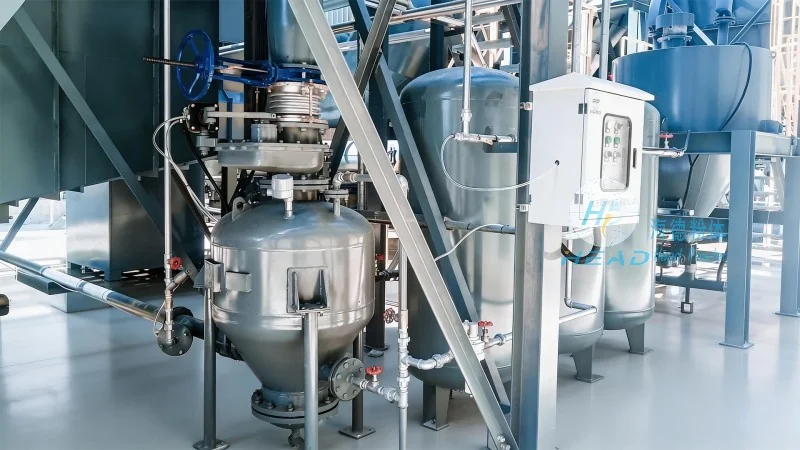
The application of glucose powder pneumatic conveying systems spans multiple industries, including pharmaceuticals, food processing, and chemical manufacturing. In the pharmaceutical sector, these systems are crucial for transporting glucose powder in sterile environments, ensuring compliance with GMP (Good Manufacturing Practice) standards. The systems are designed to minimize contamination and maintain product purity, which is essential for drug production. In food processing, the technology is used to convey glucose powder in food factories, facilitating efficient production lines and maintaining product quality. The systems can handle varying particle sizes and moisture contents, adapting to different food products. In chemical manufacturing, glucose powder is often used as a raw material, and the pneumatic conveying systems ensure safe and efficient transportation, reducing the risk of dust explosions and improving operational safety. The systems are also used in research and development laboratories, where precise control over powder flow is required for experimental processes.
Key Features and Advantages of Glucose Powder Pneumatic Conveying Systems
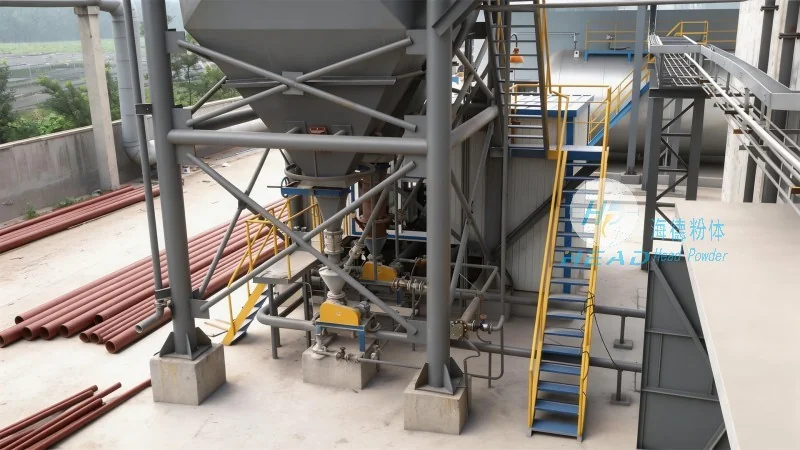
HeadPowder's glucose powder pneumatic conveying systems offer several key features that enhance performance and reliability. The systems are equipped with advanced control systems, allowing for precise regulation of air pressure and flow rates, which optimizes the conveying process and minimizes energy consumption. The use of high-quality materials, such as stainless steel and corrosion-resistant components, ensures durability and long service life, even in harsh operating conditions. The systems are designed for easy maintenance and cleaning, which is critical for industries with strict hygiene requirements. Additionally, the systems can be customized to meet specific customer needs, including different conveying capacities, distances, and environmental conditions. The company's expertise in powder handling technology enables the development of tailored solutions that address the unique challenges of each application.
Conclusion and Future Outlook
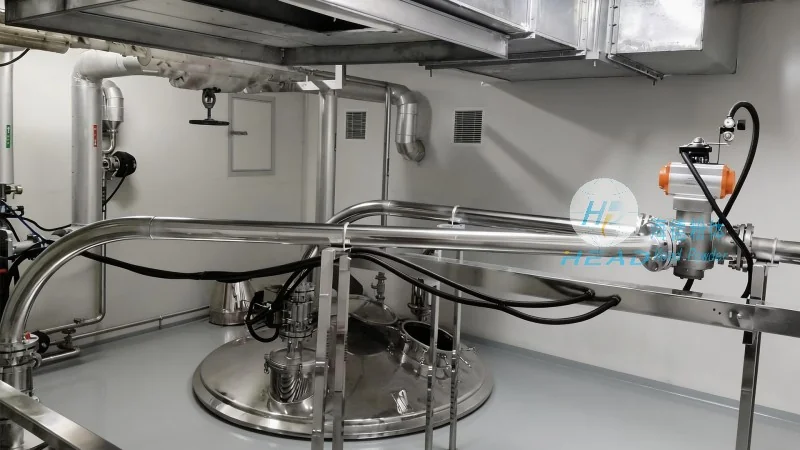
Glucose powder pneumatic conveying systems are essential for efficient and safe transportation of glucose powder in various industrial applications. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and improve its systems, providing reliable solutions that meet the evolving needs of the industry. With a focus on quality, performance, and customer satisfaction, HeadPowder remains a trusted partner for businesses seeking advanced powder handling solutions. The company's commitment to research and development ensures that its products remain at the forefront of technological advancements, contributing to the growth and success of its clients.