

Working Principle and Features of Sugar Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment tailored for the sugar industry. This article explores the fundamental working principles and distinctive features of sugar pneumatic conveying systems, highlighting how these technologies enhance efficiency and reliability in sugar processing operations.
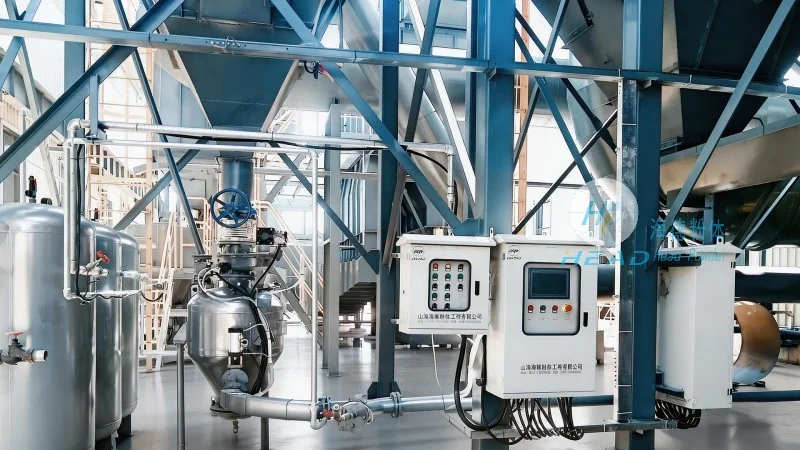
Working Principle of Pneumatic Conveying Systems for Sugar
Pneumatic conveying equipment for sugar operates by transporting bulk materials, such as raw sugar, refined sugar, or sugar crystals, through a pipeline using air or gas as the conveying medium. The system typically consists of a hopper, a rotary valve, a conveying line, and a receiver. When the material is fed into the hopper, it is drawn into the conveying line by the air flow generated by a blower or compressor. The air flow creates a negative pressure in the line, which pulls the sugar particles along the pipeline. The speed and pressure of the air are carefully controlled to ensure smooth and efficient transport without causing material degradation or blockages.
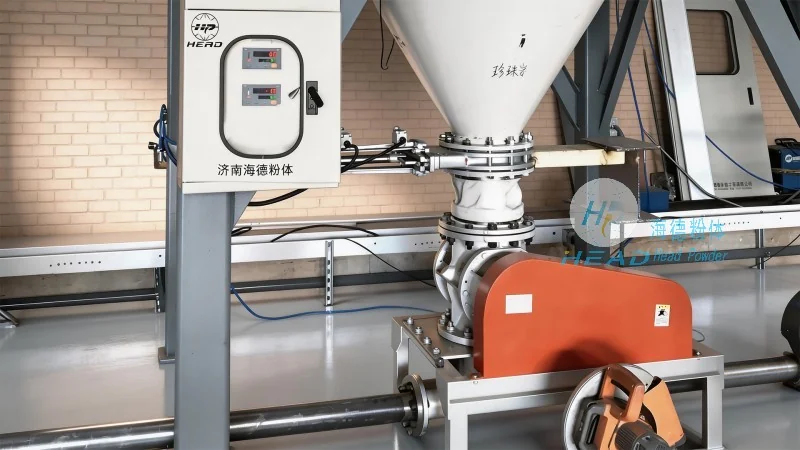
There are two main types of pneumatic conveying systems used in the sugar industry: dilute-phase and dense-phase. Dilute-phase systems use lower air velocities and higher material concentrations, making them suitable for short-distance transport. Dense-phase systems employ higher air pressures and lower material concentrations, ideal for longer distances or when handling sensitive materials. The choice between these systems depends on the specific requirements of the sugar processing plant, including the distance between the source and destination, the material characteristics, and the desired flow rate.
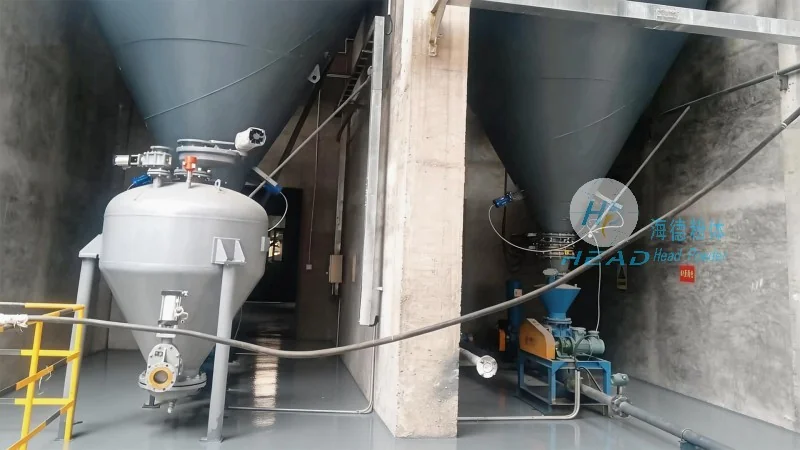
Key Features of Sugar Pneumatic Conveying Equipment
Modern sugar pneumatic conveying equipment from HeadPowder is designed with several key features that enhance performance and durability. These include: Advanced Control Systems, which allow precise regulation of air pressure, flow rate, and material feed, ensuring consistent operation and minimizing downtime. Corrosion-Resistant Materials, such as stainless steel and special alloys, are used to withstand the acidic and humid conditions commonly found in sugar processing environments, extending the equipment's service life. Energy-Efficient Design, with optimized blower and compressor configurations, reduces operational costs while maintaining high conveying efficiency. Easy Maintenance and Cleaning, featuring accessible components and CIP (Clean-In-Place) systems, simplifies routine maintenance and adheres to strict hygiene standards required in the food industry.
Application Scenarios and Benefits
Sugar pneumatic conveying systems are widely used in various stages of sugar production, including raw sugar handling, refining, and packaging. In raw sugar processing, the equipment efficiently transports sugar beets or cane juice residues from storage silos to processing units. During refining, it conveys refined sugar crystals from the crystallization tanks to storage silos or packaging lines. The benefits of using pneumatic conveying for sugar include: Reduced Labor Costs, as automated systems minimize manual handling of heavy or dusty materials. Improved Product Quality, as the enclosed system prevents contamination and moisture absorption, preserving the purity of the sugar. Enhanced Safety, as the enclosed pipeline eliminates the risk of dust explosions and exposure to harmful particles. Space Efficiency, as the equipment can be installed in compact areas, saving valuable floor space in processing facilities.
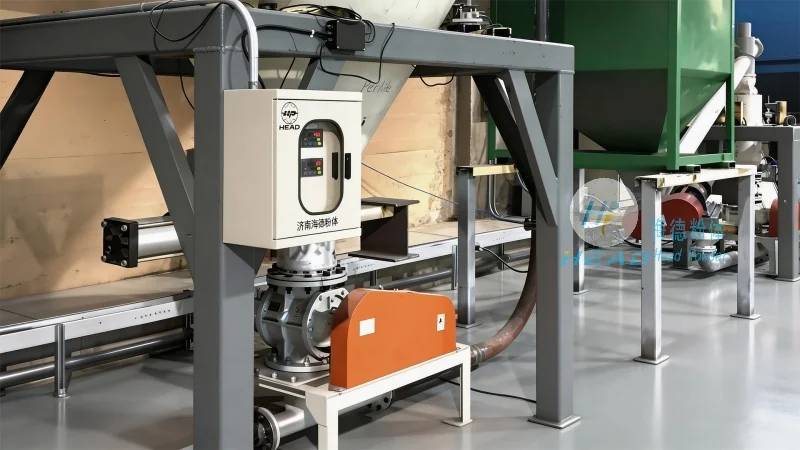
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, headquartered in Shandong, China, is a reputable engineering company dedicated to providing high-quality pneumatic conveying solutions for the sugar industry. With years of experience and a team of skilled engineers, the company has developed a comprehensive range of equipment tailored to meet the unique needs of sugar processing plants. HeadPowder's commitment to innovation and customer satisfaction has earned it a strong reputation in the industry, with clients worldwide relying on their products for reliable and efficient material handling. The company's facilities in Shandong are equipped with advanced manufacturing capabilities, ensuring strict quality control and timely delivery of products to meet global market demands.