

Working Principle and Features of Fine Light Sand Material Pneumatic Conveying Systems
When it comes to the efficient and reliable transportation of fine light sand materials, pneumatic conveying systems offer a sophisticated solution that combines advanced technology with practical application. These systems are designed to handle materials like fine light sand, which are often characterized by their small particle size and light weight, making traditional methods of material handling less effective. The core of such systems lies in their ability to use air as the conveying medium, enabling the material to be transported through a network of pipes and ducts without the need for mechanical components like belts or buckets.
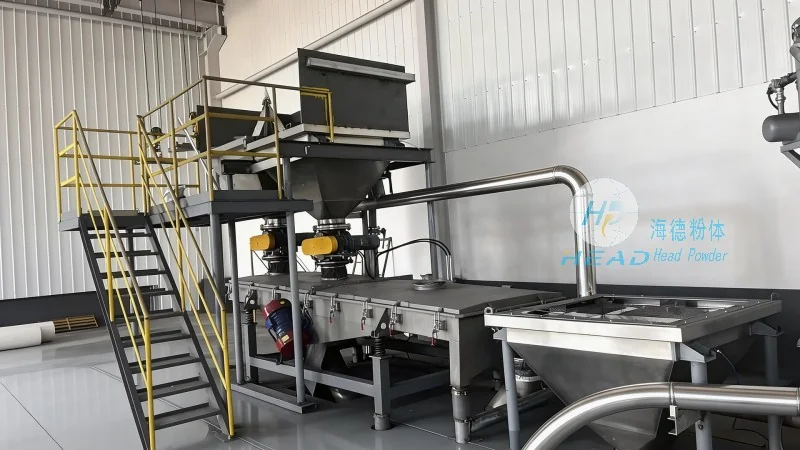
Working Principle of Fine Light Sand Material Pneumatic Conveying Systems
The working principle of a fine light sand material pneumatic conveying system is based on the fundamental concept of transporting solid particles using a gas stream. In this system, the fine light sand is introduced into a hopper or feeder, where it is then drawn into a pipeline by a high-pressure air stream generated by a blower or compressor. The air and sand mixture travels through the pipeline under pressure, with the air providing the necessary force to move the particles. The system typically includes components such as a feed hopper, a rotary valve or feeder, a blower or compressor, a pipeline network, and a discharge point or receiver. The air flow is controlled to ensure that the material is conveyed at an optimal velocity, preventing issues like clogging or particle degradation. The pressure and flow rate are carefully regulated to maintain the stability of the material stream and ensure efficient transport. This principle allows for a continuous and automated process, reducing manual labor and enhancing operational efficiency.
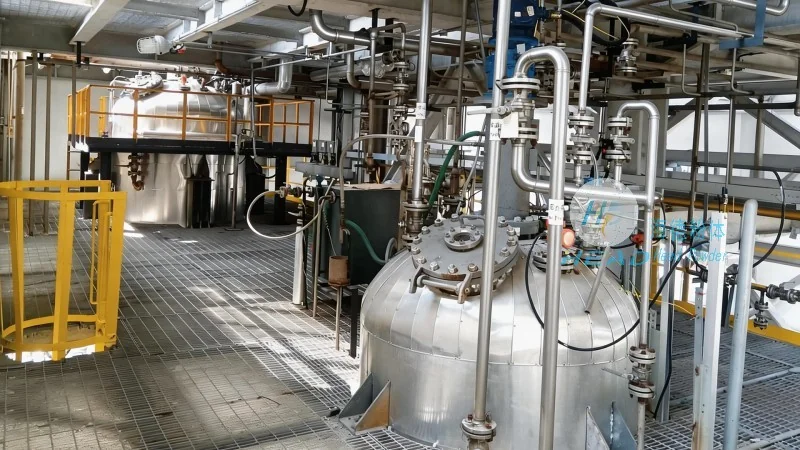
Key Features of Fine Light Sand Material Pneumatic Conveying Systems
Fine light sand material pneumatic conveying systems are distinguished by several key features that make them ideal for handling delicate and light-weight materials. One of the primary features is their ability to handle fine particles without causing damage or segregation. The system's design minimizes the risk of particle breakage, which is crucial for maintaining the quality of the fine light sand. Another important feature is the system's flexibility in terms of layout and installation. Pneumatic conveying systems can be configured to fit various plant layouts, with the ability to route the material through complex pipe networks to reach different processing or storage locations. The systems also offer high efficiency in terms of material transport, with minimal energy loss compared to other methods. Additionally, they provide a clean and hygienic operation, as the material is contained within the pipeline, reducing dust and contamination. The systems are also relatively low in maintenance, as they have fewer moving parts compared to mechanical conveyors, which reduces the risk of breakdowns and maintenance costs. Furthermore, the ability to control the flow rate and pressure allows for precise control over the material's movement, ensuring that the process is optimized for the specific requirements of the fine light sand material being handled.
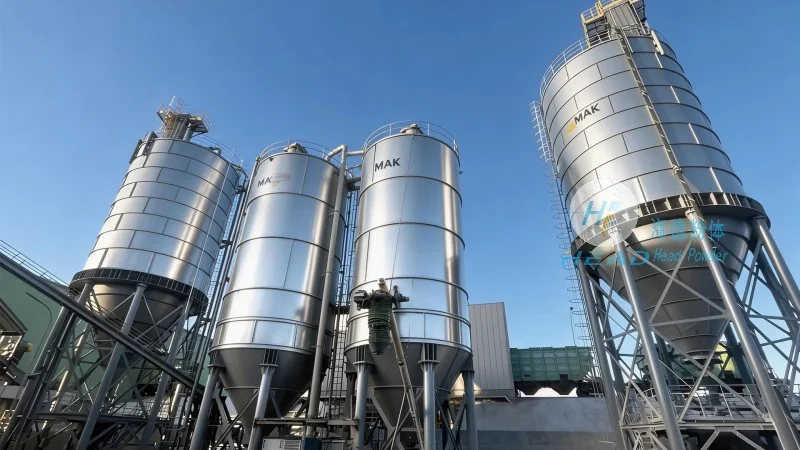
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of material handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and supply of pneumatic conveying systems tailored for various industrial applications. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses dealing with fine light sand and other similar materials. The company's expertise lies in the development of customized solutions that meet the specific needs of clients, ensuring that the systems are optimized for efficiency, reliability, and cost-effectiveness. HeadPowder's team of engineers and technicians work closely with clients to understand their operational requirements and provide tailored solutions that enhance productivity and reduce operational costs. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing procedures, ensuring that all products meet the highest performance and safety requirements. HeadPowder's pneumatic conveying systems are designed to deliver long-term performance and durability, with components that are built to withstand the demands of industrial environments. The company's customer-centric approach and technical support ensure that clients receive comprehensive solutions and assistance throughout the entire process, from system design and installation to maintenance and after-sales support.