

Working Principle and Characteristics of High-Temperature Fine Powder Material Pneumatic Conveying S
Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced pneumatic conveying solutions for high-temperature fine powder materials. Our systems are engineered to handle challenging applications where conventional methods may fall short. This article explores the fundamental working principle and key characteristics of our high-temperature fine powder pneumatic conveying systems, designed to meet the demands of modern industrial processes.
Understanding the Working Principle of High-Temperature Pneumatic Conveying Systems
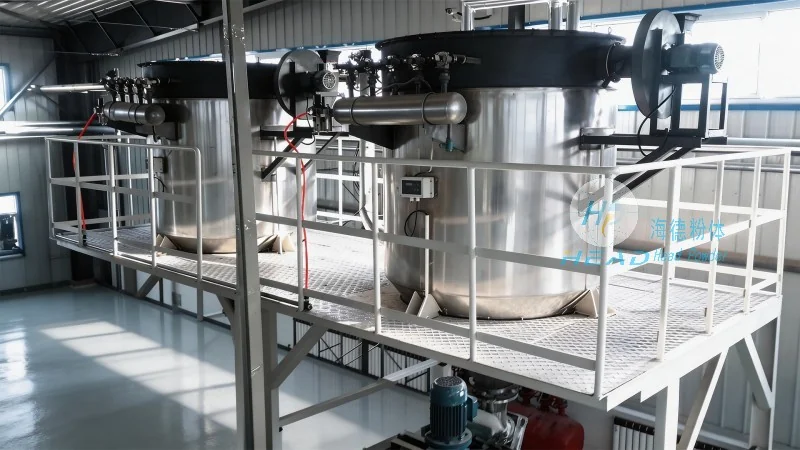
At the core of our high-temperature fine powder pneumatic conveying systems is a sophisticated mechanism that efficiently transports fine powders over long distances while maintaining temperature stability. The system operates on the principle of air pressure, utilizing a combination of positive and negative pressure zones to move material through a network of pipes. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. A high-pressure air stream, generated by a blower or compressor, propels the powder particles through the pipeline. The air velocity is carefully controlled to ensure that the powder remains suspended and transported without clogging or degradation. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational reliability. The system's design incorporates heat-resistant materials and insulation to prevent heat loss or gain, ensuring that the material's temperature is maintained throughout the conveying process. This is particularly critical for materials that are sensitive to temperature fluctuations, such as certain industrial powders used in pharmaceuticals, food processing, or chemical manufacturing.
Key Characteristics of High-Temperature Fine Powder Pneumatic Conveying Systems
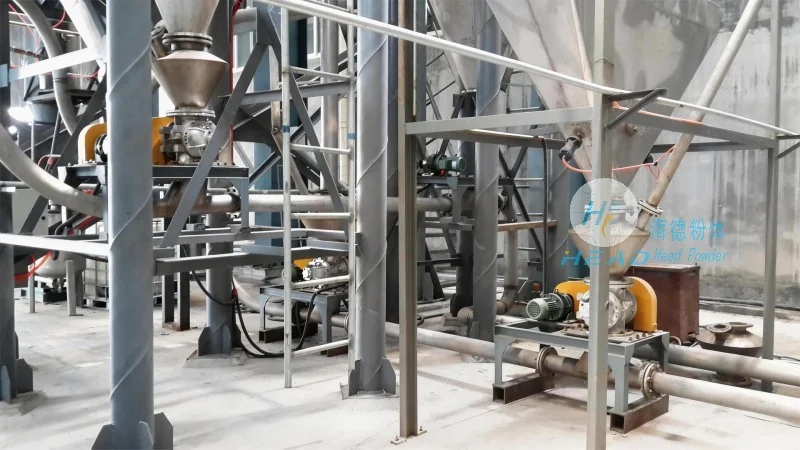
Our high-temperature fine powder pneumatic conveying systems exhibit several distinct characteristics that set them apart from traditional conveying methods. Firstly, they offer a high degree of flexibility in terms of material handling. The systems can transport a wide variety of fine powders, including those with varying particle sizes, densities, and moisture content. This adaptability makes them suitable for diverse industrial applications, from cement and coal to pharmaceutical powders and food additives. Secondly, the systems provide excellent control over the conveying process. By adjusting the air pressure and flow rate, operators can precisely regulate the speed and volume of material transport. This level of control is essential for maintaining consistent product quality and preventing overloading or underloading of downstream equipment. Thirdly, the systems are highly efficient in terms of energy consumption. Compared to mechanical conveying systems, pneumatic systems can achieve lower energy costs due to the reduced need for moving parts and the ability to operate with lower air pressures. Additionally, the systems offer a compact design, requiring less floor space and installation complexity. This makes them ideal for retrofitting into existing facilities or for new plant constructions where space is limited. Fourthly, the systems provide superior material handling capabilities, especially for fine powders that are prone to dusting or caking. The air stream helps to keep the material in a suspended state, preventing blockages and ensuring smooth flow. This reduces downtime and maintenance costs, as the system is less susceptible to material buildup in the pipes. Finally, the systems are designed with safety and environmental considerations in mind. The use of enclosed pipelines and proper filtration systems minimizes dust emissions and ensures compliance with environmental regulations. The materials used in the construction of the system components are heat-resistant and durable, ensuring long-term performance and reliability.
Applications and Benefits in Industrial Settings
The high-temperature fine powder pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. are widely used in various industrial sectors due to their versatility and efficiency. In the cement industry, these systems are employed to transport raw materials and finished products, such as clinker and cement powders, over long distances with minimal temperature loss. In the chemical industry, they are used to handle sensitive chemicals that require temperature control during transport. The pharmaceutical industry benefits from the system's ability to maintain sterile conditions and prevent contamination, as the enclosed design and filtration systems ensure that the material remains clean and free from particulate matter. In the food processing industry, the systems are used to transport food-grade powders, such as sugar, flour, and spices, while maintaining hygiene standards. The benefits of these systems extend beyond material transport; they also contribute to improved operational efficiency and reduced maintenance costs. By eliminating the need for mechanical components and reducing downtime, the systems provide a reliable solution for industries that rely on consistent and high-quality material handling. The compact design and energy efficiency further enhance the economic viability of the systems, making them a cost-effective choice for long-term industrial applications.
Conclusion and Company Overview
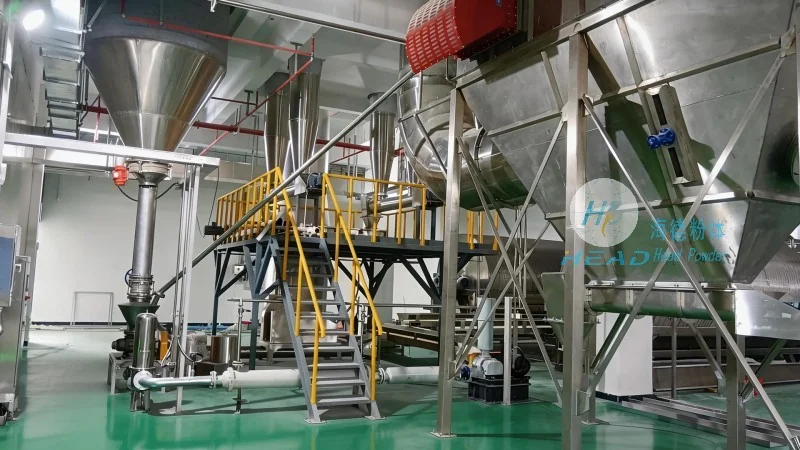
Shandong HeadPowder Engineering Co., Ltd. is committed to providing innovative and reliable high-temperature fine powder pneumatic conveying systems that meet the evolving needs of modern industry. Our systems are designed with precision engineering and rigorous testing to ensure optimal performance and durability. With a focus on customer satisfaction and technological advancement, we continue to develop solutions that enhance the efficiency and safety of material handling processes. Based in Shandong, China, our company leverages local expertise and resources to deliver high-quality products and services to clients worldwide. Whether you are in the cement, chemical, pharmaceutical, or food industry, our high-temperature fine powder pneumatic conveying systems offer a superior solution for your material transport needs. Contact us today to learn more about how our systems can improve your operational efficiency and product quality.