

Working Principle and Features of a Pneumatic Conveying System for Carbon Black and Coal Powder Mate
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for handling carbon black and coal powder materials. This article explores the fundamental working principle and key features of such systems, providing a comprehensive overview for industry professionals and potential clients.
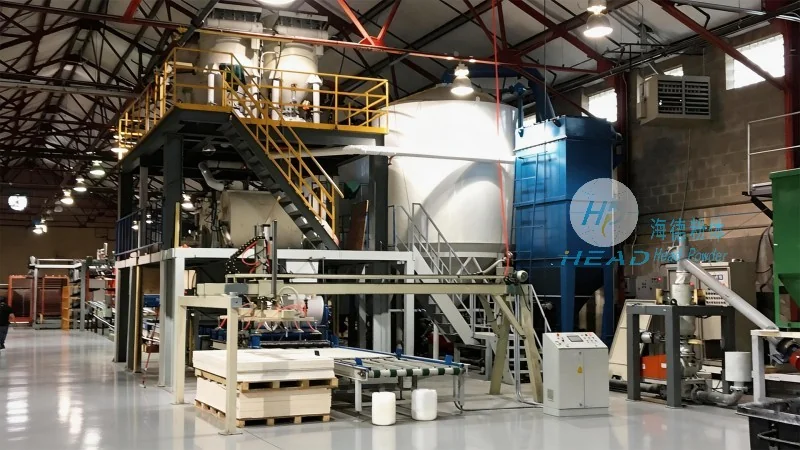
Understanding the Working Principle of Pneumatic Conveying Systems
A pneumatic conveying system for carbon black and coal powder materials operates by utilizing air or gas as the primary medium to transport bulk materials from one location to another. The core mechanism involves the creation of a pressure differential, typically through a blower or compressor, which generates the necessary force to move the particulate materials through a pipeline network. The system generally consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the deposited material. The process begins when the material is discharged from the hopper into the feeder, which then feeds the material into the conveying line under the pressure of the moving air. As the air flows through the pipeline, it entrains the particles, carrying them to the destination point. The receiver then collects the material as the air is separated and either recirculated or discharged, depending on the system design.
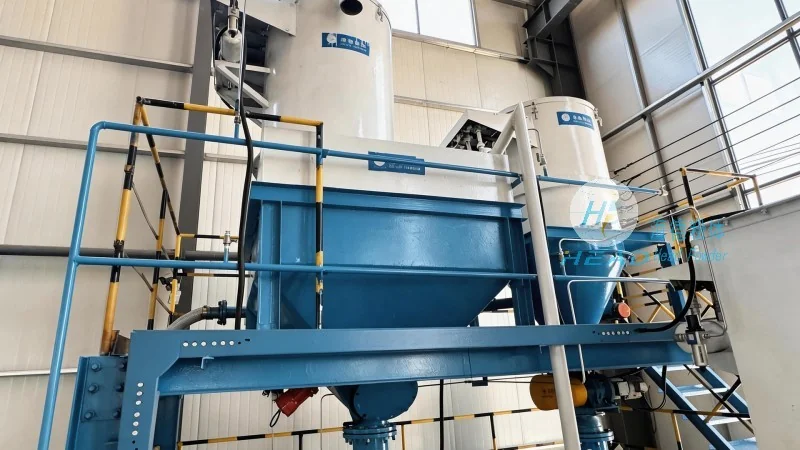
Key Features of Pneumatic Conveying Systems for Carbon Black and Coal Powder
Systems designed for carbon black and coal powder materials exhibit several distinct features that enhance their efficiency and adaptability. One of the primary advantages is the ability to handle fine, abrasive, and potentially explosive materials without the need for mechanical components that could cause wear or contamination. The enclosed pipeline system minimizes dust emissions, ensuring compliance with environmental regulations and providing a safer working environment. Additionally, these systems offer high transport capacity and can cover long distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators. The flexibility of the system allows for multiple inlets and outlets, enabling complex material routing and integration with existing industrial processes. Another notable feature is the ability to control the flow rate precisely, which is crucial for maintaining consistent material quality and preventing overloading or underloading of downstream equipment. The system's design also incorporates safety features such as pressure relief valves and explosion-proof components, ensuring operational safety in handling potentially hazardous materials like carbon black.
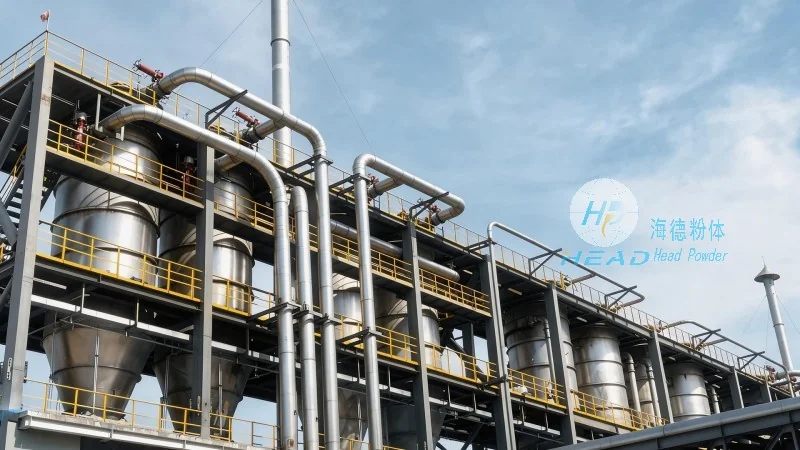
Technical Advantages and Application Considerations
The pneumatic conveying system for carbon black and coal powder materials offers several technical advantages that make it an ideal choice for industrial applications. The enclosed nature of the system prevents material loss and contamination, which is critical for maintaining product purity in sensitive processes. The use of air as the conveying medium allows for gentle handling of the materials, reducing particle degradation and preserving their physical properties. This is particularly important for carbon black, where particle size and surface area are critical for end-use applications. Furthermore, the system's modular design facilitates easy installation and maintenance, with components that can be replaced or upgraded without disrupting the entire operation. When considering the application of such a system, factors like material characteristics (e.g., particle size, density, moisture content), required transport distance, and system capacity must be carefully evaluated to ensure optimal performance. The system's scalability allows for customization to meet the unique requirements of different industries, from small-scale operations to large industrial plants.
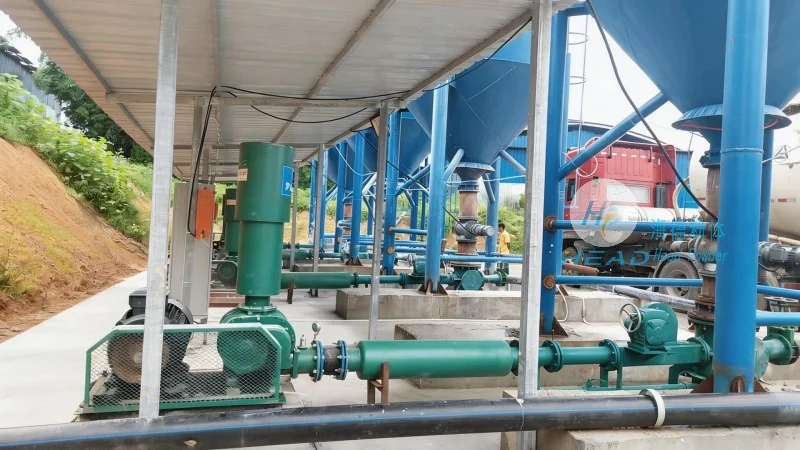
Conclusion
In summary, the pneumatic conveying system for carbon black and coal powder materials is a sophisticated and efficient solution for bulk material handling. Its working principle, based on air pressure and enclosed pipelines, provides a reliable method for transporting fine, abrasive materials while maintaining safety and environmental standards. The key features, including enclosed transport, high capacity, and precise control, make it a preferred choice in various industrial sectors. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise to design and implement tailored solutions that meet the unique requirements of clients, ensuring optimal performance and long-term operational efficiency.