

Working Principle and Features of Vacuum Dilute Phase Material Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced vacuum dilute phase pneumatic conveying systems. These systems are engineered to efficiently transport bulk materials over long distances with minimal pressure differentials, making them ideal for a wide range of industrial applications. The equipment operates under negative pressure, ensuring a safe and controlled environment for material handling while minimizing dust emissions and operational risks.
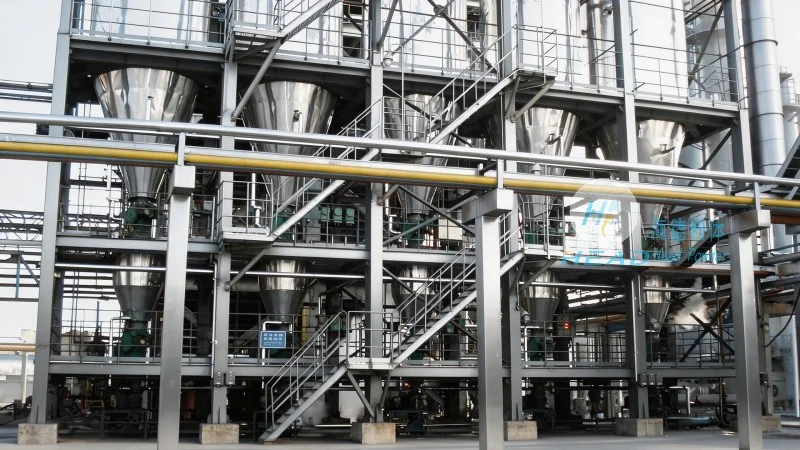
Working Principle of Vacuum Dilute Phase Pneumatic Conveying
The core mechanism of vacuum dilute phase pneumatic conveying involves the use of a vacuum pump to create a pressure differential between the material source and the destination. The system draws material from a hopper or storage silo into a conveying line by creating a negative pressure zone. As the material is drawn into the line, it is mixed with a low velocity air stream, forming a dilute phase mixture. This mixture is then transported through the pipeline to the receiving hopper or processing unit. The process is characterized by continuous flow and the ability to handle a variety of materials, including powders, granules, and fine particles, without the need for mechanical components like augers or belts.
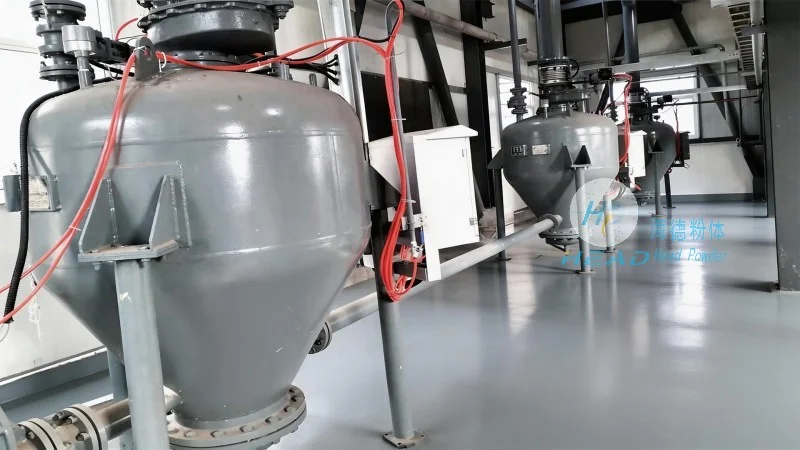
Key Features and Advantages
One of the primary advantages of vacuum dilute phase pneumatic conveying equipment is its ability to operate under low pressure, which reduces energy consumption and operational costs compared to positive pressure systems. The negative pressure environment also enhances safety by preventing dust leakage and minimizing the risk of explosions in hazardous material handling scenarios. Additionally, the system offers high flexibility in terms of layout, as it can be easily integrated into existing production lines or reconfigured for different material types. The equipment is designed for durability and low maintenance, with components such as stainless steel pipelines and robust vacuum pumps that ensure long-term reliability. Another notable feature is the system's capacity to handle materials with varying moisture content and particle sizes, making it suitable for diverse industrial applications such as food processing, pharmaceuticals, and chemical manufacturing.
Application-Specific Benefits
For industries like food and pharmaceuticals, the vacuum dilute phase system provides a hygienic and contamination-free environment, which is critical for maintaining product quality and regulatory compliance. The low velocity air stream minimizes material degradation and ensures that sensitive products are transported without damage. In chemical processing, the system's ability to handle abrasive and corrosive materials is particularly valuable, as it reduces equipment wear and extends the lifespan of components. The system also offers improved process control, as the vacuum level can be precisely adjusted to optimize material flow and prevent blockages in the pipeline. This level of control is essential for maintaining consistent production rates and reducing downtime.
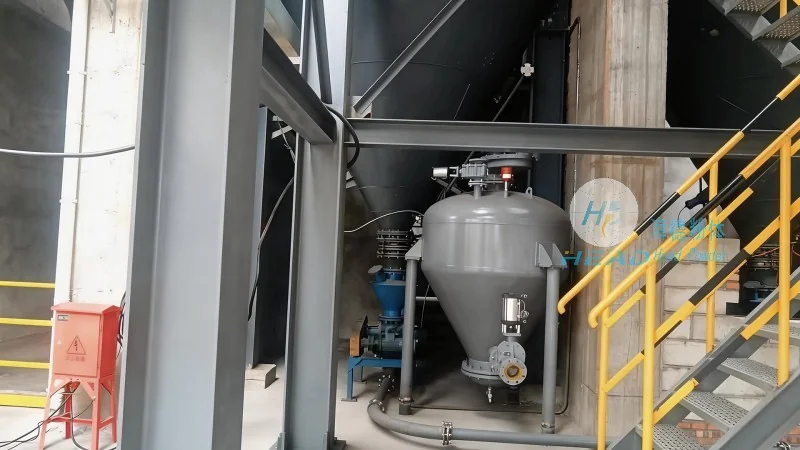
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is committed to delivering high-quality vacuum dilute phase pneumatic conveying equipment that meets the evolving needs of modern industrial operations. By combining advanced engineering with rigorous quality control, the company ensures that its systems deliver reliable performance, energy efficiency, and safety. The company's expertise in material handling technology, coupled with its customer-centric approach, makes it a trusted partner for businesses seeking to enhance their material transport processes. With a focus on innovation and sustainability, HeadPowder continues to develop solutions that improve operational efficiency while reducing environmental impact.