

Principles and Working Scene Characteristics of Bulk Material Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems for bulk materials. These systems are engineered to efficiently transport dry, granular, or powdery materials (such as grains, powders, and other bulk commodities) over long distances with minimal maintenance and operational costs. The core principle of pneumatic conveying lies in using compressed air or gas to create a flow that propels the material through a pipeline network, offering a flexible and automated solution for material handling in various industrial settings.
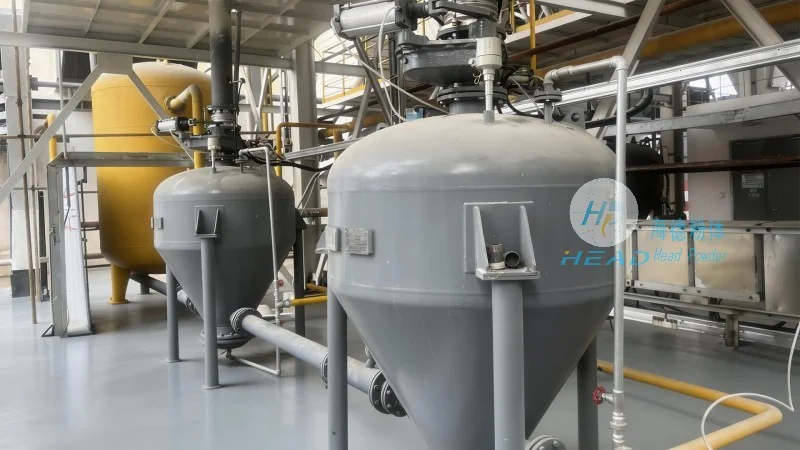
Principles of Pneumatic Conveying Systems
The fundamental principle of pneumatic conveying systems involves the use of a pressure differential to move material. In a typical system, a fan or blower generates compressed air, which is then introduced into a hopper or feeder. The material is then drawn into the air stream and carried through the pipeline to the discharge point. The system can operate under either positive pressure (where air pushes the material) or negative pressure (where air pulls the material), depending on the application requirements. The efficiency of the system is determined by factors such as the material's density, particle size, and the system's pressure and flow rates. HeadPowder's engineers carefully design the system to optimize these parameters, ensuring reliable and consistent material transport. The company's expertise in material characterization and system simulation allows for the development of tailored solutions that meet specific operational needs.
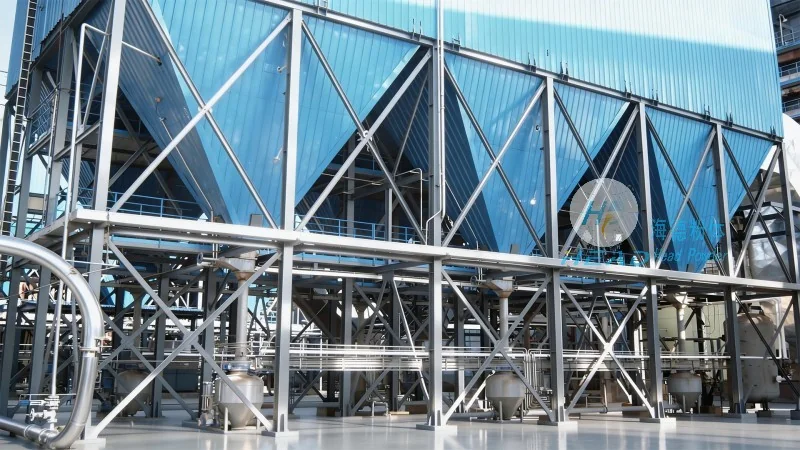
Key Working Scene Characteristics
The working scene characteristics of pneumatic conveying systems are defined by their adaptability to diverse industrial environments. These systems are particularly suited for applications where traditional mechanical conveyors (like belt or screw conveyors) may be impractical due to space constraints, material abrasiveness, or the need for dust-free handling. In grain processing facilities, for example, pneumatic conveying systems are used to transport raw grains from storage silos to processing equipment, ensuring a continuous and hygienic flow. In pharmaceutical and food processing industries, the systems are designed with sanitary components to maintain product purity and compliance with regulatory standards. The systems also excel in chemical and mineral processing plants, where they can handle abrasive or corrosive materials without causing wear or contamination. Another key characteristic is the ability to integrate with existing infrastructure, allowing for retrofits in older facilities or new installations in greenfield projects. HeadPowder's systems are designed to be modular, enabling easy expansion or reconfiguration as production needs evolve.
Advantages in Material Handling Applications
Pneumatic conveying systems offer several advantages over traditional material handling methods. One of the primary benefits is the ability to transport materials over long distances with minimal energy consumption compared to mechanical conveyors. The systems also provide a dust-free and enclosed environment, reducing the risk of contamination and improving workplace safety. Additionally, pneumatic conveyors can handle a wide range of materials, from fine powders to large granules, without the need for multiple equipment types. The flexibility of the system allows for multiple discharge points, enabling the distribution of material to several destinations from a single source. This is particularly useful in large-scale production facilities where material needs to be routed to different processing units or storage areas. The systems also require less floor space compared to traditional conveyors, making them ideal for facilities with limited headroom or space constraints. HeadPowder's systems are equipped with advanced control systems that allow for real-time monitoring and adjustment of flow rates, ensuring optimal performance and preventing system overload or material blockages.
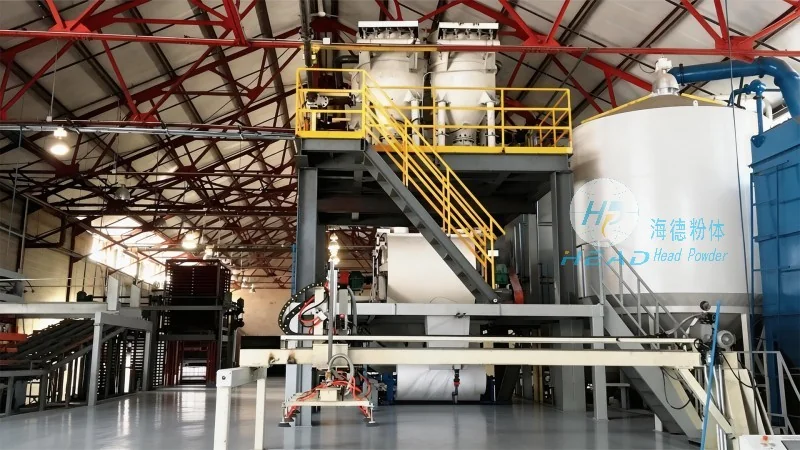
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd. is a professional engineering company headquartered in Shandong, China. The company specializes in the research, development, and manufacturing of pneumatic conveying systems and related equipment for bulk material handling. With years of experience in the industry, HeadPowder has established itself as a trusted provider of high-quality, customized solutions for various industrial sectors. The company's team of engineers and technicians are dedicated to delivering innovative and efficient systems that meet the specific needs of clients. HeadPowder's commitment to quality and customer satisfaction has earned it a reputation as a leading supplier in the market. The company's facilities in Shandong are equipped with state-of-the-art technology and testing equipment, ensuring that all products meet international standards and regulatory requirements. HeadPowder's services include system design, installation, commissioning, and after-sales support, providing clients with a comprehensive solution for their material handling needs.