

Operation Process and Working Principle of High-Pressure Bin Pump Pneumatic Conveying System
High-pressure bin pump pneumatic conveying systems are advanced industrial equipment designed to transport bulk materials efficiently over long distances with minimal maintenance. This system, manufactured by Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, combines the advantages of high-pressure air flow and a bin pump mechanism to achieve reliable material handling. The following sections will detail the operation process and working principle of this system, providing a comprehensive understanding of its functionality and benefits.
Company Introduction
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of high-quality pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a leading provider in the industry. HeadPowder specializes in designing and producing customized solutions for various bulk material handling applications, ensuring optimal performance and durability. The company's headquarters is located in Shandong, China, where state-of-the-art facilities and experienced engineers work together to develop cutting-edge equipment.
Overview of High-Pressure Bin Pump Pneumatic Conveying System
The high-pressure bin pump pneumatic conveying system is a sophisticated piece of machinery that utilizes compressed air to transport dry bulk materials from a storage bin to a discharge point. This system is particularly effective for materials that are difficult to handle using traditional methods, such as powders, granules, and fine particles. The system consists of several key components, including a storage bin, a bin pump, a conveying line, and a control system, all working in harmony to ensure smooth and continuous material flow.
Key Components and Their Functions
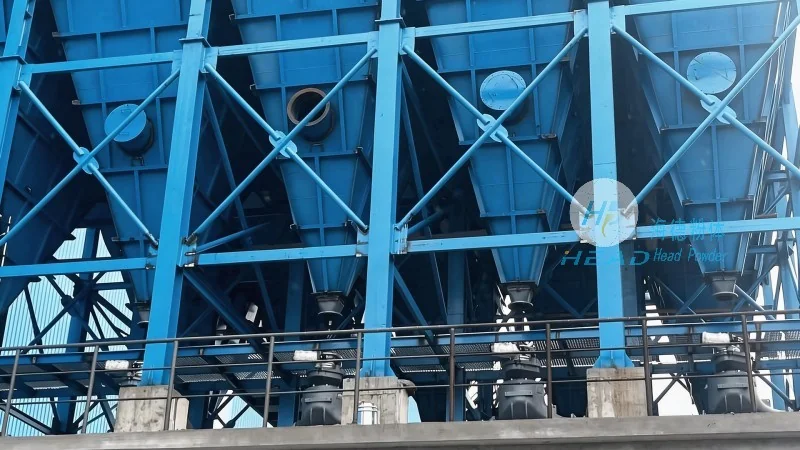
1. **Storage Bin**: The storage bin is the primary container where the bulk material is stored before being conveyed. It is typically made of durable materials like steel or stainless steel to withstand the weight and pressure of the material. The bin is equipped with a hopper or a discharge valve at the bottom to allow controlled material release.
2. **Bin Pump**: The bin pump is the heart of the system, responsible for generating the high-pressure air flow needed to move the material. It operates by creating a vacuum or pressure differential that draws the material into the pump and then forces it through the conveying line. The pump is designed to handle high-pressure conditions, ensuring efficient and reliable material transport.
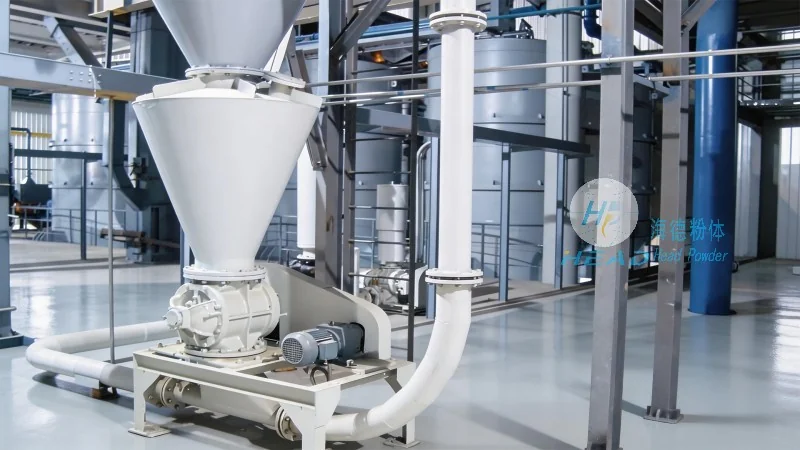
3. **Conveying Line**: The conveying line is a flexible or rigid pipe that connects the storage bin to the discharge point. It is made of materials resistant to the conveyed material and high-pressure air, such as PVC, stainless steel, or rubber. The line is equipped with valves and fittings to control the flow and direction of the material.
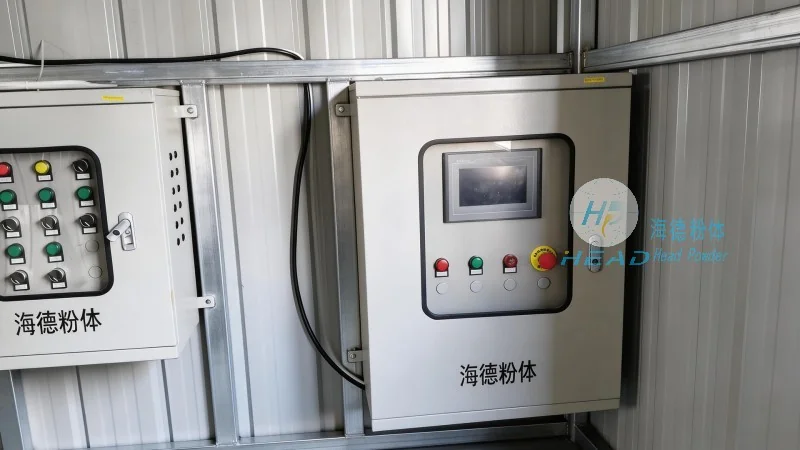
4. **Control System**: The control system manages the operation of the entire system, including the bin pump, conveying line, and material flow. It uses sensors and controls to monitor pressure, flow rate, and material level, ensuring safe and efficient operation. The system can be programmed to start and stop automatically based on material levels or other conditions.
Operation Process of the High-Pressure Bin Pump System
The operation of the high-pressure bin pump pneumatic conveying system involves several steps, each designed to ensure the smooth and continuous transport of bulk materials. The process begins with the material being loaded into the storage bin. Once the bin is filled, the control system activates the bin pump, which starts generating the high-pressure air flow. The material is then drawn from the bin into the pump and pushed through the conveying line to the discharge point. The system continues to operate until the material level in the bin drops below a certain threshold, at which point the pump stops and the system waits for more material to be added.
Working Principle of the High-Pressure Bin Pump System
The working principle of the high-pressure bin pump pneumatic conveying system is based on the principles of fluid dynamics and air pressure. The system operates by creating a pressure differential between the storage bin and the discharge point. The bin pump generates a high-pressure air flow that creates a vacuum in the bin, drawing the material into the pump. The material is then mixed with the air and forced through the conveying line under high pressure. The air and material mixture travels through the line until it reaches the discharge point, where the air is separated from the material and the material is discharged. The air is then recirculated back to the pump, completing the cycle.
Advantages of the High-Pressure Bin Pump Pneumatic Conveying System
High-pressure bin pump pneumatic conveying systems offer several advantages over traditional material handling methods. These include: efficient and continuous material transport, minimal maintenance requirements, ability to handle difficult-to-handle materials, and the ability to transport materials over long distances. The system is also highly flexible, allowing for customization to meet specific application requirements. Additionally, the system is safe and reliable, with built-in safety features to prevent accidents and ensure smooth operation.
Applications of the High-Pressure Bin Pump Pneumatic Conveying System
The high-pressure bin pump pneumatic conveying system is widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. It is particularly suitable for applications where materials need to be transported from a storage bin to a processing or packaging area. The system is also used in industries where hygiene and cleanliness are critical, such as the food and pharmaceutical industries, due to its ability to handle materials without contamination.
Conclusion
High-pressure bin pump pneumatic conveying systems are an essential part of modern industrial material handling. With their efficient operation, reliable performance, and ability to handle a wide range of materials, these systems offer significant benefits to industries that require bulk material transport. Shandong HeadPowder Engineering Co., Ltd. provides high-quality and customized solutions for these systems, ensuring that customers receive the best possible equipment for their specific needs. By understanding the operation process and working principle of this system, users can make informed decisions about its application and maximize its benefits.