

Operation Process and Working Principle of Activated Carbon Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and implementation of advanced activated carbon pneumatic conveying systems. These systems are engineered to efficiently transport activated carbon, a critical material in various industrial applications, ensuring optimal performance and reliability. The company's expertise lies in creating customized solutions tailored to meet the specific needs of clients across different industries, from environmental protection to chemical processing.
Working Principle of Activated Carbon Pneumatic Conveying Systems
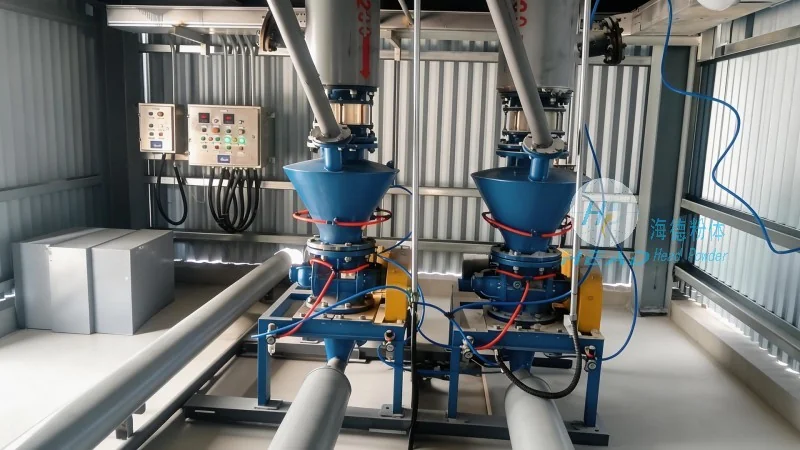
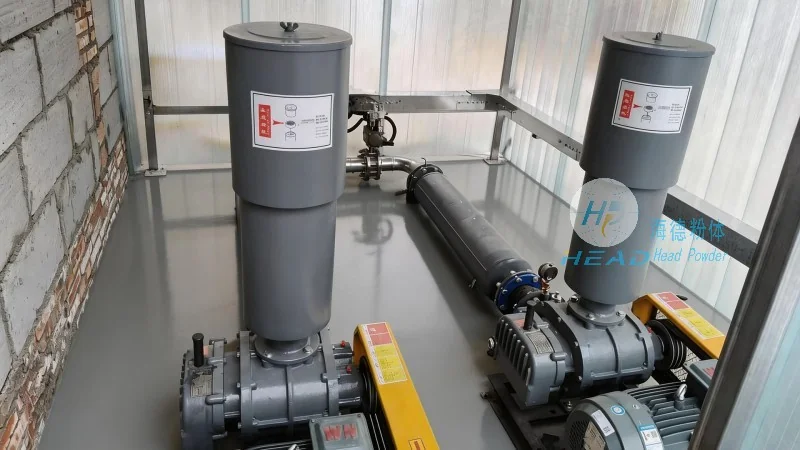
The core of an activated carbon pneumatic conveying system is the pneumatic transport mechanism, which utilizes compressed air to move the material. The process begins with the activated carbon being loaded into a hopper or storage container. From there, the material is drawn into a pipeline by the pressure differential created by the air flow. The system typically employs a combination of positive and negative pressure zones to ensure smooth and controlled movement of the carbon. Key components include the air compressor, which provides the necessary air pressure, the hopper with a feeder or rotary valve to control the material discharge, and the pipeline network that connects the source to the destination. The design of the system is crucial to prevent material degradation, blockages, and ensure consistent flow rates. By leveraging the principles of fluid dynamics and material handling, these systems achieve high efficiency in transporting activated carbon over varying distances and heights.
Operation Process of Activated Carbon Pneumatic Conveying Systems
The operation of an activated carbon pneumatic conveying system involves several sequential steps that ensure the material is transported safely and effectively. First, the system is activated by starting the air compressor, which generates the required pressure. Simultaneously, the feeder mechanism in the hopper is engaged to release the activated carbon into the pipeline. The compressed air then propels the carbon through the pipeline, maintaining a consistent flow rate. During transit, the system monitors pressure and flow parameters to detect any anomalies, such as blockages or pressure drops, which may indicate issues with the material or equipment. At the destination, the carbon is discharged into a receiving vessel or processing unit. The system then returns to standby mode until the next batch is initiated. This cycle is repeated as needed, with the system capable of handling continuous or batch operations depending on the application requirements. The efficiency of the operation is enhanced by the system's ability to maintain consistent air pressure and material feed, minimizing downtime and maximizing throughput.

Advantages of Activated Carbon Pneumatic Conveying Systems
Activated carbon pneumatic conveying systems offer several advantages over traditional material handling methods, making them a preferred choice for many industries. One of the primary benefits is the ability to transport activated carbon in a dust-free environment, which is critical for maintaining product quality and ensuring compliance with environmental regulations. The system's enclosed design prevents the release of fine particles, reducing the risk of contamination and improving workplace safety. Additionally, these systems are highly flexible, allowing for easy integration into existing production lines and the ability to transport materials over long distances without the need for multiple transfer points. The use of compressed air also enables precise control over the flow rate, ensuring that the activated carbon is delivered at the exact rate required by downstream processes. Another advantage is the reduced labor costs associated with manual handling, as the system automates the entire transport process. Furthermore, the system's compact design and minimal maintenance requirements contribute to lower operational costs over time. These benefits make activated carbon pneumatic conveying systems a cost-effective and efficient solution for material handling in various industrial applications.
Applications of Activated Carbon Pneumatic Conveying Systems
Activated carbon pneumatic conveying systems are widely used in a variety of industries due to their versatility and efficiency. In the environmental sector, these systems are crucial for transporting activated carbon used in water treatment and air purification processes. The ability to handle large volumes of carbon efficiently ensures that treatment facilities can maintain optimal filtration performance. In the chemical industry, the systems are used to transport activated carbon for adsorption processes, where the material is used to remove impurities from liquids and gases. The consistent flow and dust-free operation of the system help maintain the purity of the final products. The food and beverage industry also benefits from these systems, as they are used to transport activated carbon for filtration and deodorization of beverages. The pharmaceutical industry utilizes the systems for transporting activated carbon in drug manufacturing processes, where product quality and purity are paramount. Additionally, the systems are employed in the petrochemical industry for the removal of contaminants from oil and gas products. The adaptability of the system to different materials and applications makes it a valuable asset in various industrial settings.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a reputable company based in China, dedicated to providing high-quality activated carbon pneumatic conveying systems. With years of experience in the industry, the company has established itself as a trusted provider of reliable and efficient material handling solutions. The company's commitment to innovation and customer satisfaction has led to the development of advanced systems that meet the evolving needs of clients. HeadPowder's team of experts works closely with clients to understand their specific requirements and design customized solutions that enhance operational efficiency. The company's facilities are equipped with state-of-the-art technology and quality control measures to ensure that every system meets the highest standards. HeadPowder's presence in China, with its strategic location, allows for efficient delivery and support to clients across the region. The company's reputation for excellence and reliability has made it a preferred choice for businesses seeking dependable material handling solutions.