

Operation Process and Working Principle of Barley Pneumatic Conveying System Equipment
Barley, as a key agricultural product, plays a vital role in the food and beverage industry. The efficient handling and transportation of barley are crucial for ensuring the quality and consistency of downstream processes. The pneumatic conveying system for barley, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution that optimizes the entire workflow from storage to processing. This equipment is designed to handle the unique characteristics of barley, such as its size, density, and moisture content, while maintaining high operational efficiency and reliability.
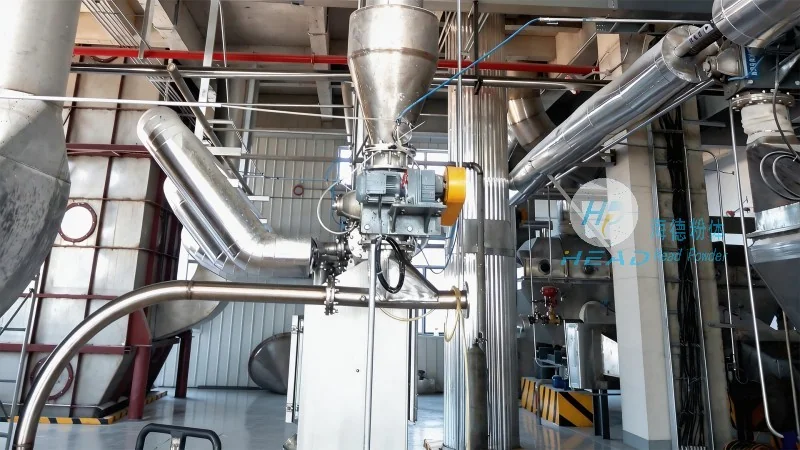
Company Overview
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder and bulk material handling systems, specializes in providing customized solutions for various industries. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable equipment for material transportation. HeadPowder's facilities are located in Shandong, China, where the company leverages advanced technology and skilled engineering teams to deliver top-tier products. The company's commitment to customer satisfaction and technical excellence is reflected in the robust design and performance of its pneumatic conveying systems.
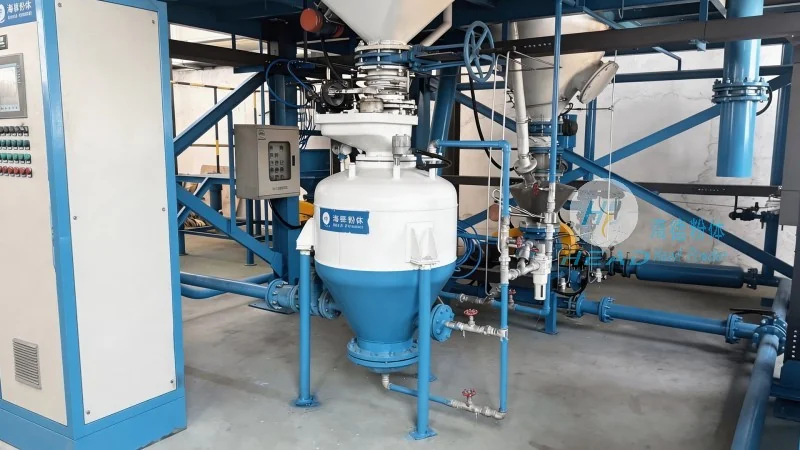
Working Principle of the Barley Pneumatic Conveying System
The core of the barley pneumatic conveying system is the air-based transport mechanism, which utilizes compressed air to move barley particles through a network of pipes. The system operates on the principle of creating a pressure differential between the inlet and outlet of the conveying line. When the system is activated, a fan or blower generates high-pressure air, which is then introduced into the hopper containing the barley. The barley is then drawn into the air stream and carried through the pipeline to the destination point, such as a silo or processing unit. This method eliminates the need for mechanical components like belts or buckets, reducing wear and tear and maintenance costs.
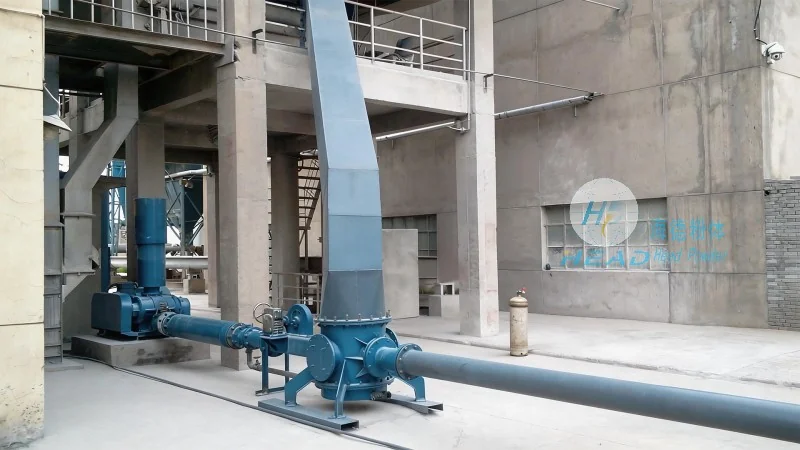
Operation Process of the Barley Pneumatic Conveying System
The operation of the barley pneumatic conveying system involves several key steps that ensure smooth and continuous material transport. First, the barley is loaded into the hopper, which is equipped with a feeding mechanism to control the flow rate. The system is then started by activating the air compressor or blower, which generates the necessary air pressure. As the air flows through the pipeline, it creates a suction effect that pulls the barley particles into the system. The barley is then conveyed through the pipeline to the receiving vessel, where it is discharged. The system includes control valves and sensors that monitor the pressure, flow rate, and level of the material, allowing for real-time adjustments to maintain optimal performance. The entire process is automated, minimizing the need for manual intervention and ensuring consistent operation.
Key Features and Advantages
Shandong HeadPowder Engineering Co., Ltd.'s barley pneumatic conveying system offers several advantages that make it an ideal choice for agricultural and food processing applications. The system is designed to handle the delicate nature of barley, preventing breakage or damage during transport. The air-based method reduces the risk of contamination and cross-contamination, which is critical in food processing environments. Additionally, the system is highly efficient, with low energy consumption and minimal material loss. The modular design allows for easy installation and integration into existing facilities, and the robust construction ensures long-term durability and reliability. The system also includes safety features such as pressure relief valves and emergency shut-off mechanisms to protect operators and equipment from potential hazards.
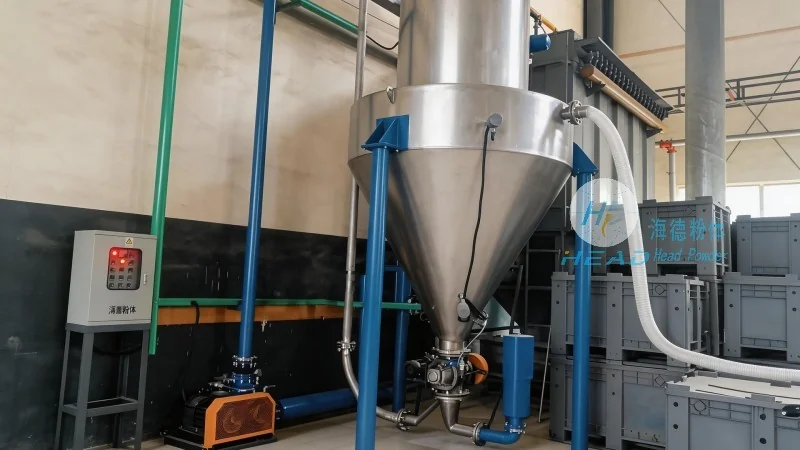
Conclusion
The pneumatic conveying system for barley by Shandong HeadPowder Engineering Co., Ltd. is a cutting-edge solution that addresses the challenges of efficient and safe barley transportation. By leveraging advanced technology and engineering expertise, the company has developed a system that meets the highest standards of performance and reliability. The system's operation process and working principle are designed to optimize material flow while minimizing operational costs. For businesses in the agricultural and food industry, this equipment provides a reliable and efficient means of handling barley, ensuring consistent quality and productivity. With its commitment to quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. continues to be a leader in the development of innovative material handling solutions.