

Operation Process and Working Principle of Small Stone Powder Conveying System
Small stone powder conveying systems are critical components in industrial material handling, ensuring efficient and reliable transport of fine powders like small stones. These systems are designed to handle various applications, from mining and construction to chemical processing, where precise and consistent material movement is essential for operational efficiency. The system's design and functionality directly impact production throughput, safety, and overall process reliability.
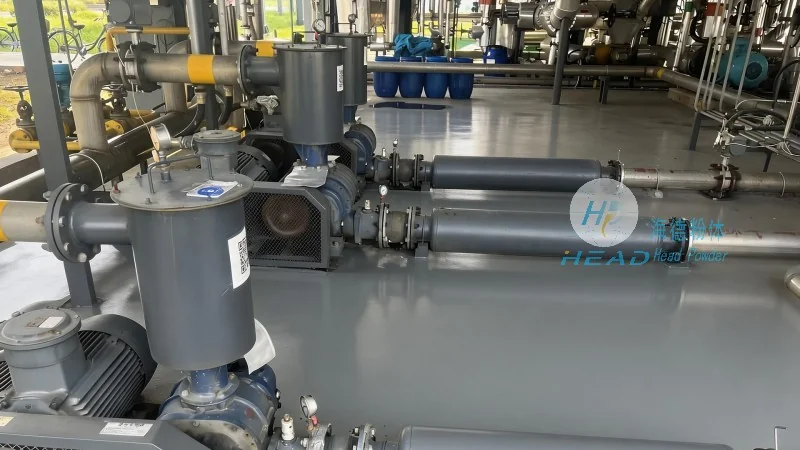
Overview of the Small Stone Powder Conveying System
The small stone powder conveying system is a sophisticated piece of industrial equipment designed to transport small stone powders from one location to another. The system typically consists of several key components, including a hopper for material storage, a feeding mechanism to regulate the flow, a conveying device (such as a screw conveyor, pneumatic conveyor, or belt conveyor), and a control panel for monitoring and adjusting operations. The design is tailored to the specific characteristics of the small stone powder, including particle size, density, and moisture content, to ensure optimal performance and minimize material degradation.
Key Components and Their Functions
The hopper is the primary storage unit, responsible for holding the raw small stone powder and maintaining a consistent feed rate. It is often equipped with a discharge valve or gate to control the flow of material into the conveying system, preventing overloading and ensuring smooth operation. The feeding mechanism, such as a rotary valve or feeder, regulates the amount of material entering the conveyor, adjusting the flow rate based on system requirements. The conveying device, which can be a screw conveyor, pneumatic conveyor, or belt conveyor, is the core component responsible for transporting the material through the system. For small stone powders, a screw conveyor is commonly used due to its ability to handle abrasive materials and maintain a consistent flow, while minimizing material degradation. The control panel allows operators to monitor system parameters, adjust speed, and respond to any issues that may arise during operation, ensuring the system operates at peak efficiency.
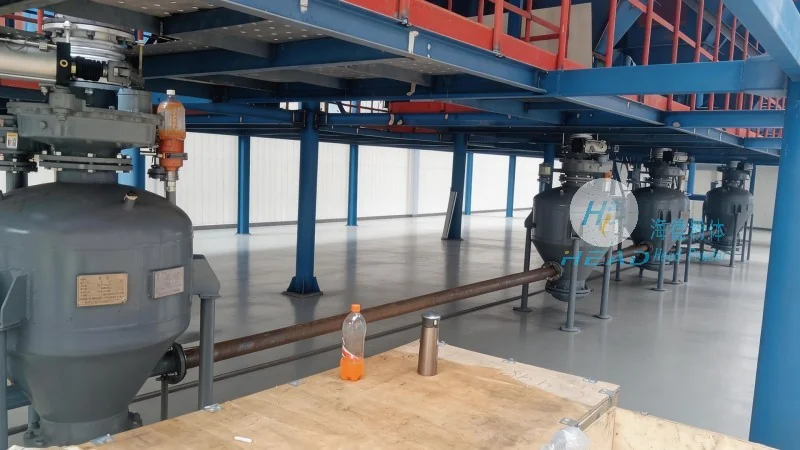
Operation Process of the Small Stone Powder Conveying System
The operation of the small stone powder conveying system follows a systematic process, starting with material loading and ending with delivery at the destination. The process begins with the loading of small stones into the hopper. The material is then discharged from the hopper into the feeding mechanism, which regulates the flow rate to match the conveying device's capacity. The regulated material is fed into the screw conveyor, which transports it through the system using rotational force. The conveyor moves the material along the designated path, ensuring it reaches the discharge point. The control panel continuously monitors the system's performance, adjusting the screw speed as needed to maintain a consistent flow rate. The entire process is automated, minimizing human intervention and reducing the risk of errors, thereby enhancing operational efficiency and productivity.
Working Principle of the Small Stone Powder Conveying System
The working principle of the small stone powder conveying system is based on mechanical force, specifically the rotation of a screw within a tube. The screw's pitch and rotational speed determine the conveying capacity and material flow rate. As the screw rotates, it pushes the small stone powder forward along the tube, using gravity and mechanical force to move the material. The system is designed to handle abrasive materials like small stones, with the screw and tube constructed from durable materials to withstand wear and tear. The control panel monitors the system's performance, adjusting parameters to maintain optimal operation and prevent issues such as blockages or overloading. For pneumatic conveying systems, the principle involves the use of air pressure to move the material through a pipeline. The material is suspended in the air stream and transported to the destination, using a blower or compressor to generate the air pressure. The choice of system depends on the material characteristics, such as particle size and moisture content, and the distance to be covered.
Benefits and Applications of the Small Stone Powder Conveying System
The small stone powder conveying system offers several key benefits, including high efficiency, low maintenance costs, and versatility. The system is designed to handle a wide range of materials, from fine powders to small stones, making it suitable for various industrial applications. The automated operation reduces labor costs and minimizes human error, improving overall productivity and quality control. The system ensures consistent material flow, which is crucial for maintaining uniform product quality in production processes. Additionally, the system is engineered for safety, with features such as overload protection, emergency stop buttons, and material flow monitoring to prevent accidents and ensure operator safety. The small stone powder conveying system is widely used in industries such as mining, construction, chemical processing, and food processing, where material handling is a critical component of the production workflow. It enhances operational efficiency by reducing downtime and improving material transport reliability.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer and supplier of small stone powder conveying systems and related industrial equipment. The company is headquartered in Shandong, China, and has established a strong reputation for producing high-quality, reliable, and efficient systems tailored to the needs of various industries. Headpowder specializes in designing and manufacturing customized conveying solutions, ensuring that each system meets the specific requirements of its clients. The company's products are known for their durability, low maintenance, and excellent performance, making them a preferred choice for industrial applications. Headpowder's team of experienced engineers and technicians work closely with clients to understand their operational challenges and develop innovative solutions that enhance productivity and reduce costs. The company is committed to providing superior customer service, including technical support and after-sales assistance, to ensure that clients receive the best possible solutions for their material handling needs. With a focus on quality and customer satisfaction, headpowder has become a trusted partner for businesses seeking reliable small stone powder conveying systems.