

Principle and Working Scene Characteristics of Coal Fly Ash Material Conveying Lines
Coal fly ash, a byproduct of coal combustion, is widely utilized in various industrial applications due to its unique properties. The efficient transportation of this material is crucial for optimizing production processes and ensuring environmental compliance. This article explores the fundamental principles of coal fly ash material conveying lines and highlights the key characteristics of their operational scenarios.
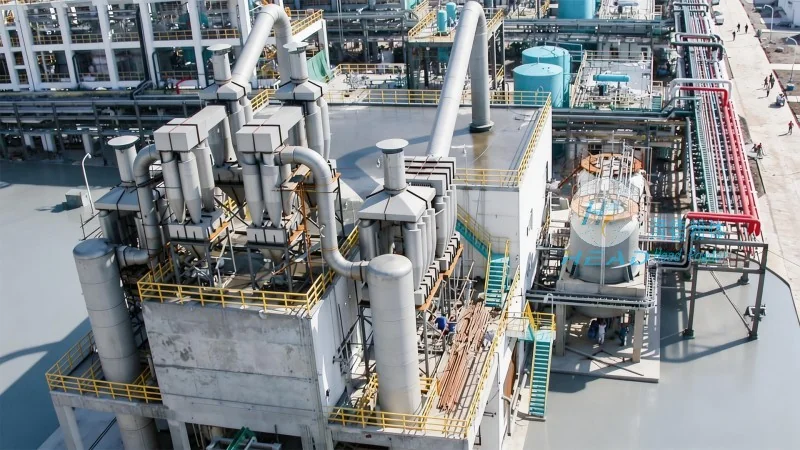
Overview of Coal Fly Ash Material Conveying Lines
Coal fly ash material conveying lines are specialized systems designed to transport coal fly ash from its source, such as power plant ash storage facilities, to processing or disposal sites. These systems typically consist of components like hoppers, feeders, conveyor belts or pipes, and control mechanisms. The primary goal is to achieve a reliable, continuous, and low-loss transfer of the fine, abrasive material while minimizing operational costs and environmental impact. The design of these systems must consider factors like material properties, flow rates, and the distance to be covered, ensuring that the chosen technology—whether pneumatic, mechanical, or a hybrid approach—optimizes performance and longevity.
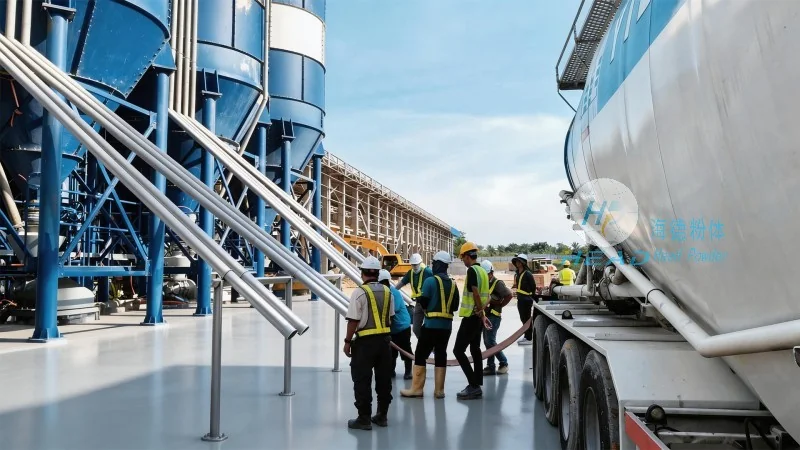
Working Principle of the Conveying System
The operation of a coal fly ash material conveying line is based on mechanical energy transfer. The process generally starts with the material being discharged from a storage hopper into a feeder. The feeder then regulates the flow rate, ensuring a consistent supply to the conveyor. For pneumatic conveying systems, compressed air is used to create a flow that transports the ash through pipelines. The air pressure and velocity are carefully controlled to prevent material degradation and ensure efficient transport. In mechanical systems, such as belt conveyors, the material is moved by the rotation of conveyor belts or rollers. The speed and tension of the belt are adjusted based on the material's characteristics and the required throughput. The control system monitors parameters like pressure, flow rate, and temperature to maintain optimal performance and prevent blockages or equipment damage. Additionally, sensors are often integrated to detect abnormalities, such as overloading or clogging, allowing for timely intervention and reducing downtime.
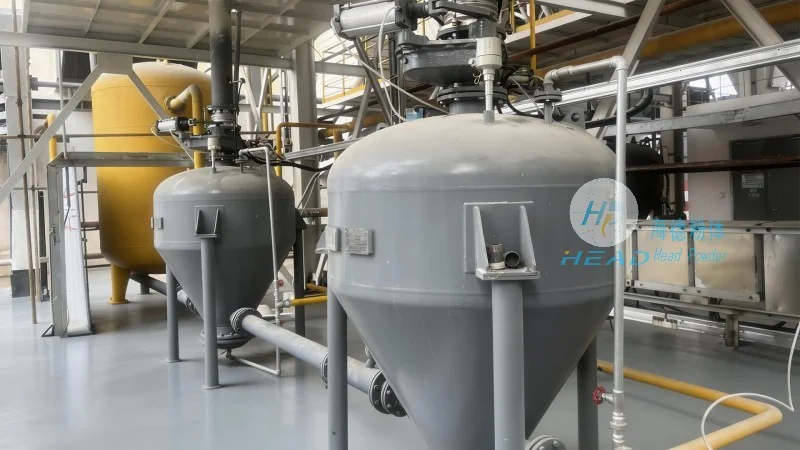
Key Working Scene Characteristics
The operational scenarios of coal fly ash material conveying lines vary significantly based on the application and industrial environment. For instance, in power plants, these systems are often integrated with existing infrastructure to handle large volumes of ash produced during electricity generation. The design must account for the material's fine particle size and potential for dust generation, requiring effective dust control measures like sealing and filtration. In construction material production facilities, the conveying lines may be used to supply ash as an ingredient in cement or concrete, necessitating precise control over moisture content and particle size distribution. This ensures that the final product meets quality standards and performance requirements. Furthermore, the systems are designed to operate in harsh conditions, including high temperatures and abrasive environments, which demands durable materials and robust construction to ensure long-term reliability. The ability to handle high volumes and maintain consistent flow rates is critical for maintaining production efficiency and reducing waste.
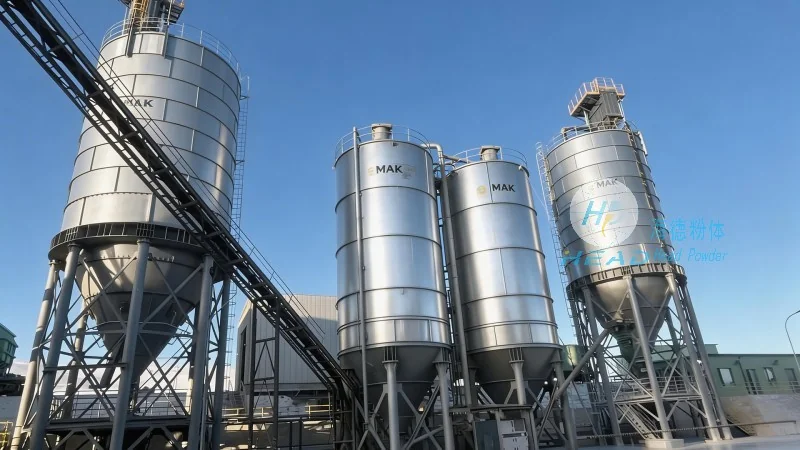
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of engineering solutions for material handling systems. With a focus on innovation and customer satisfaction, the company specializes in designing and manufacturing coal fly ash material conveying lines tailored to the specific needs of industrial clients. Headpowder's headquarters is located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality, cost-effective solutions for material transportation challenges. The company's commitment to quality and efficiency has made it a trusted partner in the industry for over [years of operation, if available, but as per info, just state as is]. Headpowder adheres to international standards and employs advanced technologies to ensure that its products meet the rigorous demands of modern industrial applications. The company's team of experienced engineers and technicians work closely with clients to understand their unique requirements and develop customized solutions that enhance operational performance and reduce costs.