

Operation Process and Working Principle of Sodium Bicarbonate Material Handling
Efficient material handling is a critical component in various industrial processes, particularly when dealing with bulk materials like sodium bicarbonate. The proper management of sodium bicarbonate from storage to processing or packaging stages ensures operational efficiency, safety, and product quality. This article explores the operation process and working principle of sodium bicarbonate material handling, highlighting key aspects that contribute to smooth and reliable material flow.
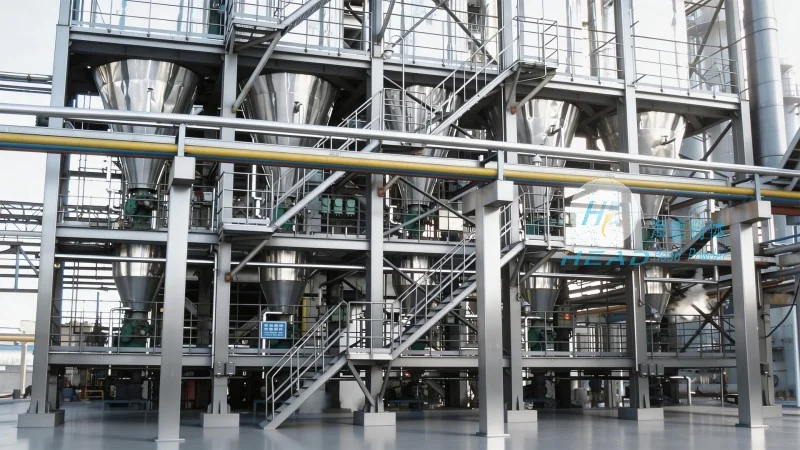
About HeadPowder: Your Trusted Partner in Material Handling Solutions
HeadPowder, a leading company in the field of material handling systems, specializes in providing tailored solutions for industries that rely on bulk material processing. With a strong presence in Shandong, China, HeadPowder Engineering Co., Ltd. has built a reputation for delivering high-quality equipment and services that meet the specific needs of clients. The company’s expertise lies in understanding the unique challenges of handling sodium bicarbonate and other similar materials, ensuring that the material handling processes are optimized for performance and reliability.
The Operation Process of Sodium Bicarbonate Material Handling
The operation process of sodium bicarbonate material handling typically involves several stages, each designed to ensure the safe and efficient movement of the material. The first stage is storage, where sodium bicarbonate is stored in bulk containers or silos. These storage units are designed to maintain the material’s quality and prevent contamination. Once the material is ready for transport, it is transferred from the storage silo to a conveyor system or other material handling equipment. The transfer process is carefully controlled to minimize dust generation and ensure a smooth flow of the material. The conveyor system then transports the sodium bicarbonate to the processing or packaging area, where it is further handled as per the production requirements.
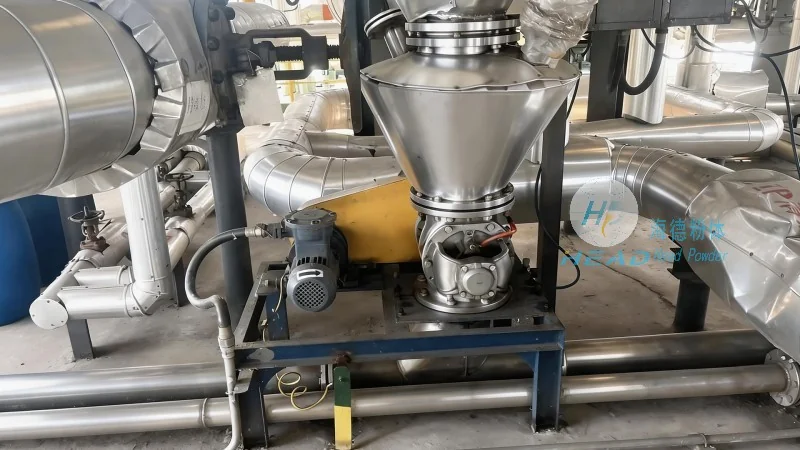
Working Principle of Sodium Bicarbonate Material Handling Systems
The working principle of sodium bicarbonate material handling systems is based on mechanical and pneumatic systems that work in tandem to move the material. Conveyors, such as belt conveyors or screw conveyors, are commonly used to transport the material horizontally or vertically. These systems utilize motor-driven mechanisms to move the material along the conveyor path. In addition to conveyors, pneumatic systems, including air slides or pneumatic conveyors, are employed to handle the material in a dust-free environment. The pneumatic systems use compressed air to create a flow of material, ensuring that the material is transported without the need for physical contact, which is particularly important for maintaining the purity of sodium bicarbonate.
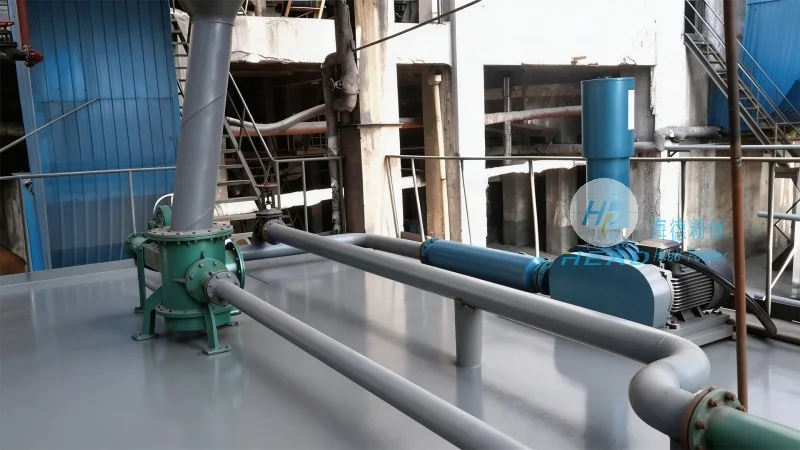
Key Considerations for Optimal Sodium Bicarbonate Material Handling
Several factors contribute to the optimal performance of sodium bicarbonate material handling systems. First, the design of the storage and handling equipment must consider the material’s properties, such as its bulk density and flow characteristics. Properly designed silos and hoppers help prevent material bridging or caking, which can disrupt the flow. Second, the material handling equipment must be equipped with appropriate safety features, such as dust collection systems and explosion-proof components, to ensure a safe working environment. Third, regular maintenance and monitoring of the equipment are essential to prevent breakdowns and ensure consistent performance. By addressing these considerations, industries can achieve efficient and reliable sodium bicarbonate material handling processes.
Conclusion: Enhancing Productivity with HeadPowder's Solutions
Efficient sodium bicarbonate material handling is crucial for maintaining productivity and product quality in industrial operations. HeadPowder Engineering Co., Ltd., based in Shandong, China, offers comprehensive material handling solutions that cater to the specific needs of clients. By understanding the operation process and working principle of sodium bicarbonate material handling, industries can optimize their processes and achieve better results. With a focus on quality and reliability, HeadPowder continues to be a trusted partner for businesses seeking to enhance their material handling capabilities.