

Operation Process and Working Principle of Purified Ash Pneumatic Conveying Equipment
Efficient material handling is a critical aspect of modern industrial operations, and the purified ash pneumatic conveying equipment offered by Shandong HeadPowder Engineering Co., Ltd. plays a pivotal role in achieving this goal. As a leading manufacturer in the field, HeadPowder specializes in providing high-performance solutions that ensure reliable and safe transport of ash and other particulate materials. This article delves into the operation process and working principle of these advanced systems, highlighting the key components, operational steps, and the technological advancements that make them indispensable in various industrial applications.
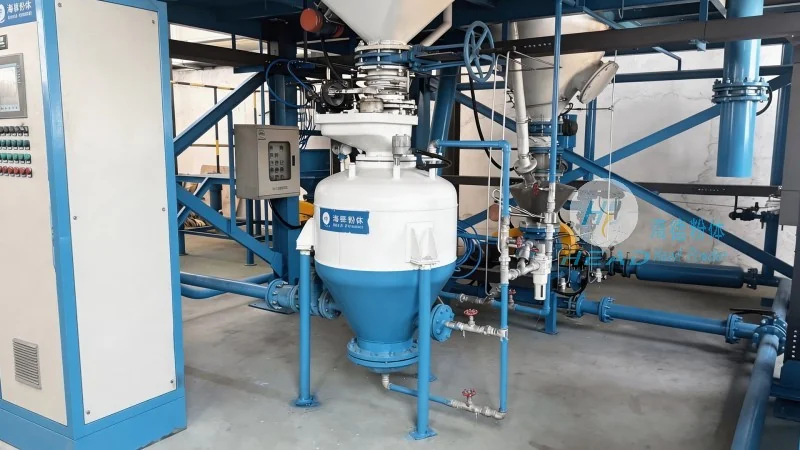
Introduction to Purified Ash Pneumatic Conveying Equipment
Purified ash pneumatic conveying equipment is designed to transport ash and other fine particulate materials from one location to another using a pressurized air system. The technology is widely used in power plants, waste management facilities, and other industrial settings where the efficient removal and transport of ash are essential for operational efficiency and environmental compliance. HeadPowder's equipment is engineered to meet stringent industry standards, ensuring durability, low maintenance, and optimal performance under various operating conditions.
Key Components of the System
The purified ash pneumatic conveying system consists of several critical components that work in tandem to facilitate the transport process. These include the ash hopper, which serves as the storage and feeding unit; the air compressor, responsible for generating the necessary pressure to move the material; the conveying pipeline, which transports the ash from the source to the destination; and the control system, which monitors and regulates the entire operation. Each component is meticulously designed to ensure seamless integration and optimal functionality.
Working Principle of the Equipment
The operation of the purified ash pneumatic conveying equipment is based on the principle of pneumatic transport, where the ash is suspended in a stream of air and carried through the pipeline. The process begins with the ash being fed from the hopper into the conveying line. The air compressor then generates a high-pressure air flow, which entrains the ash particles and propels them through the pipeline. The conveying line is typically equipped with bends, valves, and other accessories to direct the flow and control the speed of the material. The system is designed to maintain a consistent pressure and flow rate, ensuring that the ash is transported efficiently and without clogging or degradation.
Operation Process: Step-by-Step Guide
The operation of the purified ash pneumatic conveying equipment follows a systematic process that ensures smooth and continuous material transport. The steps involved are as follows:
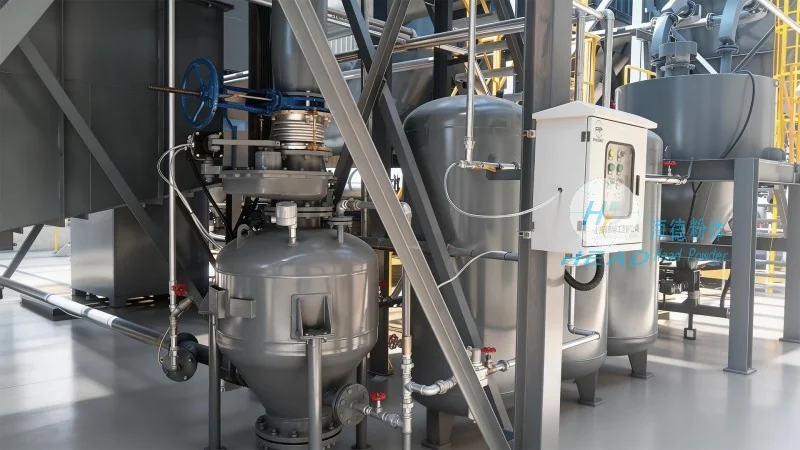
1. **Material Loading**: The ash is loaded into the ash hopper from the source, such as a boiler or storage silo. The hopper is equipped with a feeding mechanism that regulates the flow of ash into the conveying line.
2. **Air Compression**: The air compressor is activated, generating a high-pressure air stream. The pressure is maintained at a level sufficient to entrain the ash particles and move them through the pipeline.
3. **Conveying**: The ash is drawn into the conveying line by the high-pressure air, forming a slurry of ash and air. The mixture travels through the pipeline to the destination, such as a storage silo or treatment facility.
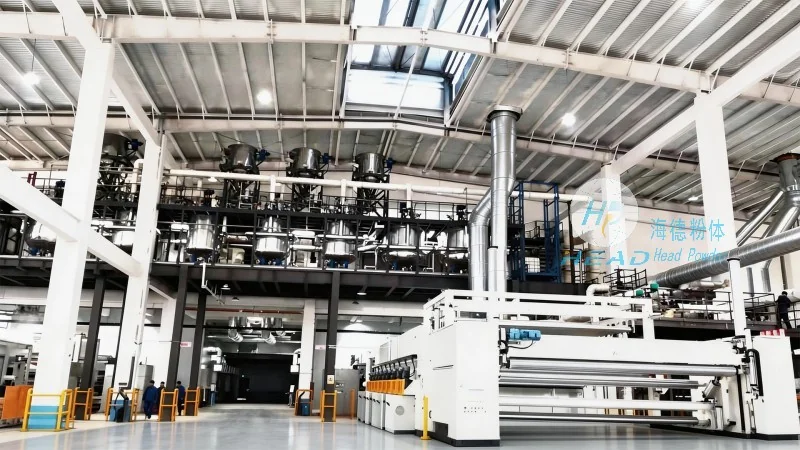
4. **Deposition**: At the destination, the ash is deposited into the receiving container. The air is then released, and the ash settles out, leaving the air to be recirculated or vented as needed.
Advantages of Purified Ash Pneumatic Conveying Equipment
HeadPowder's purified ash pneumatic conveying equipment offers several advantages that make it a preferred choice for industrial applications. These include:
- **High Efficiency**: The system ensures rapid and continuous transport of ash, reducing downtime and increasing overall operational efficiency.
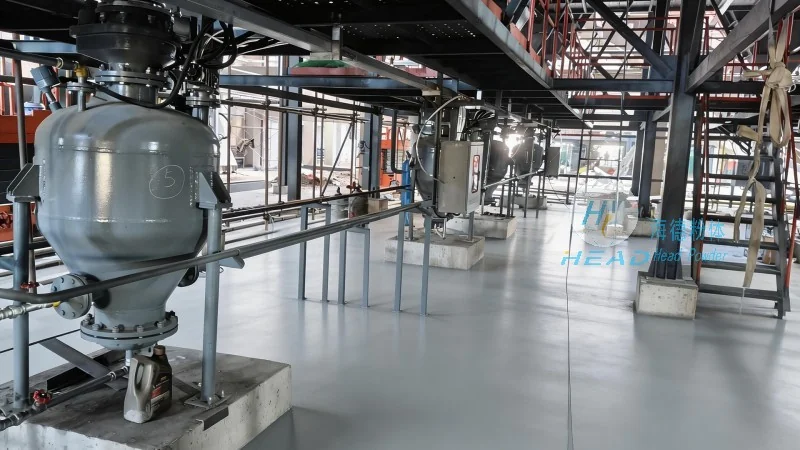
- **Low Maintenance**: The design of the equipment minimizes wear and tear, resulting in lower maintenance costs and longer service life.
- **Environmental Compliance**: The system is designed to minimize dust emissions and ensure compliance with environmental regulations, contributing to a cleaner and safer working environment.
- **Versatility**: The equipment can be customized to suit various material types and operational requirements, making it suitable for a wide range of industrial applications.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced purified ash pneumatic conveying equipment that combines cutting-edge technology with robust engineering. The operation process and working principle of these systems are designed to deliver reliable, efficient, and environmentally friendly material transport solutions. By understanding the key components, operational steps, and advantages of these systems, industrial facilities can enhance their material handling capabilities and achieve optimal performance in their operations.