

Operation Process and Working Principle of Sugar Powder Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. Among these, the sugar powder pneumatic conveying system stands out due to its efficiency and reliability in transporting granular and powdered materials like sugar. This article delves into the operation process and working principle of such systems, providing a comprehensive understanding for industry professionals and potential clients.
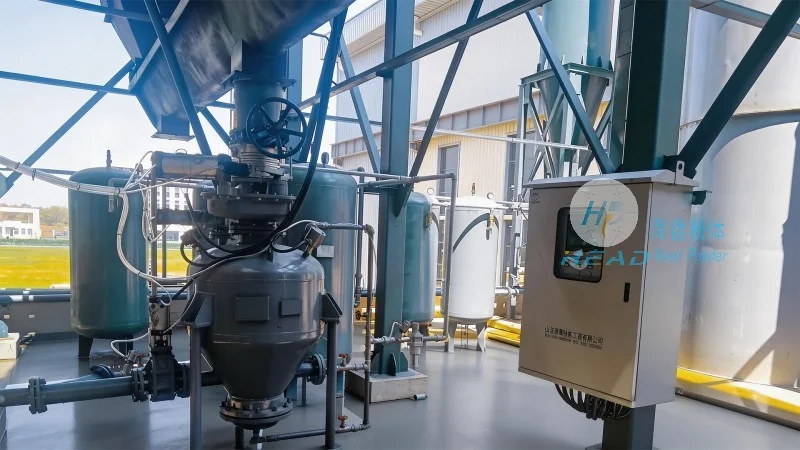
Understanding Pneumatic Conveying Basics
Pneumatic conveying is a method of transporting bulk materials through a pipeline using compressed air or other gases. Unlike traditional mechanical conveying systems, which rely on belts, screws, or buckets, pneumatic systems utilize the force of air to move materials. For sugar powder, this approach offers several advantages, including reduced product contamination, lower maintenance costs, and the ability to handle materials in a closed system, minimizing dust and environmental impact.
The Operation Process of Sugar Powder Pneumatic Conveying
The operation of a sugar powder pneumatic conveying system involves several key steps, each designed to ensure efficient and safe material transport. The process typically begins with the material being fed into a hopper or storage silo. From there, the material is drawn into the conveying line by a vacuum or pressure source, depending on the system configuration. The compressed air or gas then propels the sugar powder through the pipeline to the destination point, such as a processing plant or storage facility. The system may include components like rotary valves, filters, and cyclones to control the flow and ensure consistent performance.
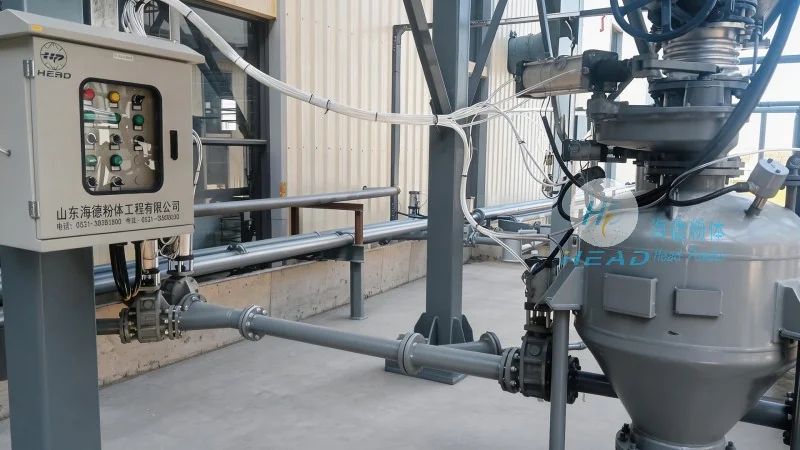
Working Principle of the System Components
To understand the working principle, it's essential to examine the key components of a sugar powder pneumatic conveying system. The primary components include the material feed hopper, the air supply unit (either a vacuum pump or a positive pressure blower), the conveying pipeline, and the discharge equipment. The feed hopper ensures a consistent supply of sugar powder, preventing blockages and maintaining a steady flow. The air supply unit generates the necessary pressure or vacuum to move the material. The pipeline, often made of stainless steel or other corrosion-resistant materials, is designed to handle the abrasive nature of sugar powder. The discharge equipment, such as a rotary valve or a dust collector, regulates the release of the material at the receiving end.
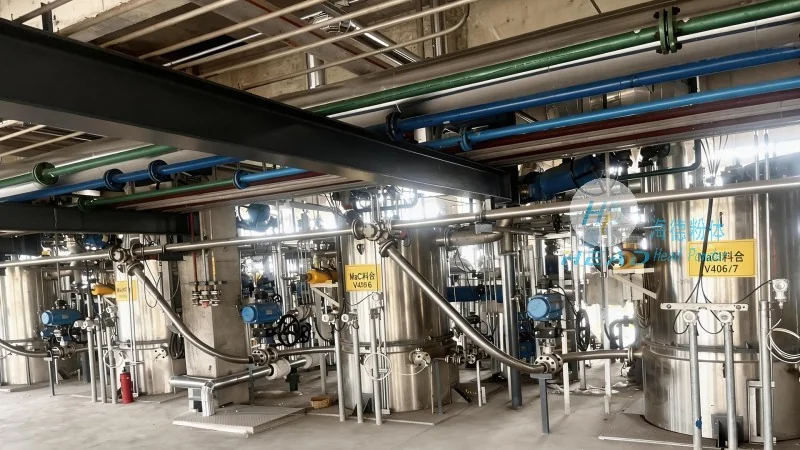
Advantages of Using Pneumatic Conveying for Sugar Powder
Implementing a pneumatic conveying system for sugar powder offers numerous benefits. Firstly, it provides a hygienic and dust-free environment, which is crucial for food-grade products like sugar. The closed system prevents contamination from external sources and reduces the risk of product degradation. Secondly, the system is highly efficient, with minimal energy consumption compared to mechanical conveying methods. Additionally, it allows for flexible layout designs, as the pipeline can be installed in various configurations to suit the plant's layout. The system also reduces labor costs by automating the material transport process, improving overall productivity.
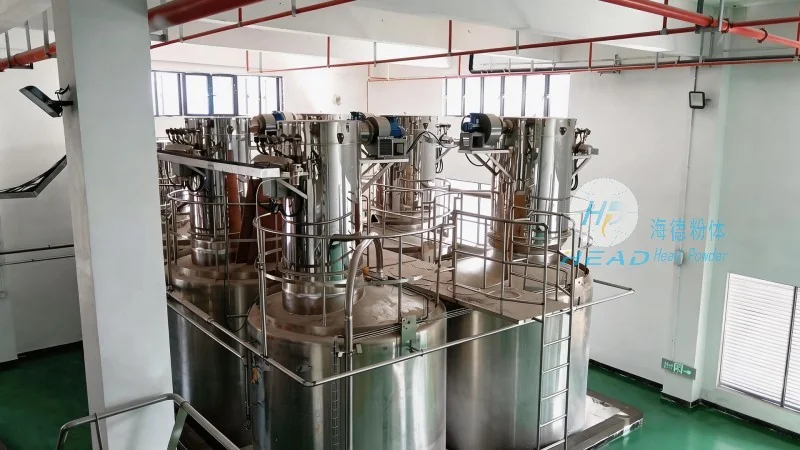
Applications and Industries
Sugar powder pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, these systems are essential for transporting sugar from storage to production lines, ensuring a smooth and consistent supply. In pharmaceutical applications, the hygienic design of the system meets stringent regulatory requirements, maintaining product purity. The versatility of the system also makes it suitable for handling other fine powders, such as flour, starch, and chemicals, making it a valuable asset in diverse industrial settings.
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in powder handling technology to provide customized pneumatic conveying solutions tailored to the specific needs of sugar processing facilities. By understanding the operation process and working principle of sugar powder pneumatic conveying, industries can enhance their operational efficiency, reduce costs, and ensure product quality. With a commitment to innovation and quality, HeadPowder continues to lead the way in developing advanced solutions for the bulk material transport industry.