

Introduction to Gray Bin Pneumatic Conveying: Structure and Principle Explanation
Gray bin pneumatic conveying systems are a critical technology in modern material handling, designed to efficiently transport bulk materials such as powders, granules, and other particulate substances. These systems utilize air as the primary conveying medium, enabling the seamless movement of materials from storage bins to processing or discharge points. The technology is based on pneumatic transport principles, which involve fluidizing material particles with pressurized air to create a consistent flow.
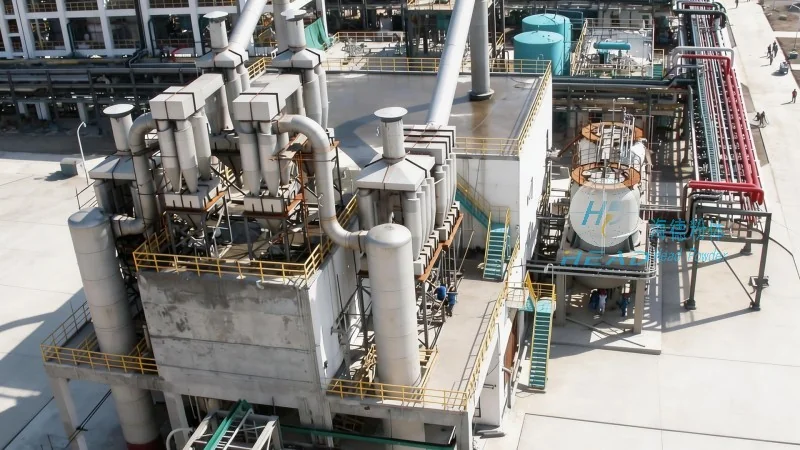
Core Components of Gray Bin Pneumatic Conveying Systems
The structure of a gray bin pneumatic conveying system typically consists of several key components that work together to ensure effective material transport. The primary elements include the gray bin or hopper, which serves as the material storage and feeding unit; an air compressor or blower that generates the necessary air pressure; a conveying line that transports the material from the bin to the discharge location; and a control system that regulates air flow and pressure to maintain optimal performance. Each component plays a vital role in the overall operation, ensuring that material is moved efficiently and without interruption.
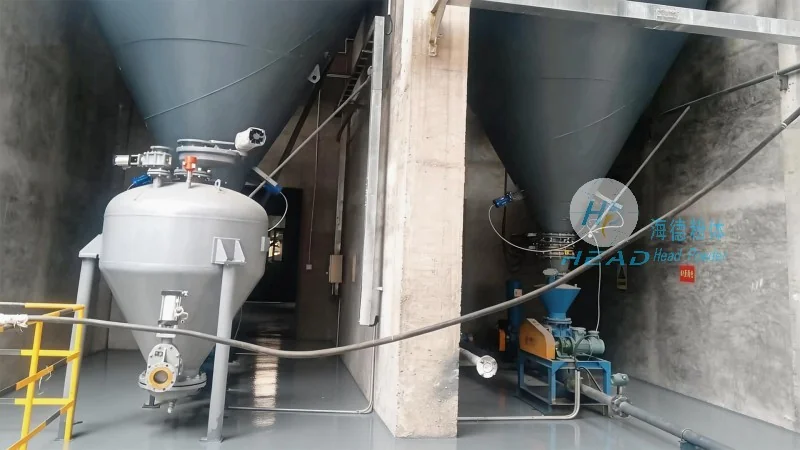
Working Principle and Operational Mechanism
The operation of a gray bin pneumatic conveying system relies on the principle of pneumatic transport, where pressurized air is used to lift and suspend material particles. When the air compressor activates, it draws ambient air and pressurizes it to a level sufficient to fluidize the material in the bin. The pressurized air then mixes with the material, creating a slurry-like flow that travels through the conveying line. The control system monitors and adjusts air pressure and flow rate to prevent blockages and ensure consistent material delivery. This process allows for continuous, low-maintenance material handling, making it ideal for industries requiring high throughput and reliability.
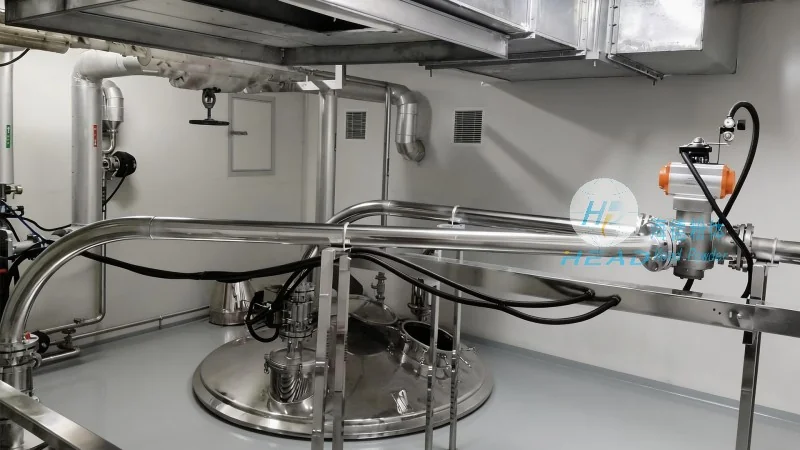
Advantages and Applications
Gray bin pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These include reduced maintenance costs due to the absence of moving parts like belts or screws, improved material handling efficiency with minimal downtime, and enhanced safety as there are no exposed mechanical components that could pose a risk. The system can handle a wide range of materials, from fine powders to larger granules, and is particularly suitable for industries such as chemical processing, food manufacturing, pharmaceuticals, and industrial minerals. The use of air as the conveying medium also ensures cleaner and more hygienic material transport, which is crucial in sectors where product purity and contamination control are paramount.
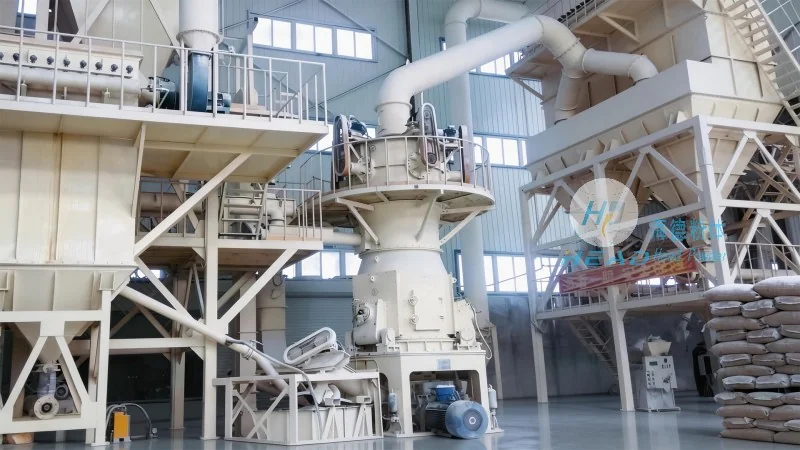
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling solutions, including gray bin pneumatic conveying systems. The company is headquartered in Shandong, China, and has built a strong reputation for its innovative designs, high-quality products, and reliable service. With years of experience in the industry, headpowder has developed a comprehensive range of pneumatic conveying systems tailored to meet the diverse needs of various industries. The company's commitment to technological advancement and customer satisfaction has made it a trusted partner for businesses seeking efficient and effective material handling solutions. Headpowder's expertise in pneumatic transport technology ensures that customers receive systems that are not only functional but also optimized for their specific operational requirements.